

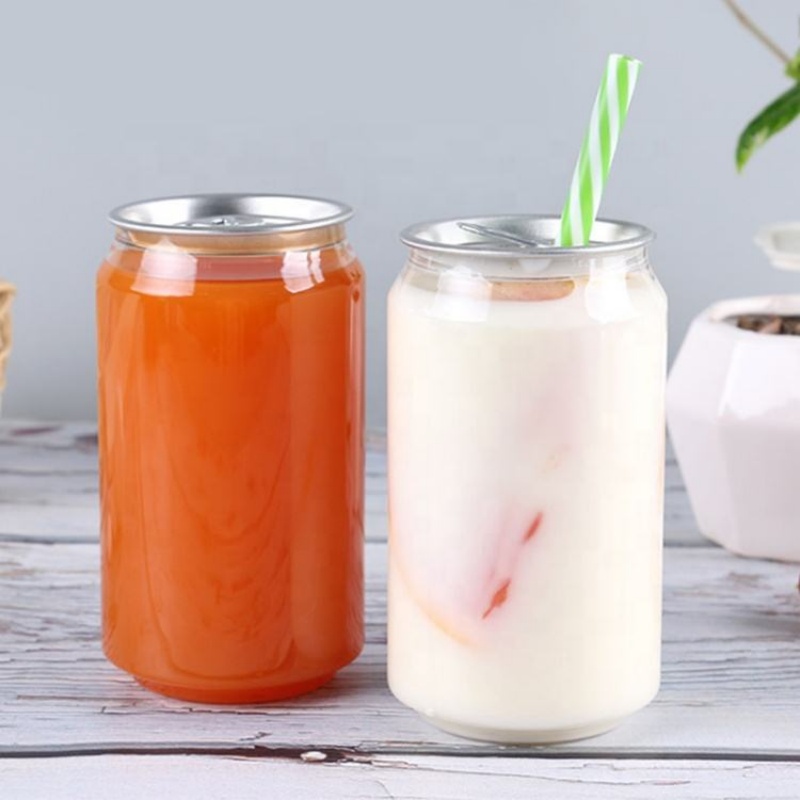
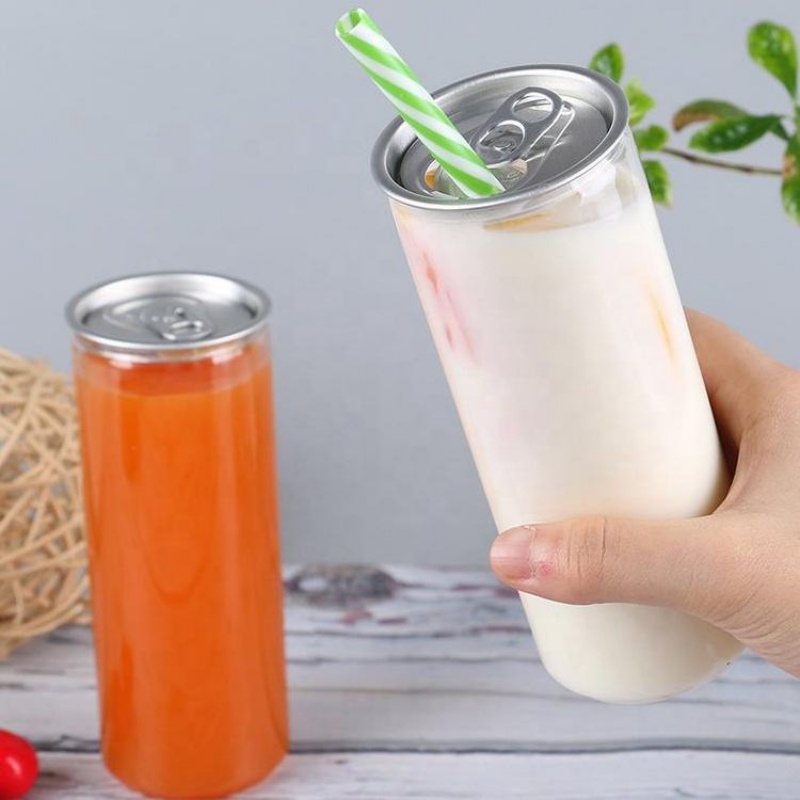
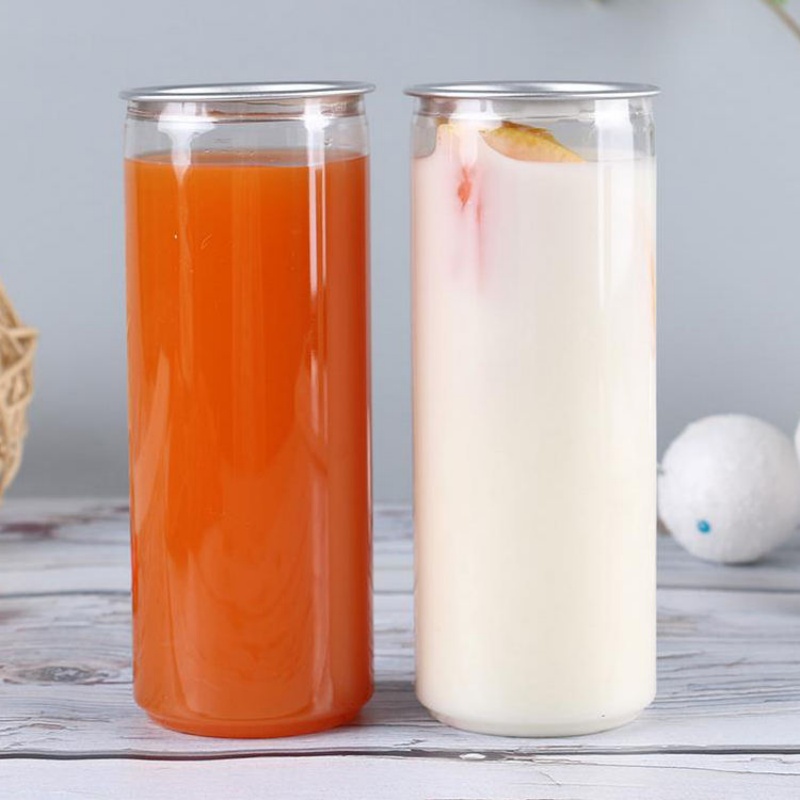
Wholesale PET beverage can with easy open end
Video
Product Introduction
The production process of a PET beverage can is a standardized, multi-step workflow that combines material preparation, molding, finishing, and quality control. Below is a detailed, step-by-step breakdown, including key technologies and quality checkpoints tailored for beverage packaging applications:
Production Stage |
Key Processes |
Technical Details & Quality Requirements |
Purpose |
1. Raw Material Preparation |
- Material selection & drying- Compound mixing (optional) |
- Virgin PET resin: Food-grade pellets that comply with FDA/EFSA standards (no BPA, phthalates). - rPET integration: Mix recycled PET pellets (30–100% content) with virgin PET for sustainability; ensure rPET is purified to food-grade standards. - Drying: PET pellets are dried at 120–160°C for 4–6 hours to reduce moisture content below 0.02% (prevents bubble formation during molding). - Additives (optional): Mix UV stabilizers (for light-sensitive drinks) or color masterbatches (for opaque cans) into pellets. |
Eliminate moisture-induced defects; ensure material safety and consistency for food contact. |
2. Preform Injection Molding |
- Injection molding of PET preforms- Cooling & trimming |
- Process: Dried PET pellets are melted at 260–280°C in an injection molding machine, then injected into preform molds (the preform is a small, test-tube-shaped semi-finished product with a threaded neck). - Molds: Precision molds with cavity numbers matching production capacity (e.g., 96-cavity molds for high-volume production). - Cooling: Preforms are cooled rapidly (10–20 seconds) with chilled water to maintain shape stability.- Trimming: Remove excess flash from preform necks to ensure uniform thread size. |
Produce consistent preforms—the foundation of PET can shape and strength. |
3. Stretch Blow Molding (Core Step) |
- Preform heating- Stretch & blow molding- Final cooling |
- Heating: Preforms are heated to 90–110°C (glass transition temperature of PET) in an infrared oven; the neck area is shielded from heat to preserve thread integrity. - Stretch: A stretch rod pushes the heated preform vertically to 2–3 times its original length (enhances molecular orientation for strength). - Blow molding: High-pressure air (20–40 bar) is injected to expand the stretched preform against the can mold cavity, forming the final can shape (cylindrical, tapered, or custom). - Cooling: The mold is cooled with water to solidify the PET can in 2–5 seconds. |
Form the final PET can body with precise dimensions, pressure resistance, and transparency. |
4. Secondary Processing & Finishing |
- Trimming & deburring- Surface treatment (optional)- Printing & labeling- Lid assembly |
- Trimming: Cut the top edge of the can to a uniform height for lid installation. - Surface treatment: Corona treatment (increases surface tension) to ensure ink adhesion for printing; or apply a matte/frosted coating for premium brands. - Printing: Use food-safe, UV-curable inks for high-definition graphics, logos, and compliance information (e.g., recyclable labels, multilingual text). - Lid assembly: Attach easy-open ends (EOE) or resealable screw lids—ensure airtight sealing to meet beverage shelf-life requirements. |
Enhance aesthetics, branding, and functionality; ensure the can is ready for filling. |
5. Quality Control & Testing |
- Dimensional inspection- Pressure resistance test- Leakage test- Food safety testing |
- Dimensional check: Verify can height, diameter, and wall thickness (tolerance ±0.1mm) with automated gauges. - Pressure test: Subject cans to 3–4 bar internal pressure (for carbonated drinks) to ensure no deformation or rupture. - Leak test: Use vacuum or helium leak detectors to confirm airtightness (critical for beverage freshness). - Food safety test: Test for residual monomers, heavy metals, or microplastic migration (comply with FDA/EFSA limits). |
Eliminate defective products; ensure compliance with food safety and packaging standards. |
6. Packaging & Warehousing |
- Grouping & stacking- Palletizing & storage |
- Grouping: Cans are packed into plastic bags or cartons to prevent scratches during transport. - Palletizing: Use automated palletizers to stack cartons; wrap pallets with stretch film for stability. - Storage: Store in a dry, cool warehouse (temperature 15–25°C, humidity <60%) to avoid PET degradation. |
Prepare finished cans for shipment to beverage filling plants; maintain product quality before use. |
Send Inquiry
We are committed to providing you with the best quality service and look forward to communicating with you to solve problems together and bring you a better experience.