Leave Your Message
Transforming the minibar experience with innovative, sustainable packaging solutions
The global luxury hotel industry is experiencing a paradigm shift in guest amenities, with minibar offerings evolving from simple convenience items to curated experiences that reflect brand values and guest expectations. Transparent PET cans have emerged as a game-changing packaging solution in this transformation, offering luxury hotels an unprecedented combination of visual appeal, sustainability, and functional excellence. The global hotel minibar market, valued at approximately $2.8 billion in 2023, is projected to reach $4.2 billion by 2030, with premium packaging solutions like transparent PET cans driving significant growth in the luxury segment.
Luxury hotels worldwide are increasingly recognizing that minibar presentation directly impacts guest satisfaction scores and revenue per available room (RevPAR). Transparent PET cans address multiple hospitality challenges simultaneously: they provide crystal-clear product visibility that eliminates guest uncertainty, offer lightweight yet durable protection for premium beverages, and communicate a commitment to environmental responsibility that resonates with modern luxury travelers. Leading hotel chains including Four Seasons, Ritz-Carlton, and Mandarin Oriental have begun integrating transparent PET packaging into their minibar programs, reporting improved guest feedback and reduced product waste.
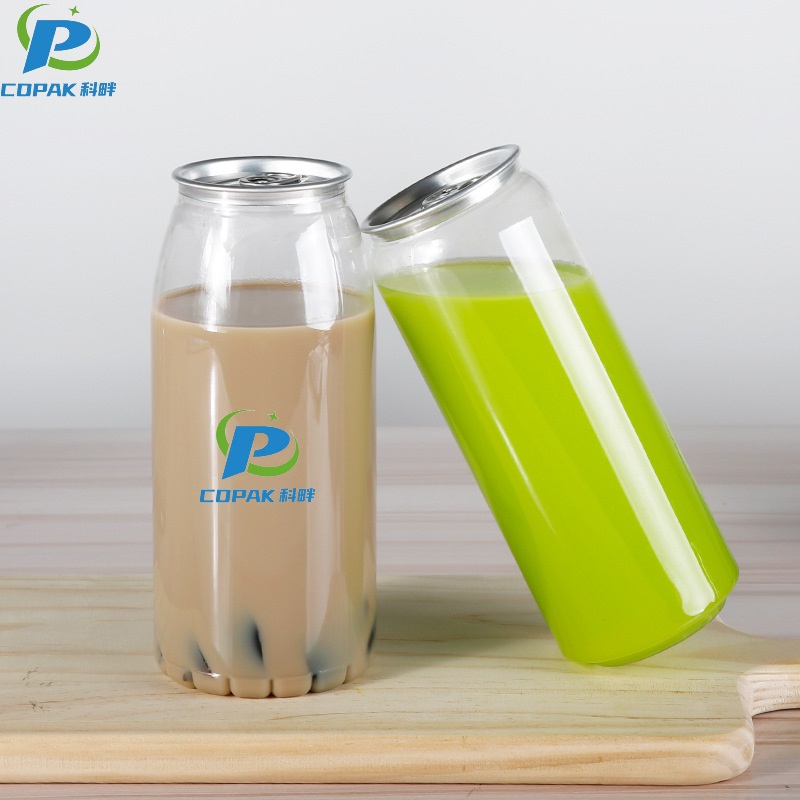
Unlike traditional aluminum cans or glass bottles, transparent PET cans offer luxury hotels a unique value proposition. The crystal-clear visibility allows guests to instantly identify beverage contents without opening the package, reducing unnecessary consumption and waste. The lightweight nature of PET significantly reduces transportation costs and carbon footprint—a critical consideration for international hotel chains managing complex supply chains. Additionally, PET's shatter-resistant properties eliminate safety concerns associated with glass in minibar environments, while maintaining the premium aesthetic luxury guests expect.
Several converging trends are accelerating the adoption of transparent PET cans in luxury hotel minibars. The sustainability imperative has become paramount, with 78% of luxury travelers indicating they prefer hotels with demonstrated environmental commitments. PET's recyclability rate—currently at 29% globally but reaching over 50% in markets with advanced collection infrastructure—positions it favorably against single-use alternatives. Furthermore, PET packaging generates 67% less CO2 emissions during production compared to glass and 45% less than aluminum, according to lifecycle assessment studies.
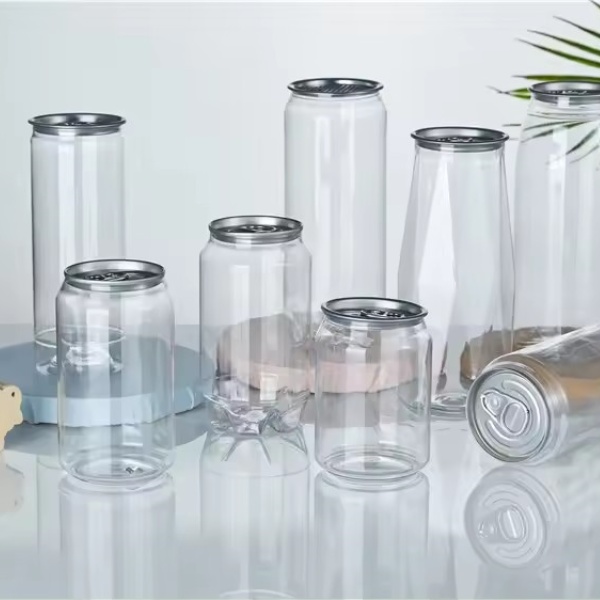
The premiumization trend in hospitality is another significant driver. Luxury hotels are moving beyond standard beverage offerings to curate unique, Instagram-worthy minibar experiences. Transparent PET cans enable this by serving as a canvas for sophisticated branding, custom shapes, and innovative designs that photograph beautifully. Hotels are partnering with boutique beverage brands to create exclusive minibar collections packaged in custom transparent PET cans, transforming the minibar from a utilitarian convenience into a memorable brand touchpoint.
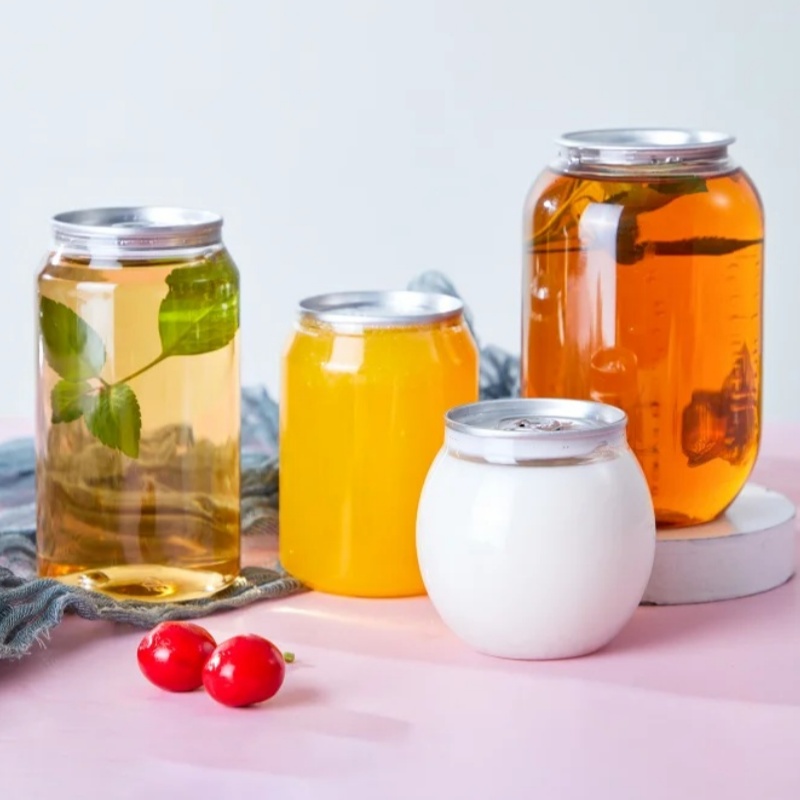
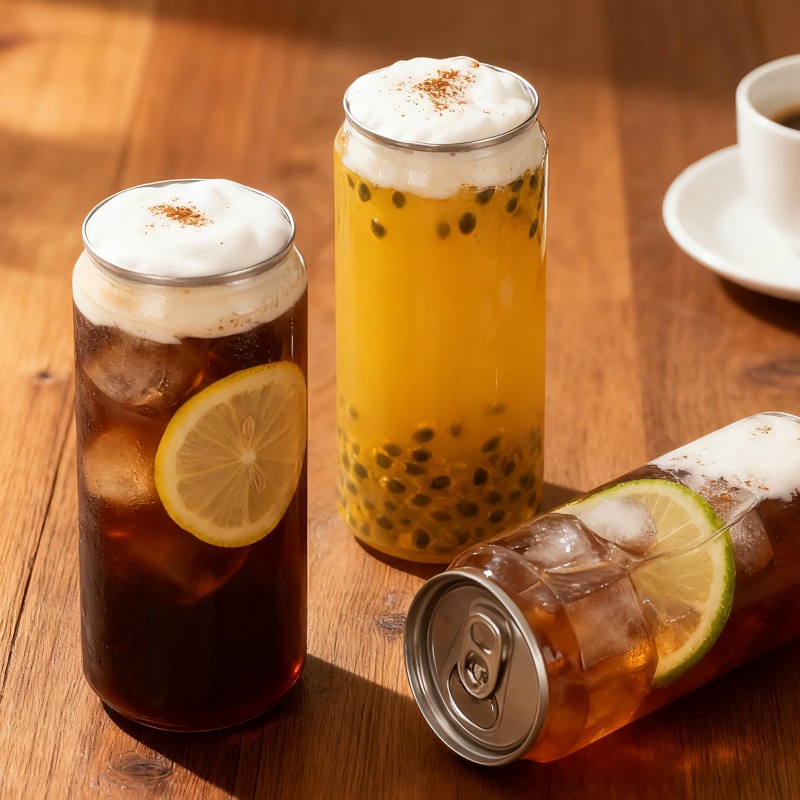
Implementing transparent PET cans in luxury hotel minibars requires strategic consideration across multiple operational dimensions. Beverage selection is paramount—transparent packaging works exceptionally well for premium sparkling waters, craft sodas, cold brew coffees, botanical beverages, and artisanal juices where visual appeal enhances perceived value. Leading luxury hotels are curating minibar selections that leverage transparency as a feature, showcasing beverages with visible ingredients like fruit pieces, herbs, or layered colors that create visual interest.
Temperature management represents a critical technical consideration. Luxury hotels typically maintain minibar temperatures between 38-42°F (3-6°C), and transparent PET cans must maintain structural integrity and condensation management within this range. Advanced PET formulations with enhanced barrier properties prevent moisture accumulation that could compromise label adhesion or visual clarity. Some luxury properties are implementing specialized minibar units with LED lighting systems specifically designed to showcase transparent PET packaging, creating an illuminated display that enhances the guest experience.
For luxury hotel chains implementing transparent PET cans across multiple properties, supply chain optimization becomes crucial. Centralized procurement of standardized PET can formats enables significant volume discounts while maintaining brand consistency. However, regional customization remains important—hotels in different markets may require varied beverage selections reflecting local preferences while maintaining the unified transparent PET packaging format. Leading hospitality groups are establishing strategic partnerships with PET can manufacturers like COPAK to ensure consistent quality, reliable supply, and access to innovation in packaging technology.
Inventory management for transparent PET cans offers distinct advantages over traditional packaging. The lightweight nature reduces storage space requirements by approximately 40% compared to glass bottles of equivalent volume. The durability of PET eliminates breakage losses during handling and restocking—a common issue with glass that can account for 3-5% of minibar inventory costs. Additionally, transparent PET's resistance to UV degradation when properly formulated ensures product quality maintenance even in minibars with ambient light exposure.
While transparent PET cans may carry a slightly higher unit cost than standard aluminum cans, the total cost of ownership for luxury hotels proves favorable. Reduced breakage, lower shipping costs, decreased storage requirements, and improved guest satisfaction scores combine to deliver ROI within 12-18 months for most luxury properties. Furthermore, the sustainability messaging enabled by PET packaging contributes to enhanced brand reputation—an intangible but valuable asset in the competitive luxury hospitality market.
The transparent PET can market for luxury hospitality continues to evolve rapidly with several emerging innovations. Smart packaging integration represents a frontier development, with pilot programs testing NFC-enabled PET cans that provide guests with detailed product information, sustainability credentials, and even pairing suggestions via smartphone interaction. Some luxury hotels are experimenting with QR codes printed on transparent PET labels that link to immersive brand stories or virtual tours of beverage production facilities.
Material science advances are pushing the boundaries of PET performance. Next-generation bio-based PET formulations derived from plant sources rather than petroleum are entering commercial production, offering luxury hotels the opportunity to further enhance their sustainability credentials. Enhanced barrier coatings are extending shelf life for sensitive beverages, while new manufacturing techniques enable increasingly complex custom shapes that transform PET cans into distinctive design objects worthy of luxury positioning.
The integration of transparent PET cans with broader hotel technology ecosystems represents another development frontier. Some luxury properties are implementing minibar sensors that automatically track transparent PET can consumption and integrate with property management systems for seamless billing. This technology also enables sophisticated inventory analytics, helping hotels optimize minibar assortments based on actual consumption patterns rather than assumptions.
The adoption of transparent PET cans in luxury hotel minibars exhibits distinct regional patterns. North American luxury hotels lead in implementation, driven by strong sustainability awareness and established PET recycling infrastructure. European luxury properties are rapidly following, particularly in markets with stringent single-use plastic regulations that favor recyclable PET over alternative materials. The Asia-Pacific region represents the highest growth potential, with luxury hotel development booming in markets like China, India, and Southeast Asia where modern properties are incorporating transparent PET from inception rather than retrofitting existing programs.
Middle Eastern luxury hotels present unique opportunities, with ultra-luxury properties in Dubai, Abu Dhabi, and Qatar seeking distinctive minibar presentations that align with their premium positioning. These properties often feature expanded minibar programs with extensive beverage selections, making the visual merchandising advantages of transparent PET particularly valuable. Latin American luxury hotels are emerging adopters, particularly in resort destinations where sustainability messaging resonates strongly with international guests.
Transparent PET cans for luxury hotel applications must meet rigorous food safety and quality standards across multiple jurisdictions. FDA compliance in the United States, EU Regulation No. 10/2011 in Europe, and GB standards in China represent baseline requirements. Luxury hotels typically require additional certifications including ISO 9001 quality management verification, HACCP compliance for food contact materials, and third-party testing documentation for BPA-free composition. Leading PET can manufacturers maintain comprehensive certification portfolios enabling seamless deployment across international hotel portfolios.
Quality assurance extends beyond regulatory compliance to encompass aesthetic and functional performance standards. Luxury hotels establish detailed specifications covering wall thickness uniformity (critical for consistent visual clarity), dimensional tolerances (ensuring proper fit in minibar configurations), seal integrity (preventing leakage and maintaining carbonation), and label adhesion performance (maintaining premium appearance throughout product lifecycle). Reputable PET can suppliers implement multi-stage quality control processes with statistical sampling to ensure consistent delivery of specification-compliant products.

Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
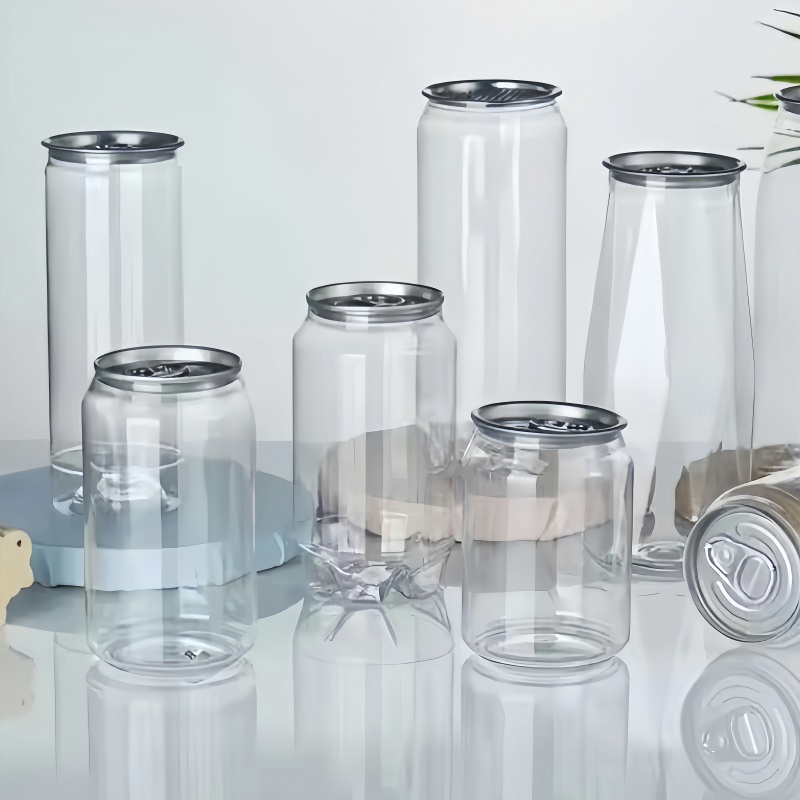
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
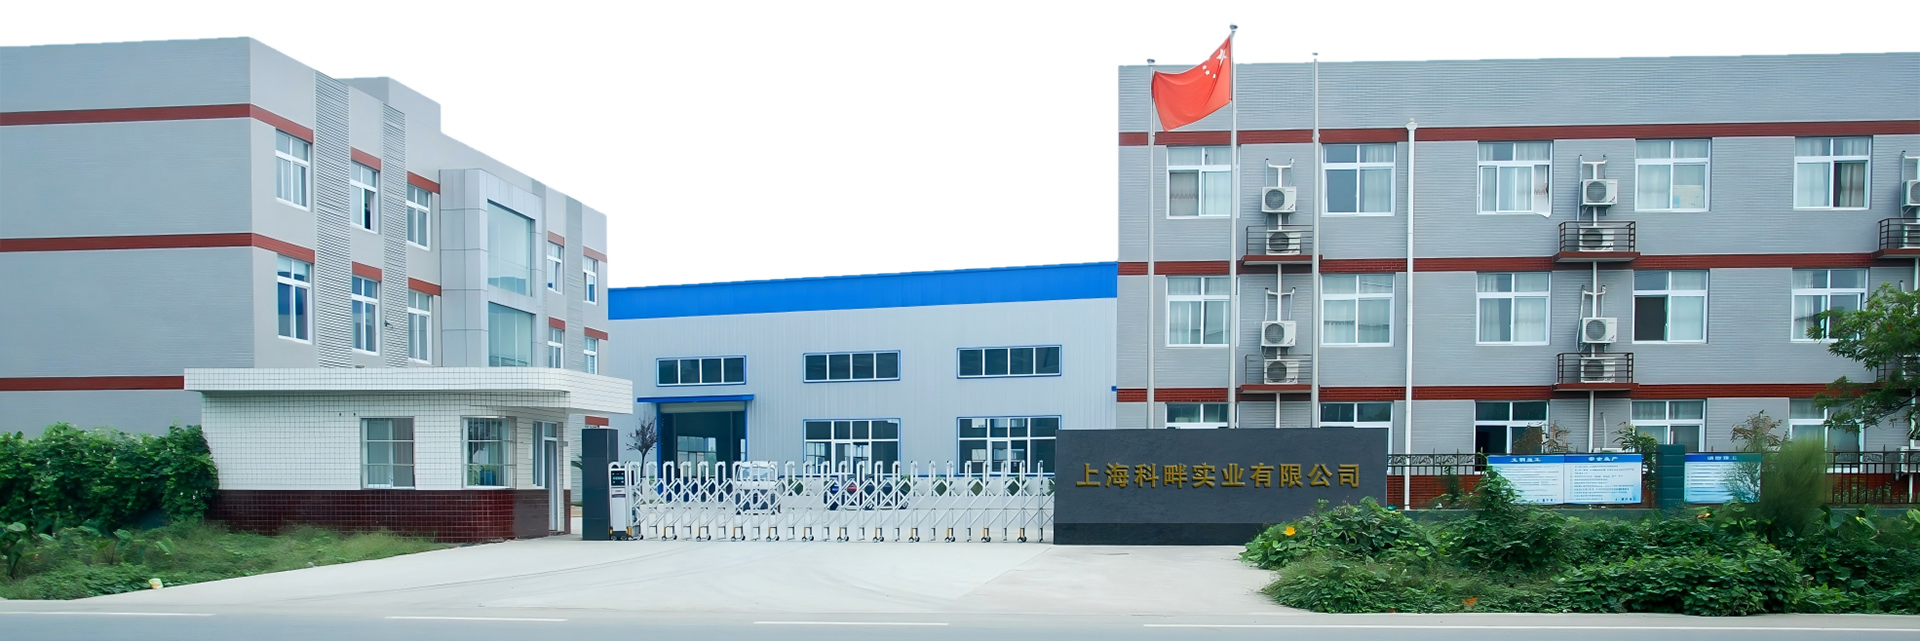
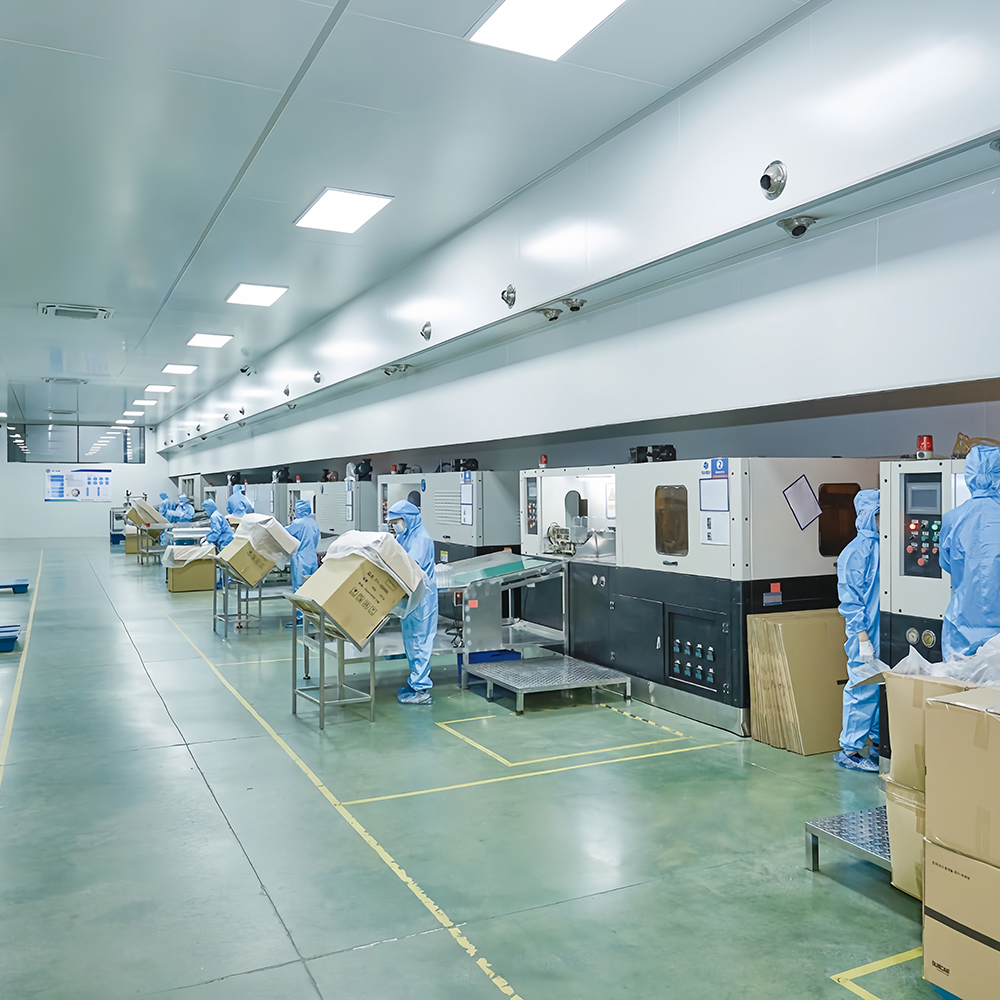
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
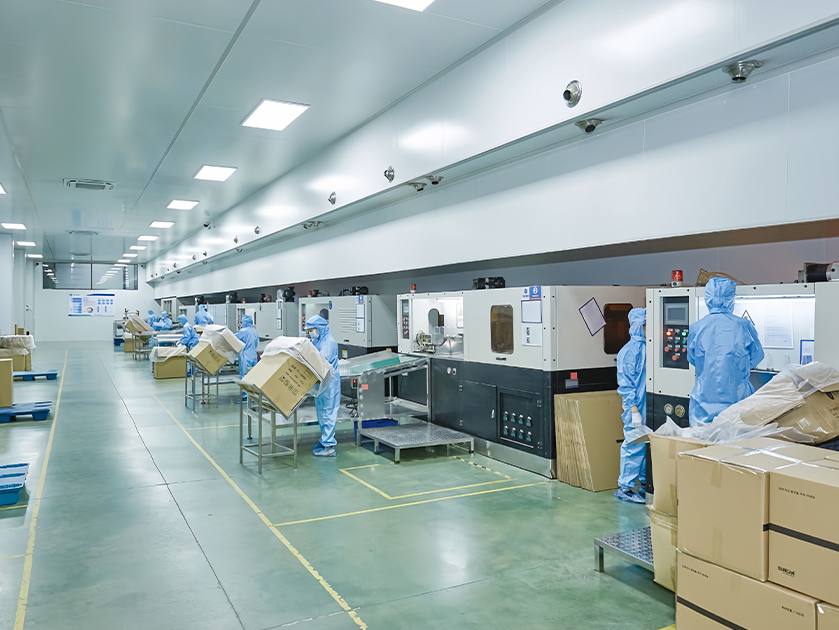
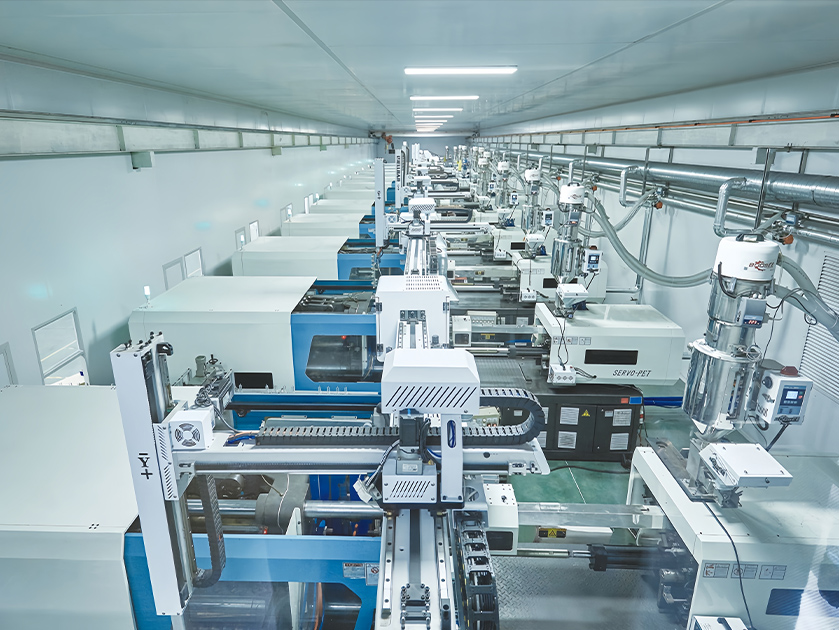
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
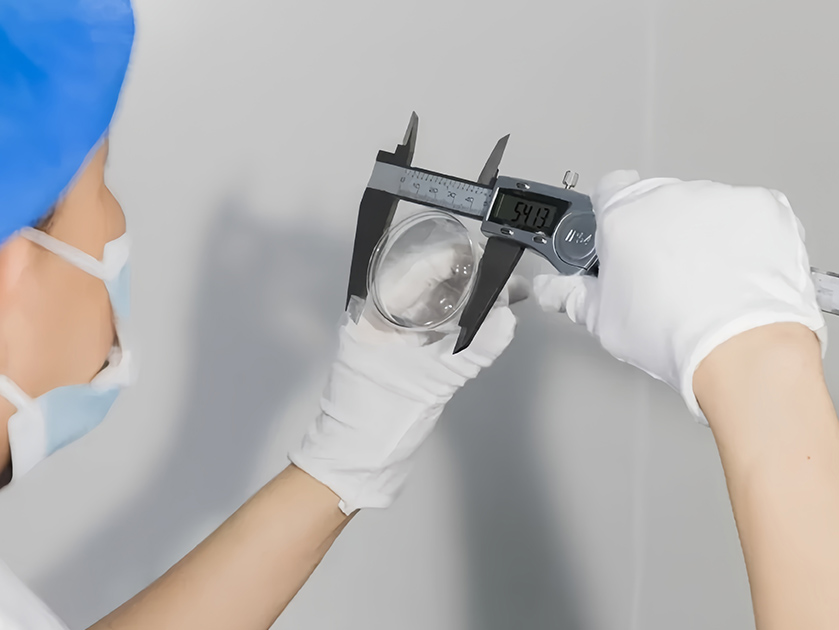
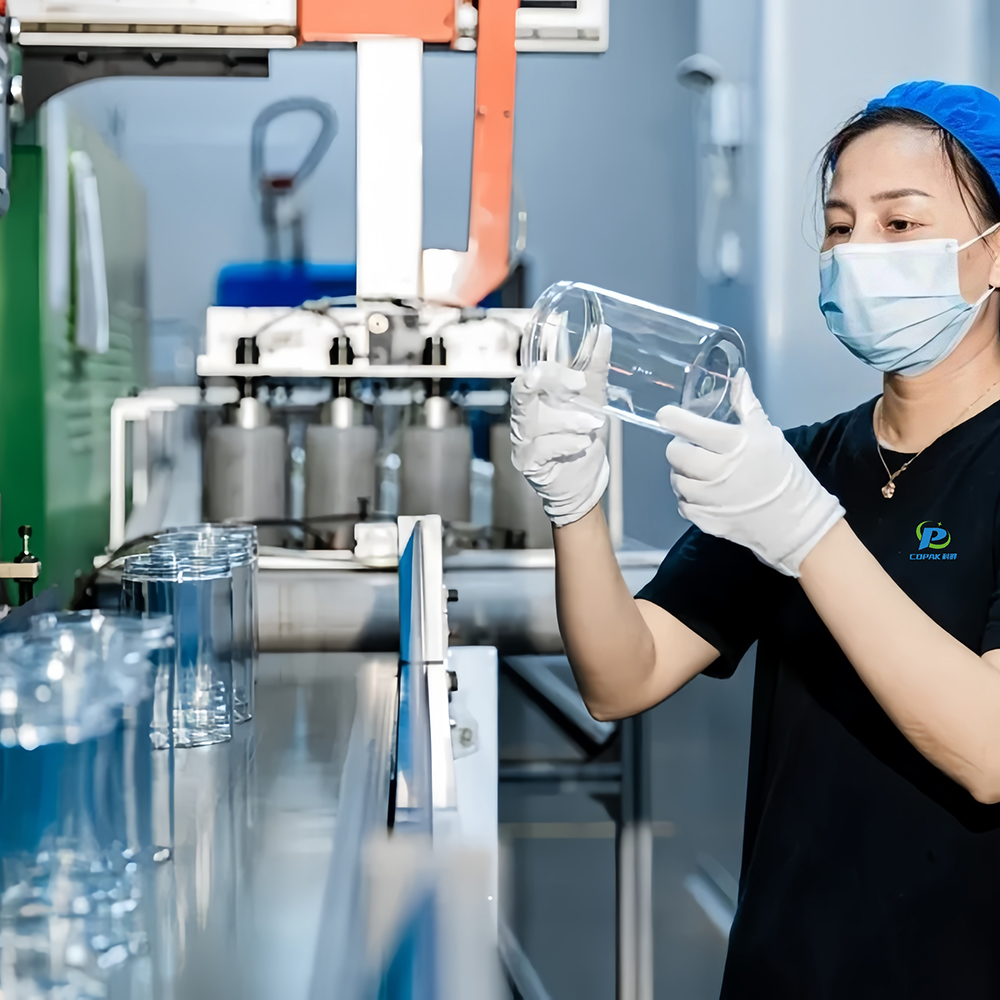
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsAdhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.