Leave Your Message
University campuses represent a rapidly growing market for sustainable beverage packaging solutions. With millions of students worldwide seeking convenient, eco-friendly refreshment options, RPET pop-top cans have emerged as the ideal solution for campus vending machines. The global campus vending machine market is projected to reach $8.5 billion by 2027, with sustainability-focused products leading the growth trajectory.
Modern universities are increasingly committed to environmental responsibility, with over 70% of campuses implementing comprehensive recycling programs. RPET (Recycled Polyethylene Terephthalate) pop-top cans align perfectly with these initiatives, offering 100% recyclable packaging that reduces carbon footprint by up to 60% compared to traditional aluminum cans. This makes them an essential component of campus sustainability strategies.
The demand for RPET packaging in educational institutions has grown by 45% annually over the past three years. This surge is driven by Generation Z's environmental consciousness, institutional sustainability commitments, and the superior functionality of pop-top cans in vending machine applications. Industry analysts predict this trend will accelerate as more campuses transition to eco-friendly vending solutions.
Advanced manufacturing technologies have enabled RPET pop-top cans to match the durability and shelf-life of traditional packaging while maintaining superior environmental credentials. Smart vending integration, QR code tracking, and IoT-enabled inventory management systems are transforming how beverages are distributed on campus, with RPET cans at the forefront of this technological revolution.
RPET pop-top cans excel in diverse university environments, providing versatile solutions for every campus need
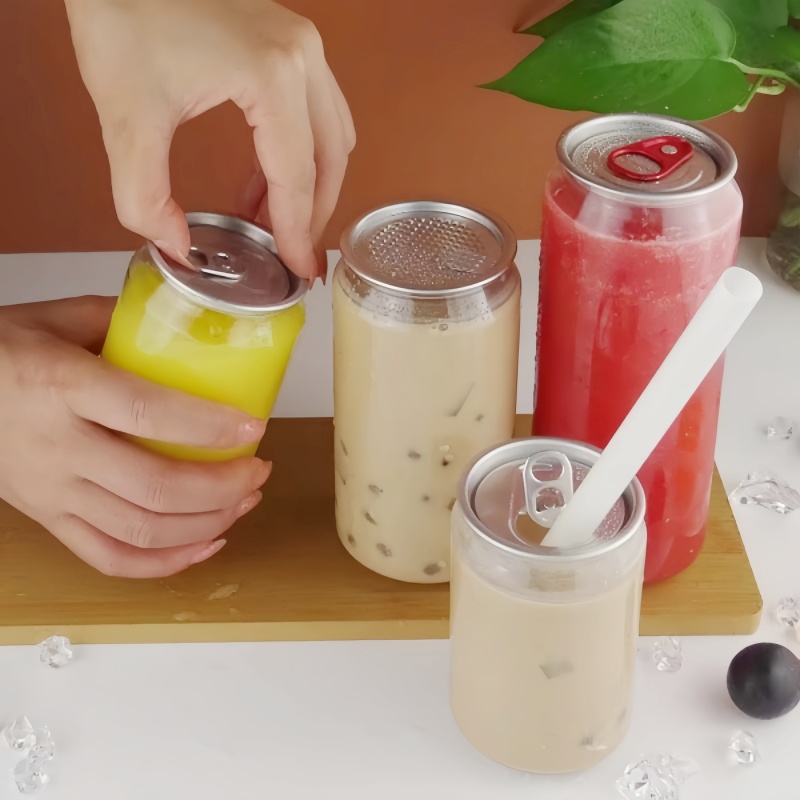
Silent pop-top opening mechanism ensures minimal disruption in quiet study environments. The transparent RPET material allows students to identify beverages quickly, while the resealable design prevents spills near valuable books and electronics.
Lightweight yet durable RPET construction withstands the demands of athletic facilities. The ergonomic pop-top design allows easy one-handed operation, perfect for post-workout refreshment. Shatter-resistant properties ensure safety in high-traffic gym environments.
Strategic placement in classroom buildings provides convenient access between lectures. The stackable design maximizes vending machine capacity, while the clear material showcases beverage quality and brand appeal, driving purchase decisions.
24/7 availability in dormitory vending machines meets student lifestyle needs. The resealable pop-top feature allows consumption over multiple occasions, reducing waste and providing better value. Compact design fits standard mini-fridges perfectly.
High-volume vending locations benefit from rapid dispensing capabilities and visual appeal. Custom printing options enable campus branding and event sponsorship opportunities, creating additional revenue streams while promoting sustainability initiatives.
Weather-resistant RPET material performs reliably in outdoor vending installations. UV-stable construction prevents degradation in sunlight, while the secure pop-top seal maintains beverage freshness in varying temperature conditions throughout the academic year.
Lower transportation costs due to lightweight design. Reduced breakage rates minimize inventory loss. Competitive pricing compared to aluminum alternatives makes RPET cans financially attractive for campus vending operations.
Food-grade RPET material meets all FDA and EU safety standards. Tamper-evident pop-top seals ensure product integrity. Non-metallic construction eliminates sharp edges and corrosion concerns in vending environments.
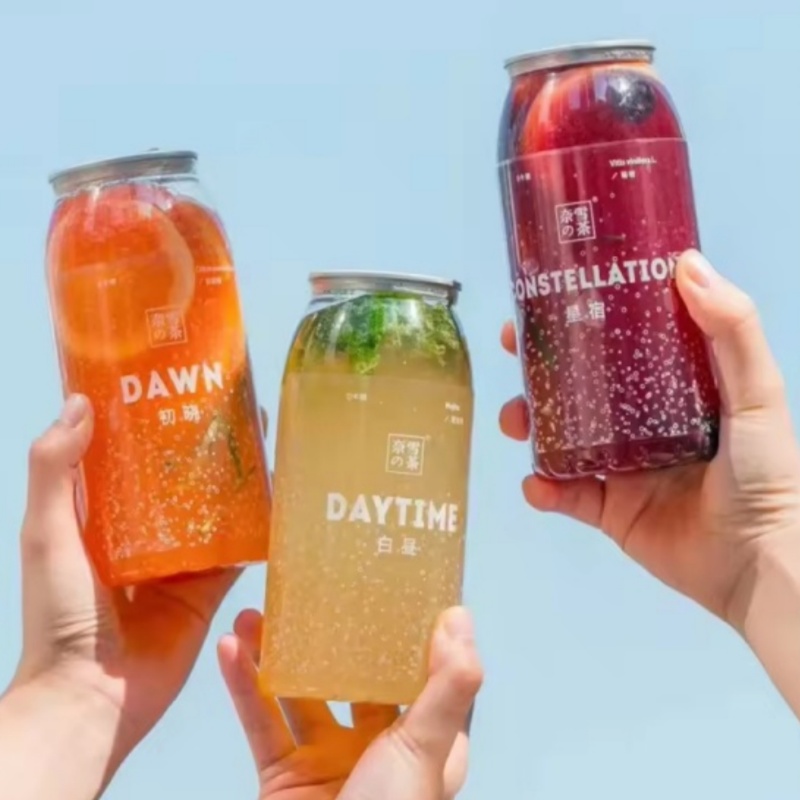
360-degree printing surface maximizes brand visibility. Clear material allows creative label designs and beverage showcase. Custom shapes and sizes available to differentiate products in competitive campus markets.
Compatible with standard vending machine configurations. Consistent dimensions ensure reliable dispensing mechanisms. Stackable design optimizes storage and reduces restocking time for campus facilities management.
75% lower carbon footprint compared to aluminum production. Fully recyclable in existing campus recycling programs. Supports university sustainability goals and green campus certifications like LEED and STARS.
Survey data shows 82% of students prefer eco-friendly packaging. Resealable feature aligns with on-the-go campus lifestyle. Transparent design appeals to health-conscious consumers who want to see product quality.
The next generation of campus vending will feature IoT-enabled machines that communicate with RPET cans embedded with NFC chips. This technology will enable real-time inventory tracking, personalized recommendations based on student preferences, and automated reordering systems. Universities will gain valuable data insights into consumption patterns, allowing for optimized product placement and reduced waste through predictive analytics.
Progressive campuses are implementing closed-loop recycling systems where used RPET cans are collected, processed on-site, and converted back into new packaging. This campus-to-campus circular economy reduces transportation emissions and creates educational opportunities for students in sustainability programs. Pilot programs have demonstrated 90% collection rates and significant cost savings over traditional waste management.
Research into bio-based PET alternatives is advancing rapidly, with several universities partnering with manufacturers to develop next-generation materials. These innovations combine recycled content with plant-based components, further reducing environmental impact. Commercial availability is expected within 2-3 years, positioning early adopters as sustainability leaders.
QR codes and augmented reality features on RPET cans are creating new engagement opportunities. Students can scan codes to access nutritional information, participate in campus sustainability challenges, or earn rewards points. This digital integration transforms beverage packaging into an interactive platform that enhances campus life and promotes environmental awareness.

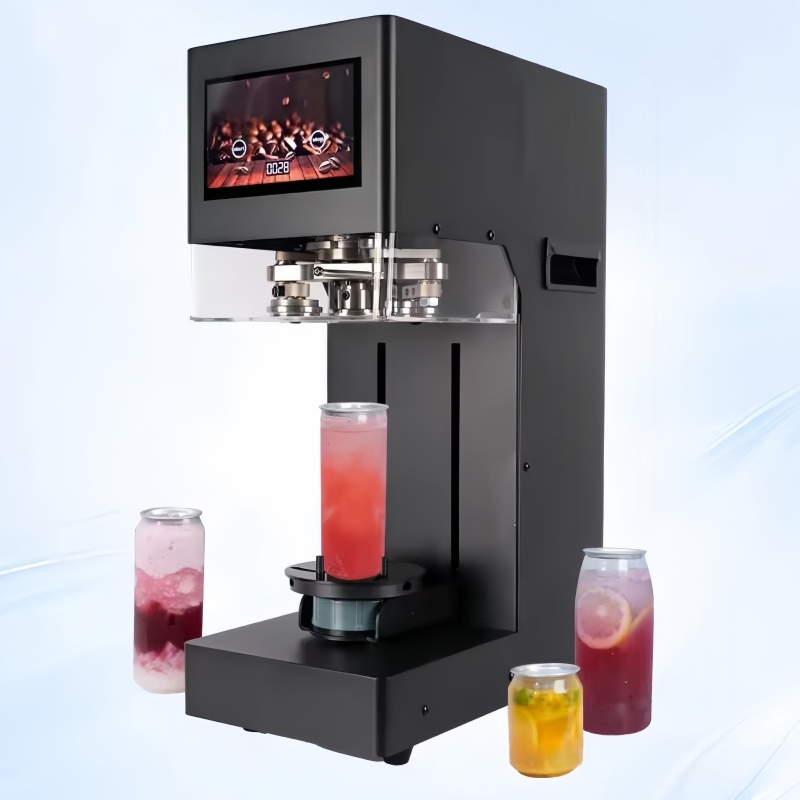
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
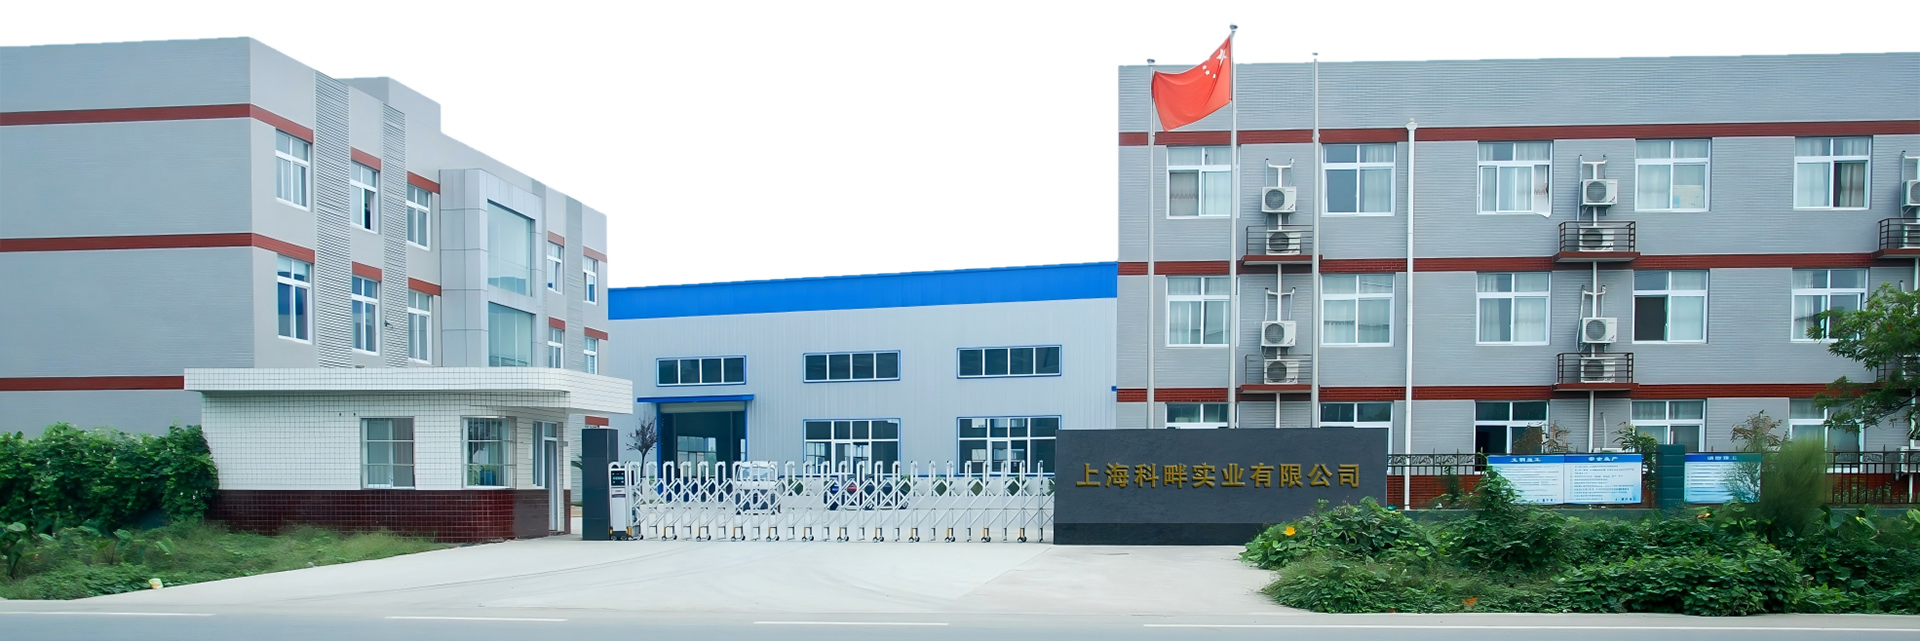
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
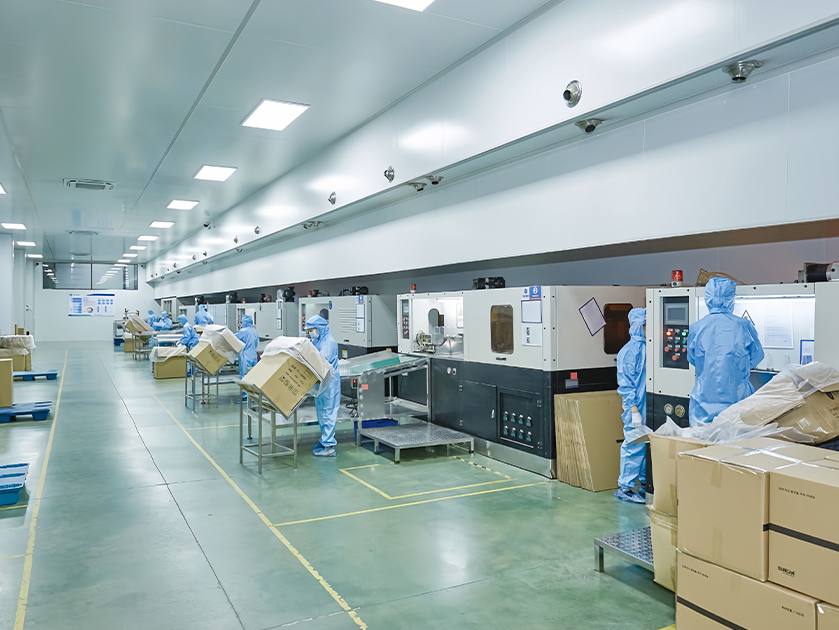
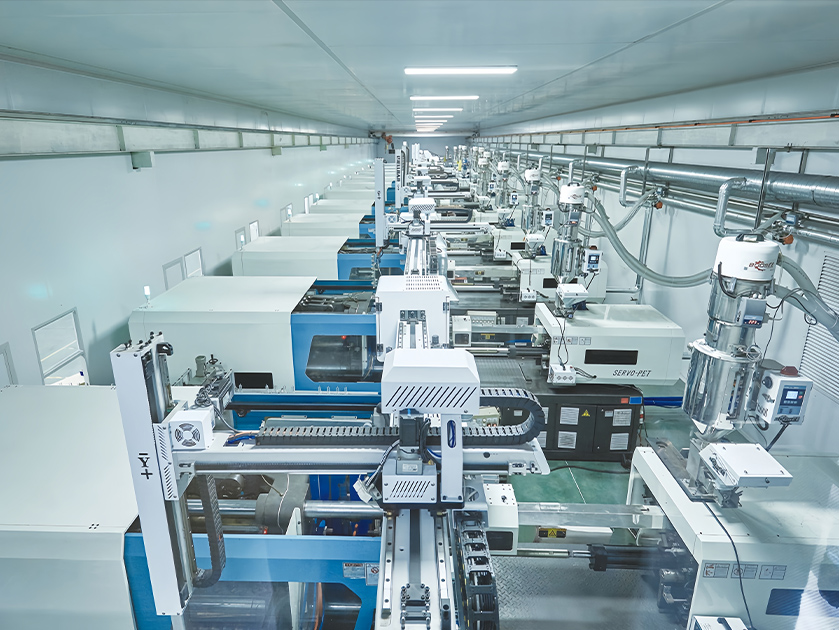
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
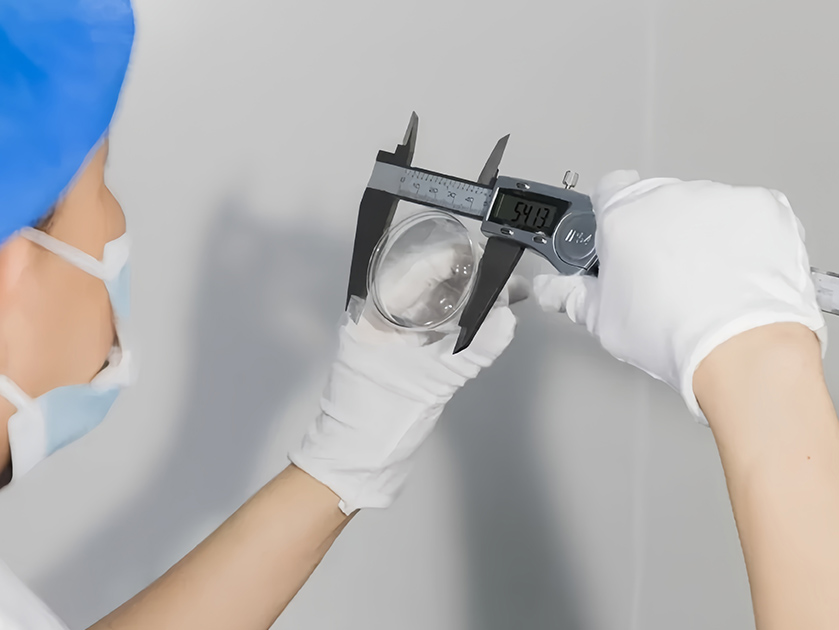
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsAdhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
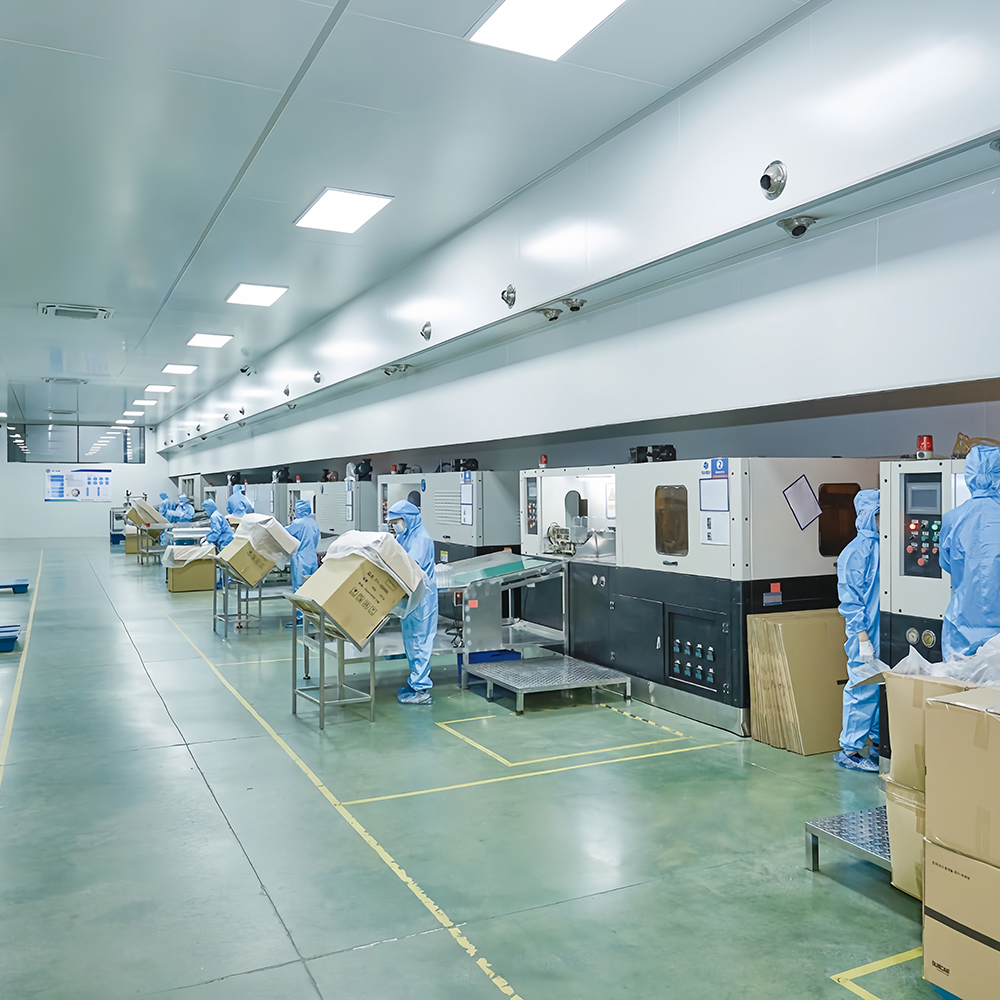
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
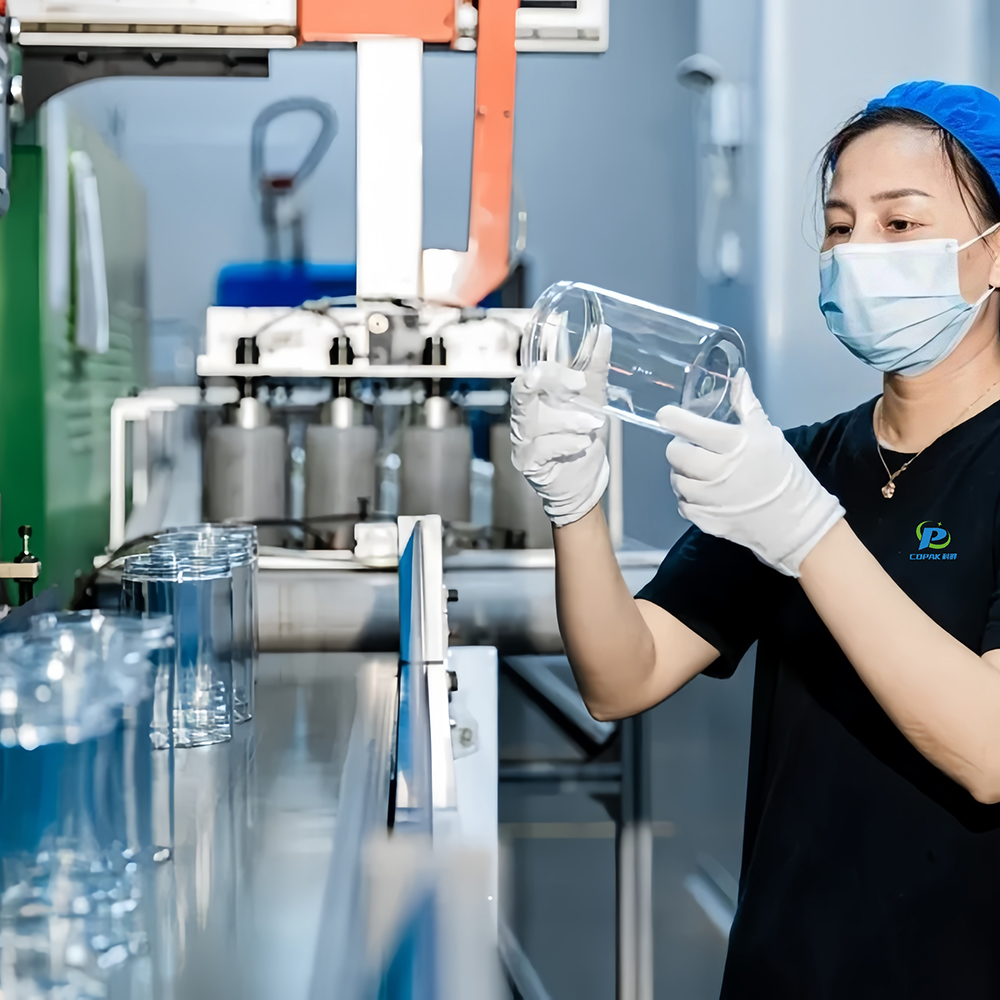
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
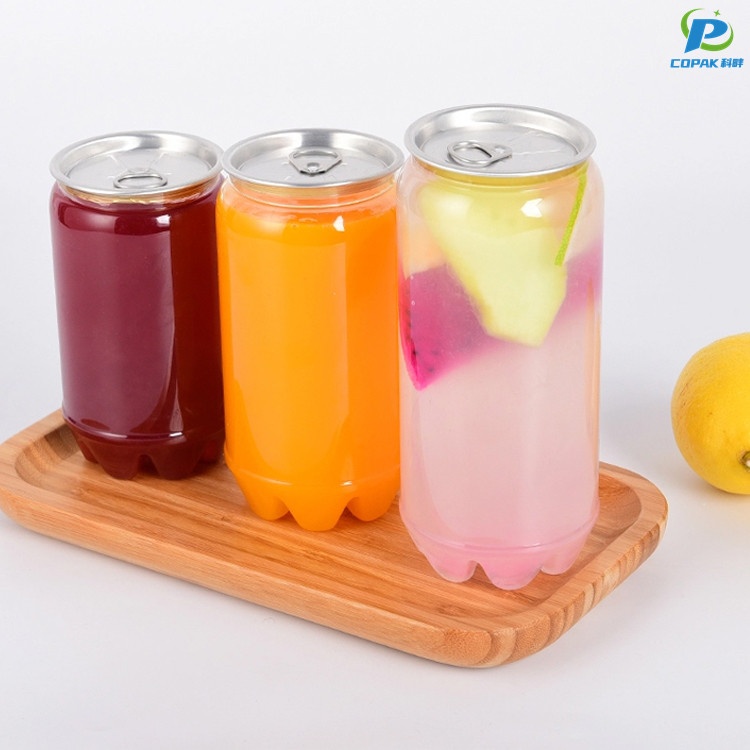
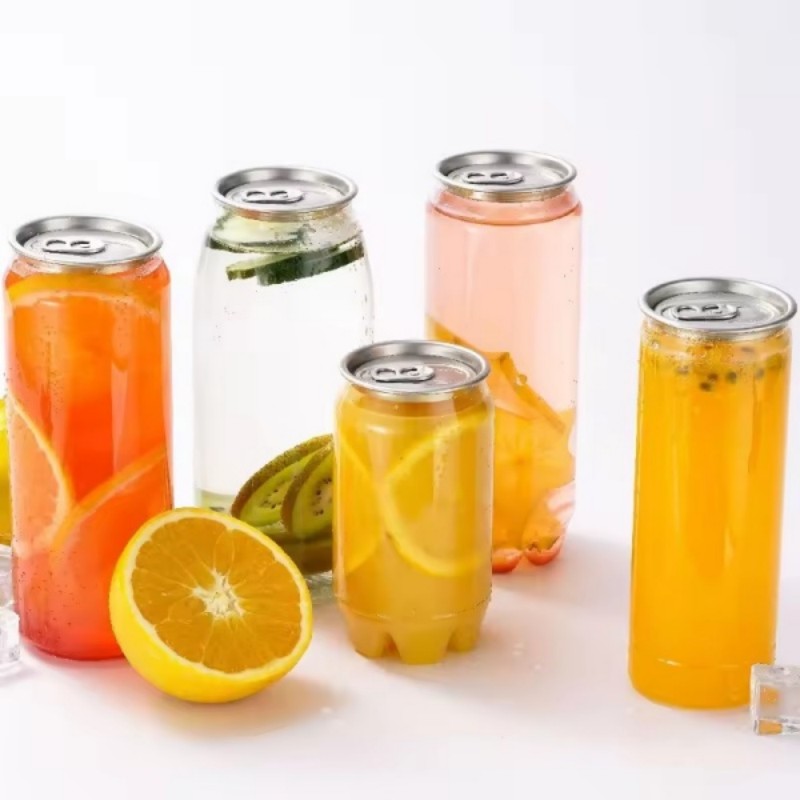
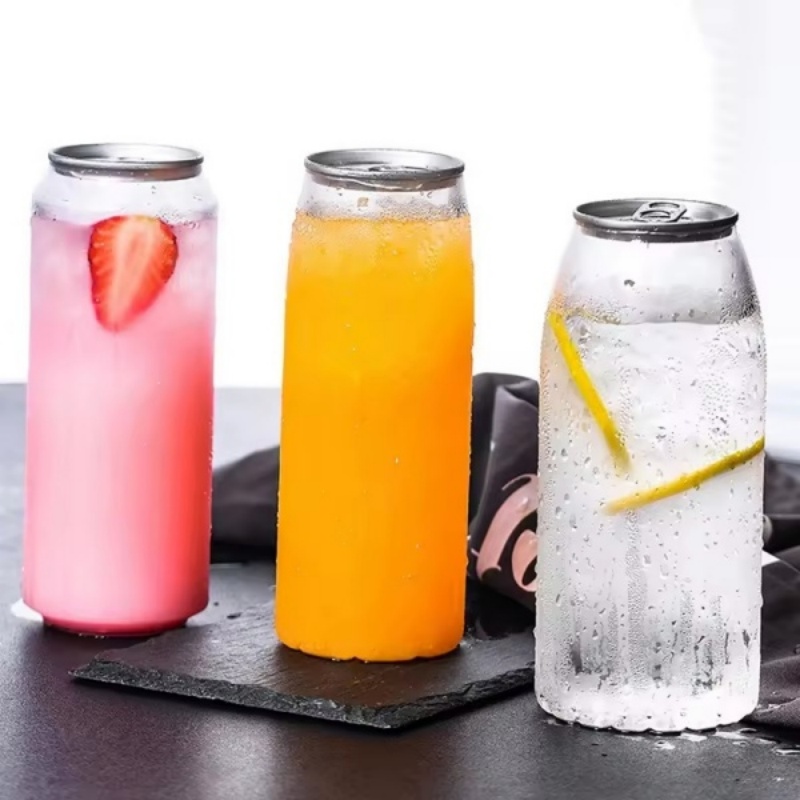
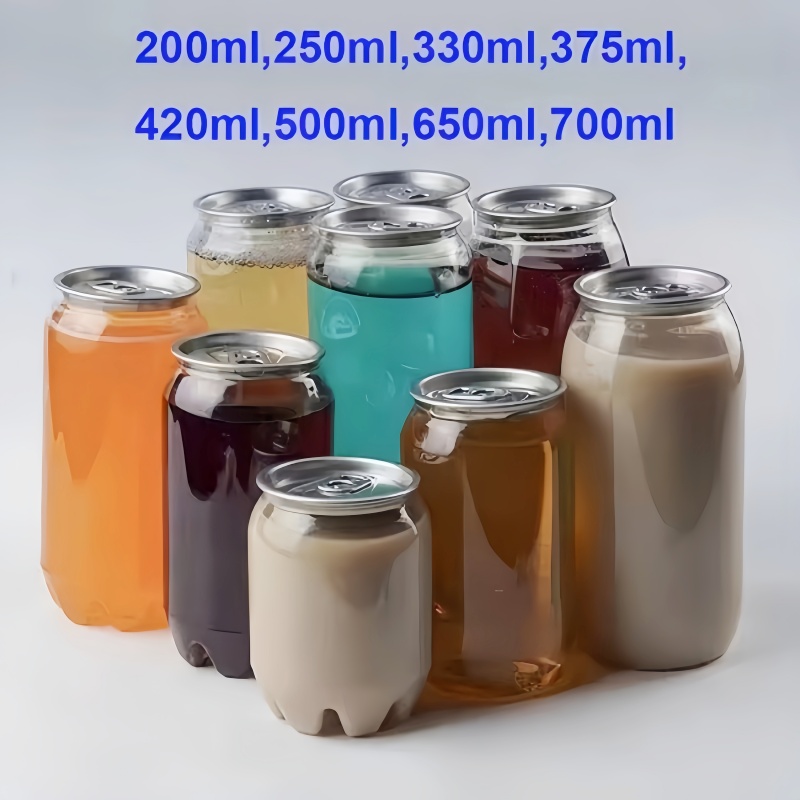
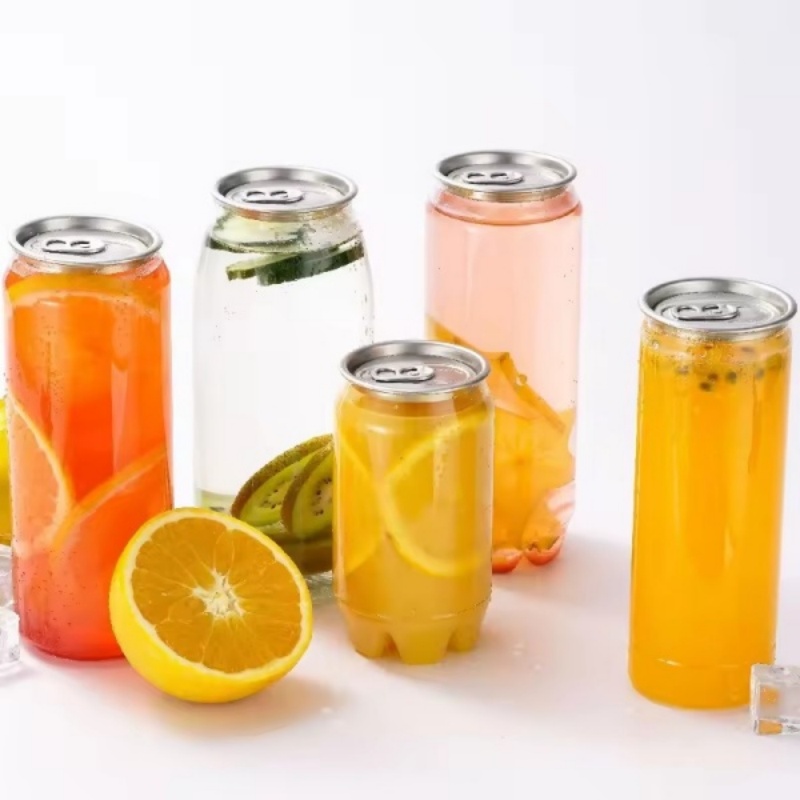
Explore our comprehensive selection of RPET packaging solutions designed for university vending applications
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.