

Leave Your Message
Explore our flagship airtight and transparent rPET beverage cans tailored specifically for high-end boutique hospitality minibars, wellness suites, and poolside executive lounges.
In the contemporary five-star hospitality landscape, the in-room minibar has evolved from a simple convenience into a curated touchpoint of lifestyle luxury, visual elegance, and environmental responsibility. Modern high-net-worth travelers and boutique hotel guests demand transparency, artisanal quality, and rigorous ecological stewardship. The traditional opaque aluminum can or heavyweight single-use glass bottle is no longer the sole standard in premium guestrooms.
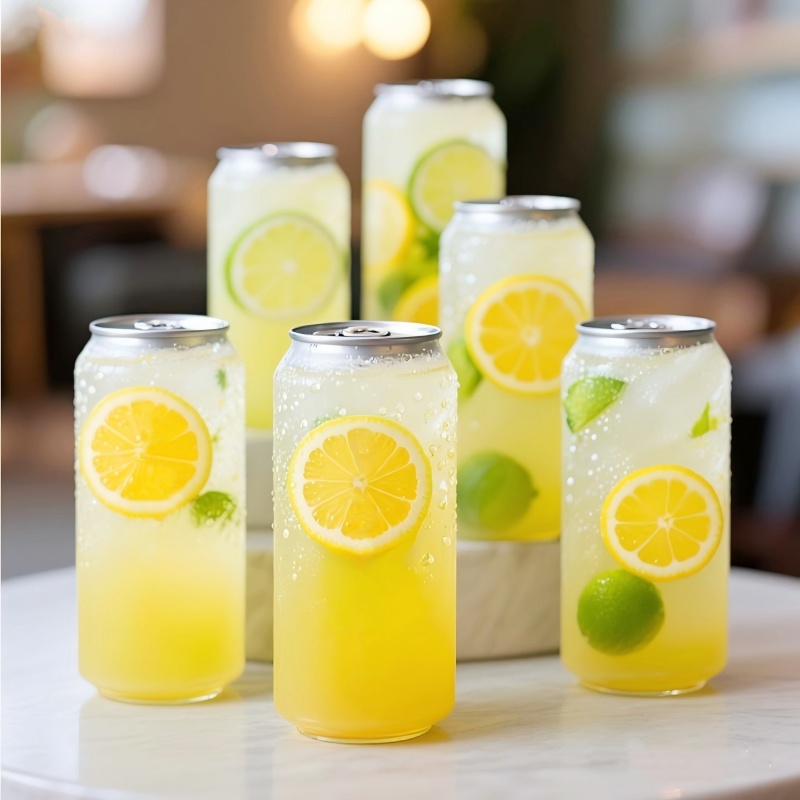
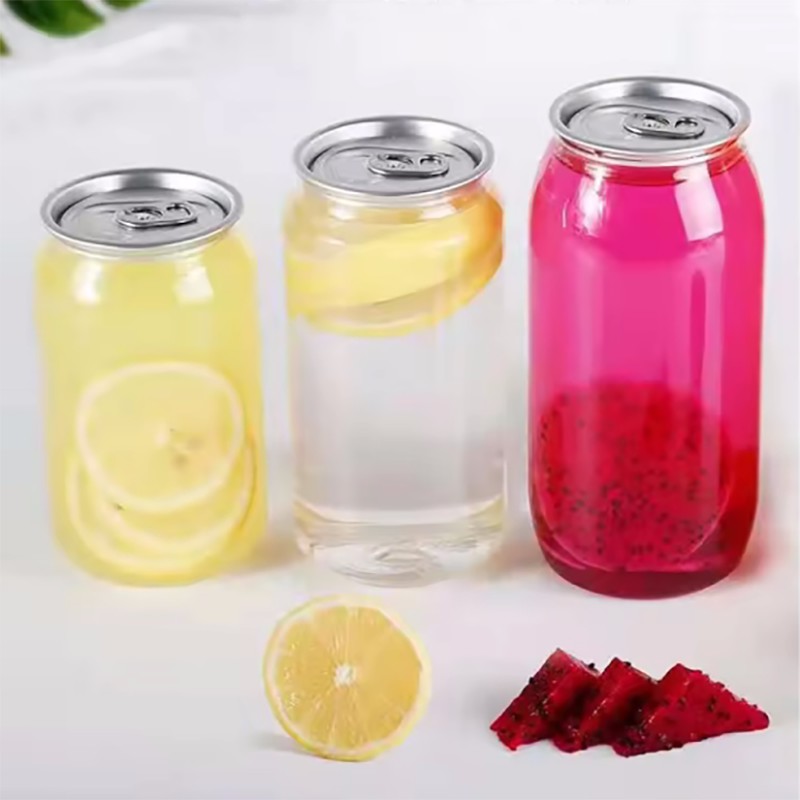
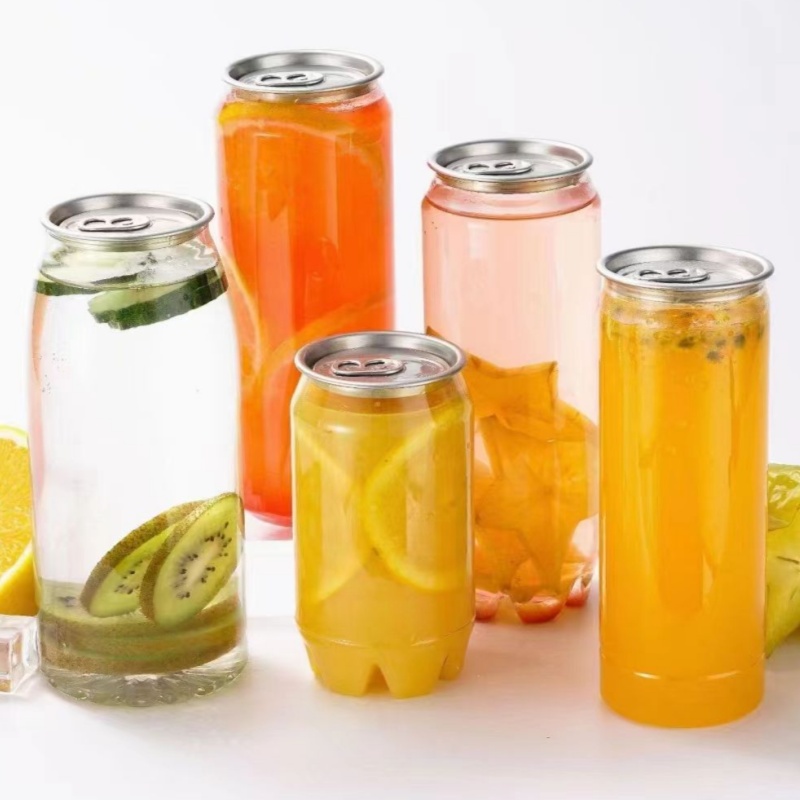
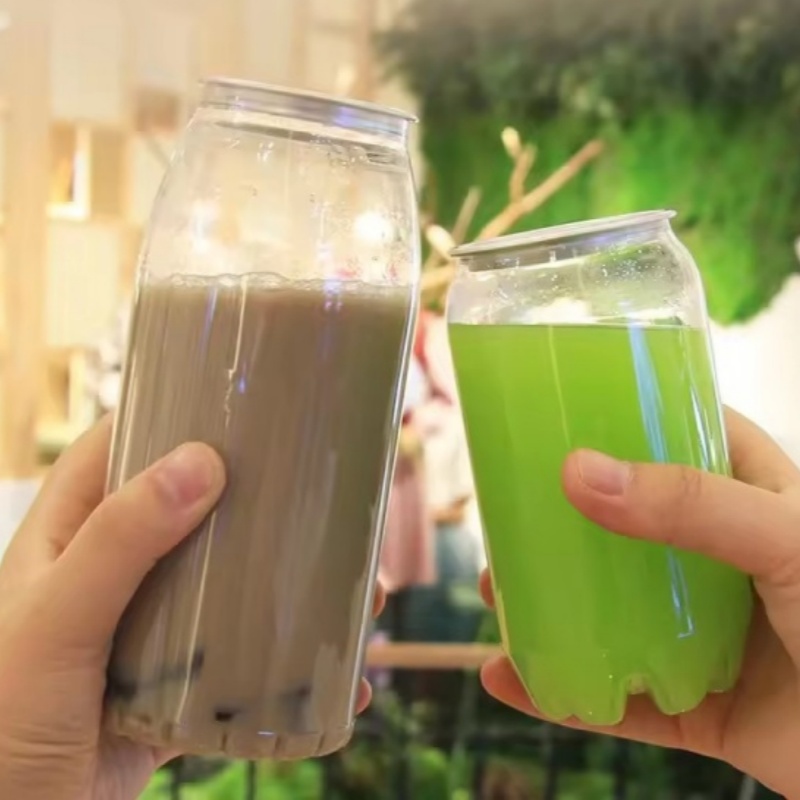
Enter the rPET (Recycled Polyethylene Terephthalate) plastic soda can—an engineering innovation that bridges the tactile satisfaction of an aluminum pull-tab closure with the immaculate clarity of ultra-clear polymer walls. By showcasing the vibrant natural hues of bespoke craft sodas, organic cold-pressed wellness tonics, and sparkling botanical infusions, rPET soda cans dramatically elevate visual merchandising inside illuminated glass-door minibars.
Key Luxury Insight: Modern hospitality data indicates that clear packaging increases guest interaction and impulse purchases in hotel minibars by up to 38% compared to concealed, standard metal packaging.
Showcases premium natural beverage color, botanical garnishes, and effervescence, transforming the minibar into an alluring visual display that commands top-tier pricing.
Utilizing high-grade food-contact rPET drastically diminishes the hotel's carbon footprint, fulfilling stringent corporate ESG and global green hospitality benchmarks.
Eliminates the acute liability of broken glass in guest suites, presidential bathrooms, spa facilities, and outdoor resort cabana minibars.
Behind the sleek aesthetic of the rPET plastic soda can lies sophisticated polymer engineering. When stocking high-velocity luxury minibars, packaging must withstand precise thermal shifts, maintain internal carbonation pressure without deformation, and preserve volatile aromatic compounds over extended storage periods.
Equipped with standardized 200/202 easy-open aluminum ends (EOE) or pop-top closures, rPET cans provide an impenetrable barrier against oxygen ingress and carbon dioxide loss. Whether containing effervescent sparkling mountain water, probiotic kombucha, or nitrogen-infused craft cold brew, the beverage retains its peak crispness and aromatic profile throughout the guest's stay.
Compared to standard glass beverage containers, rPET soda cans achieve a weight reduction of over 80%. For high-rise luxury hotel towers spanning hundreds of rooms, this substantial mass reduction optimizes daily housekeeping restocking cycles, decreases freight logistics expenses, and reduces the physical strain on hospitality service staff.
With compact tabletop machinery such as COPAK’s Intelligent Automatic Can Sealing Machine, premier hotel food & beverage programs can create limited-edition signature in-house cocktails, cold-brew roasts, and fresh juice cleanses, sealed on-site directly into rPET cans for VIP minibar placement.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsEstablished in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
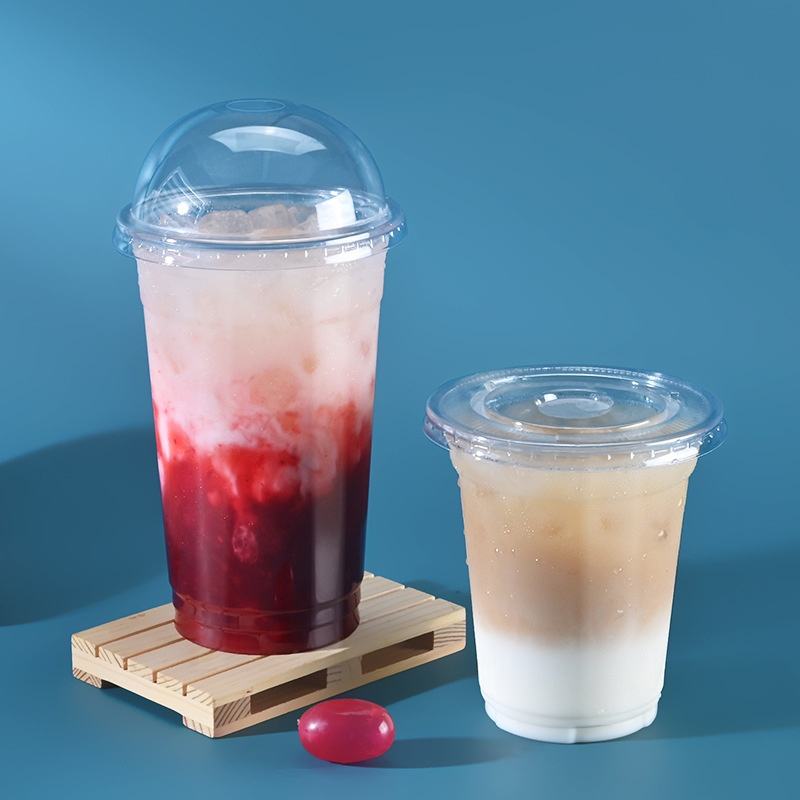
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
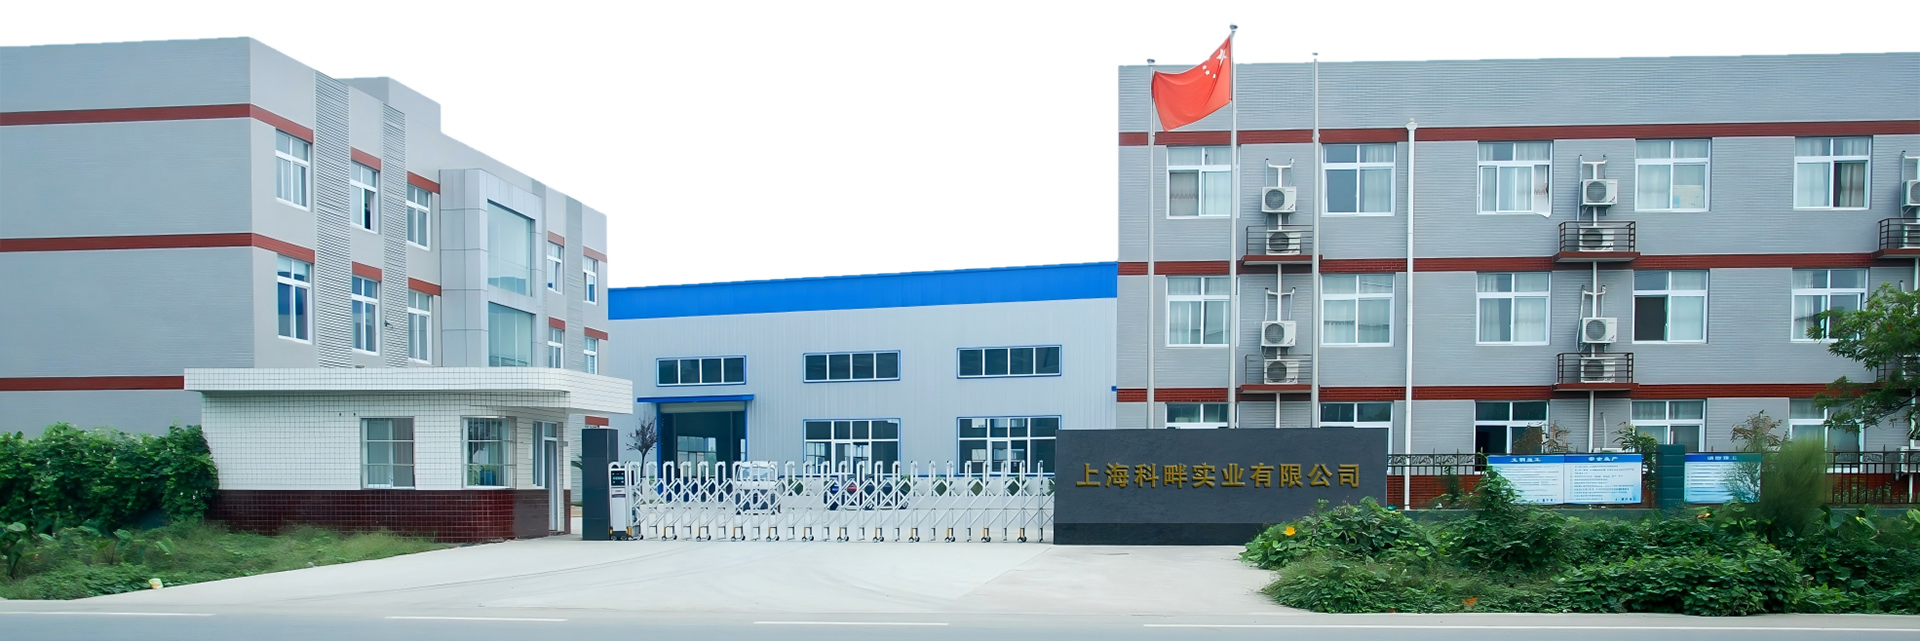
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production for global hospitality distributors.
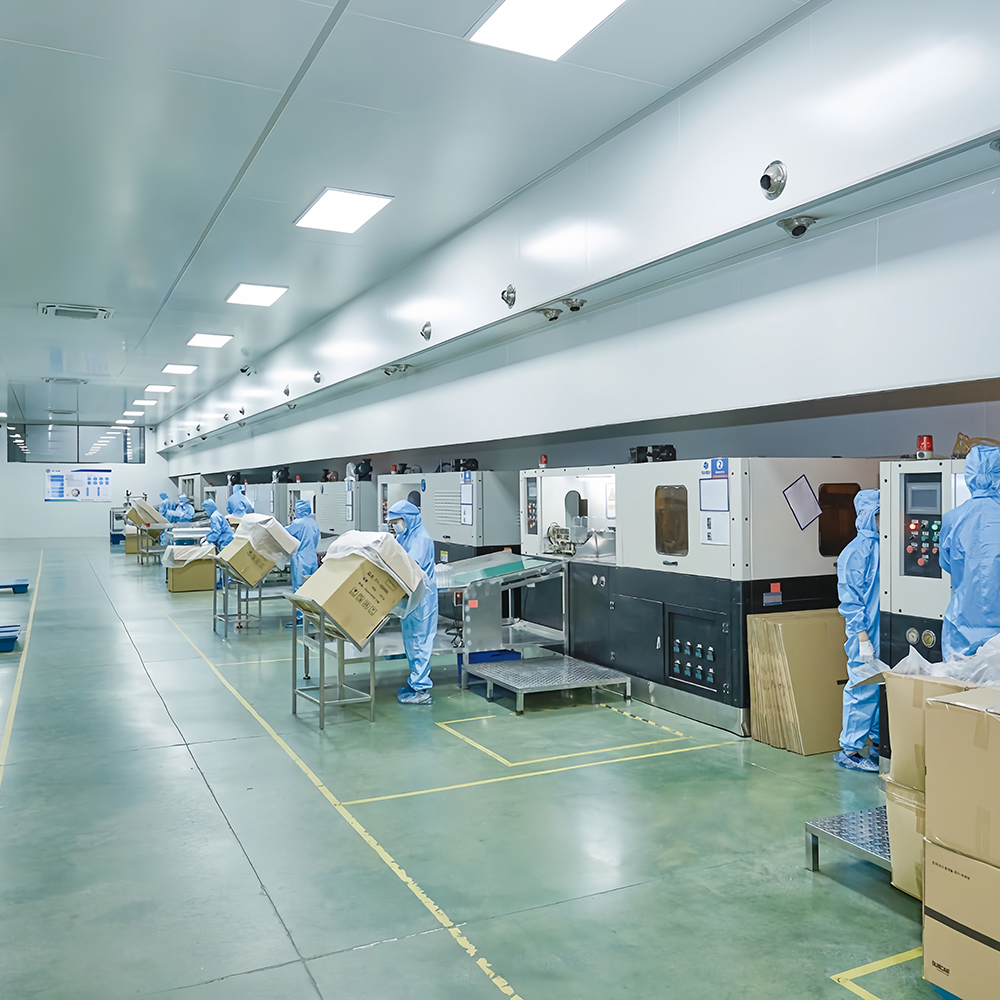
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
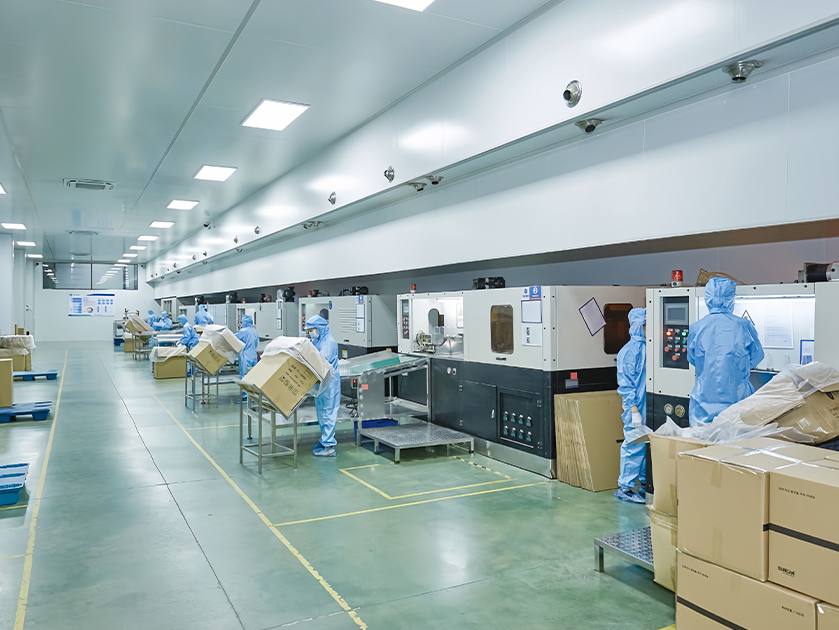
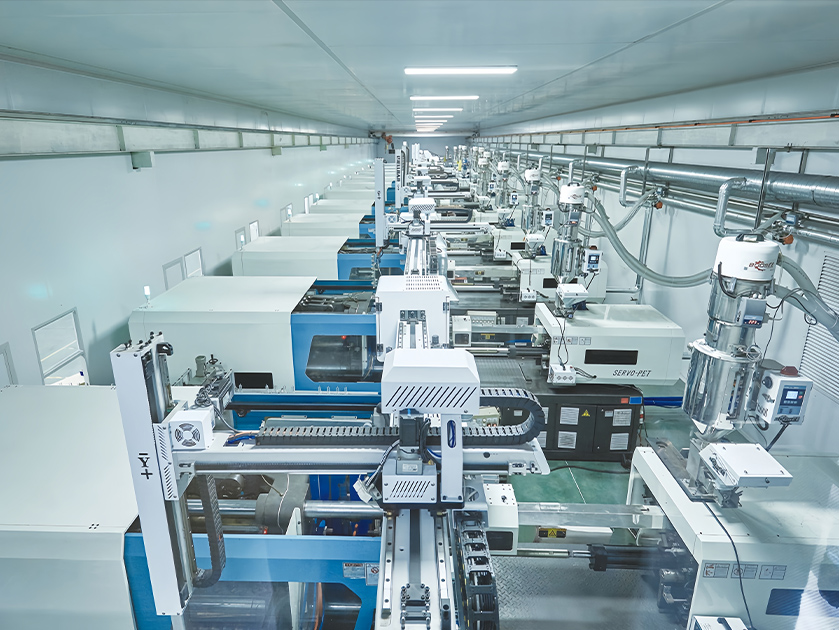
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
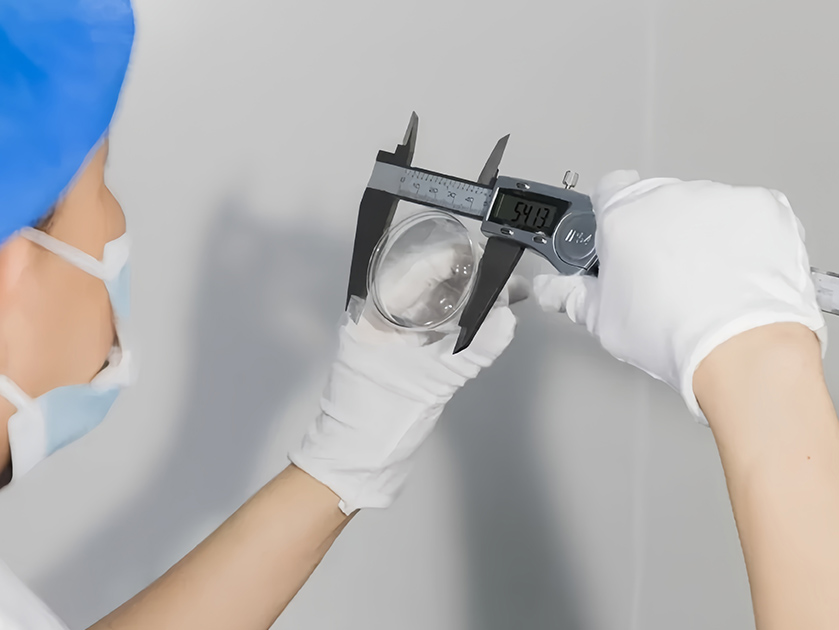
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
We offer extensive customization options to meet the unique requirements of beverage brands and luxury resort clients, including tailored shapes, sizes, and capacities for PET cups and cans. Additionally, we provide full support for custom mold development and personalized printing solutions.
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
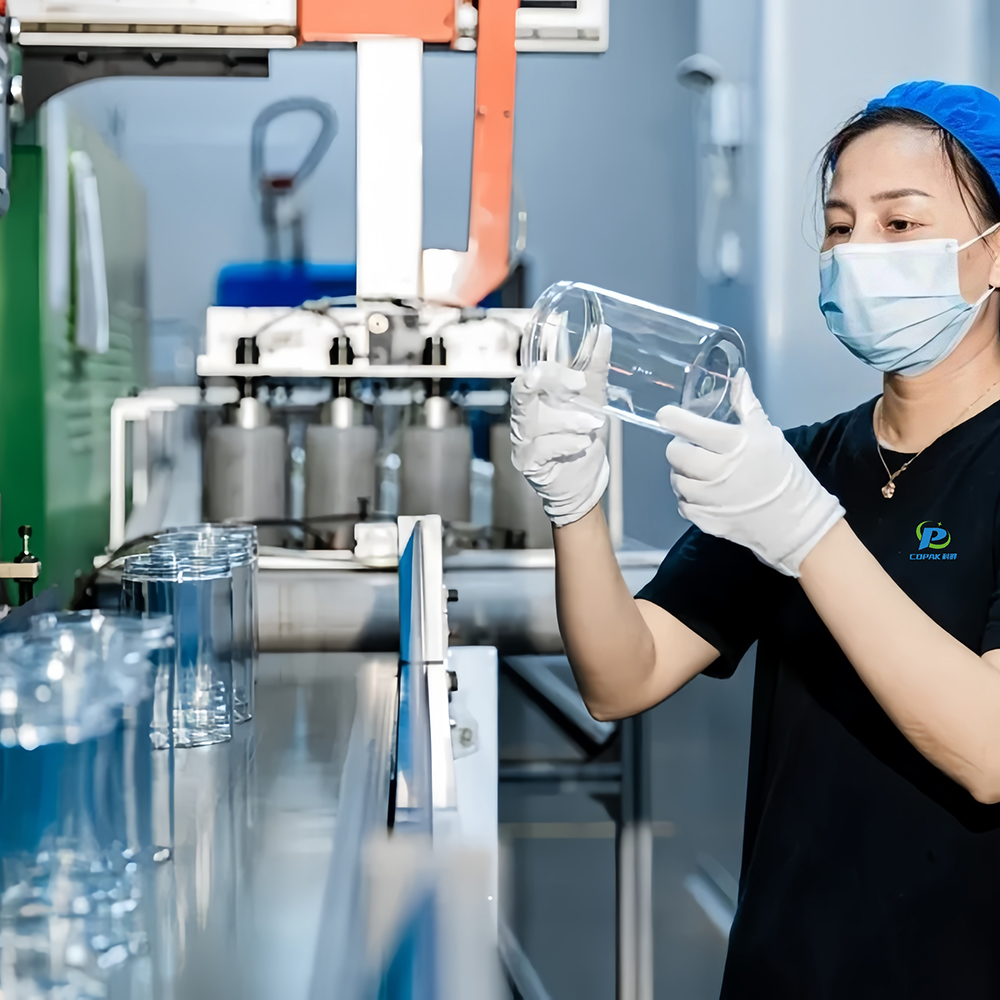
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
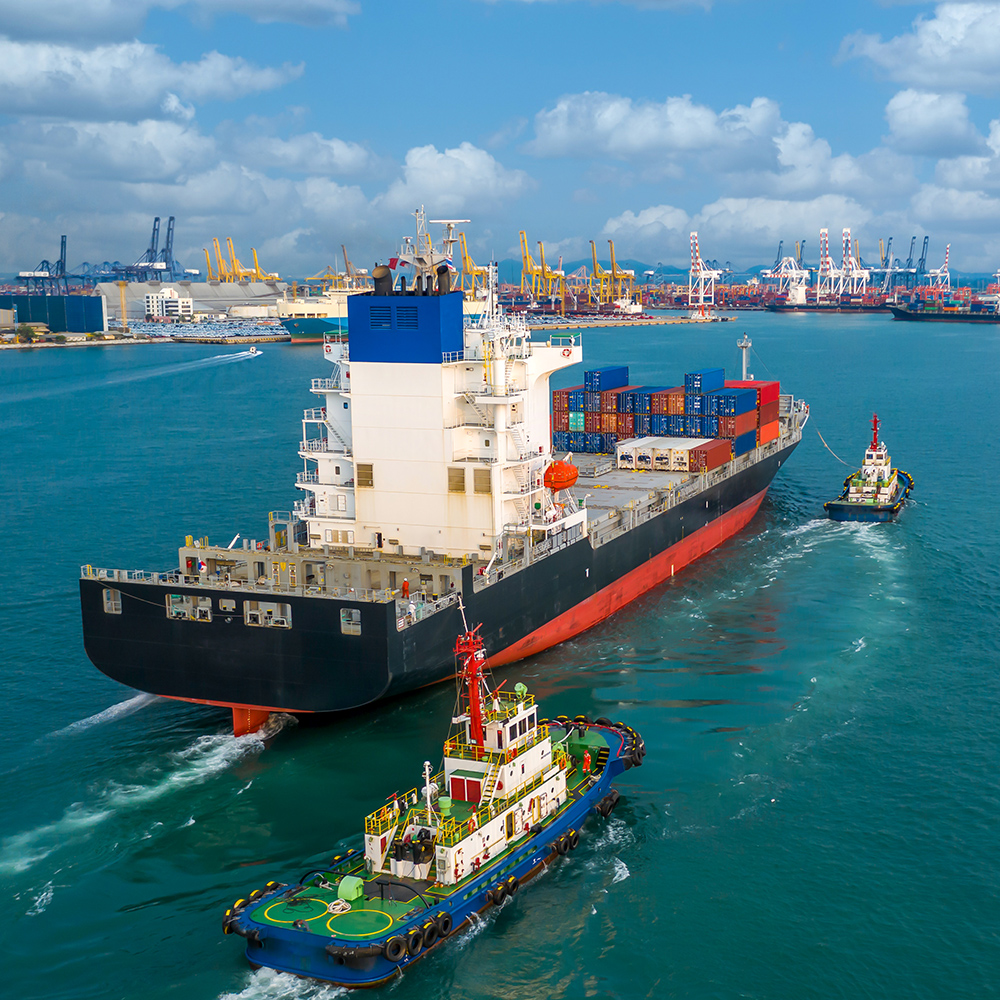
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
Empowering global hospitality partners with high-speed delivery, pristine cleanroom standards, and uncompromising manufacturing integrity.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Browse our complete catalogue of certified rPET soda cans, cold-brew bottles, sealing machines, and premium wholesale cups engineered for luxury hotels.
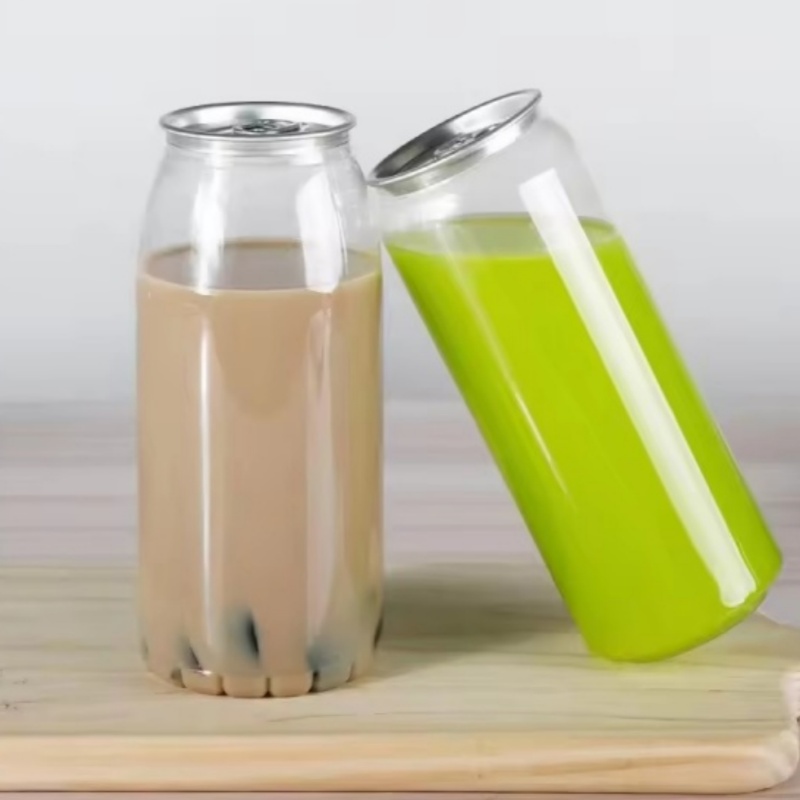
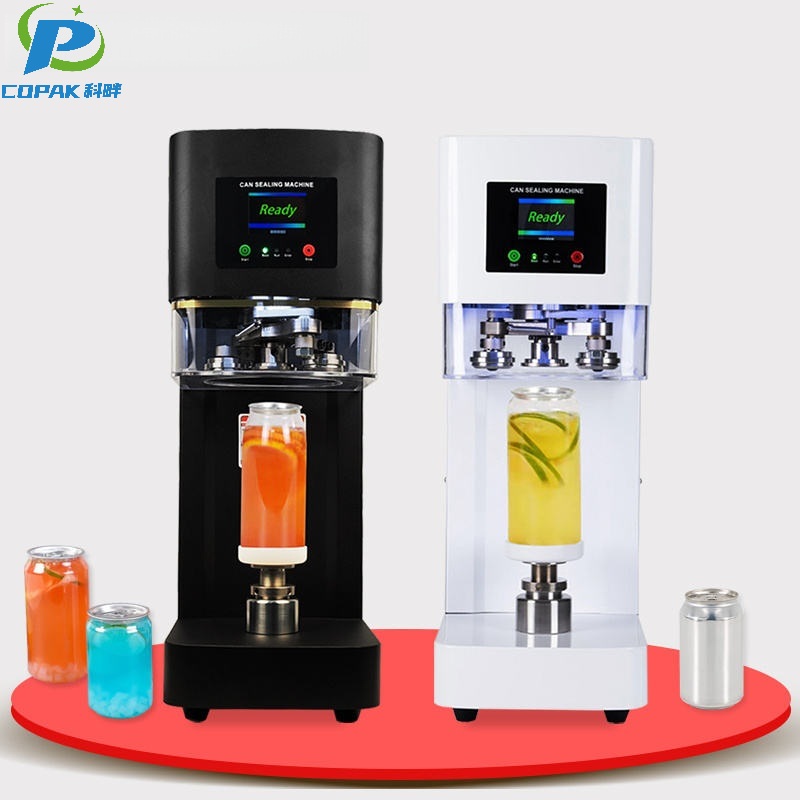
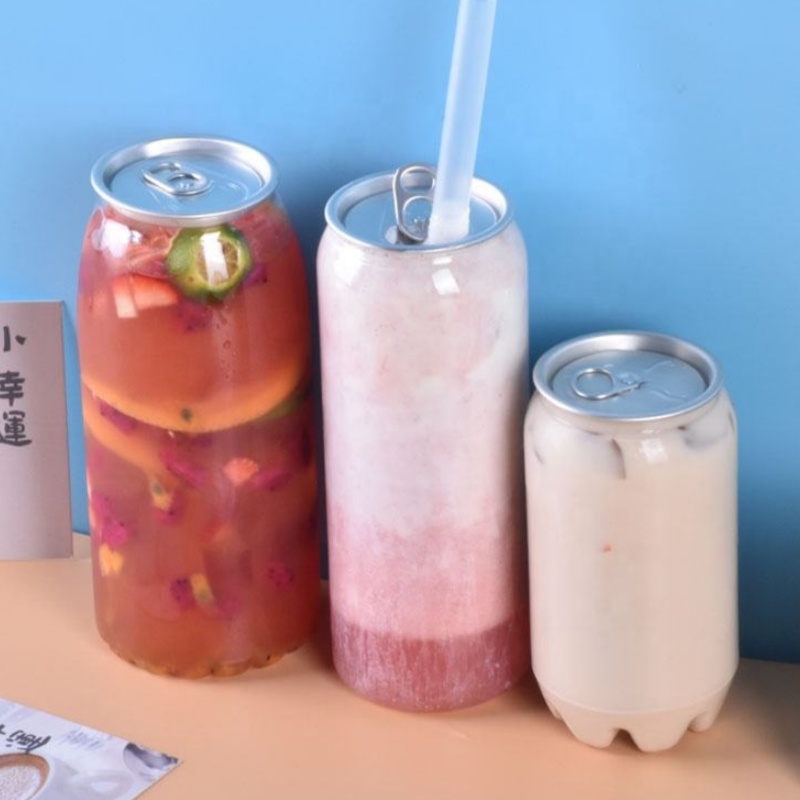
Having supplied PET cups and PET cans to numerous renowned hospitality and beverage brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
INQUIRY NOW