Leave Your Message
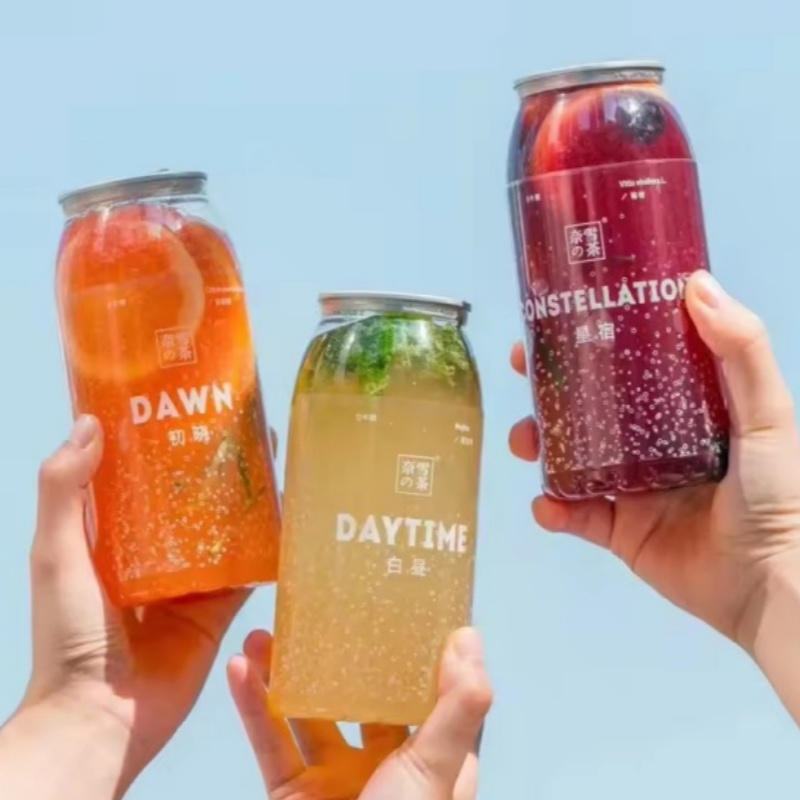
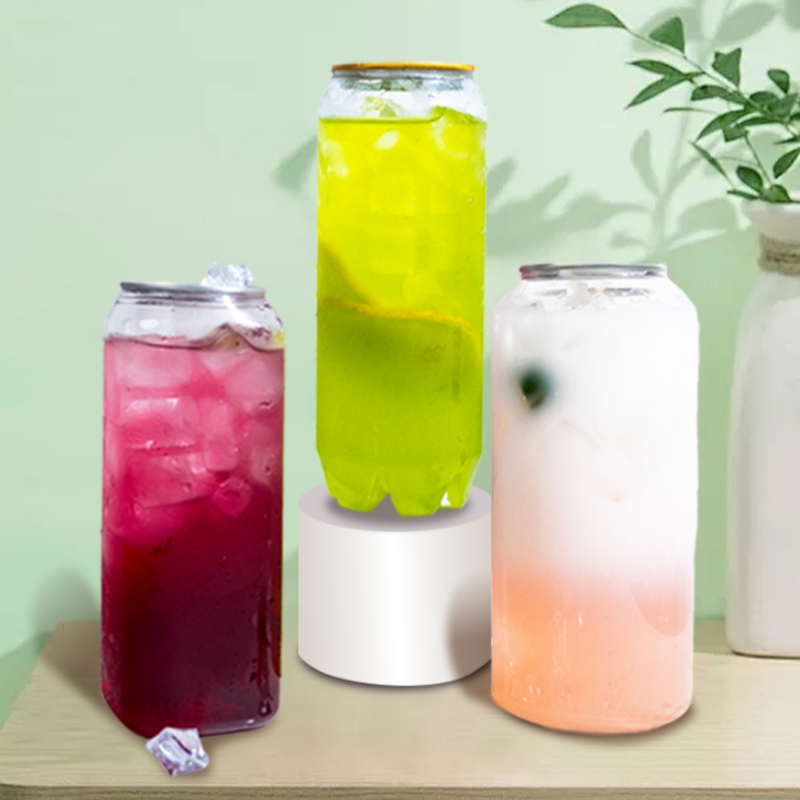
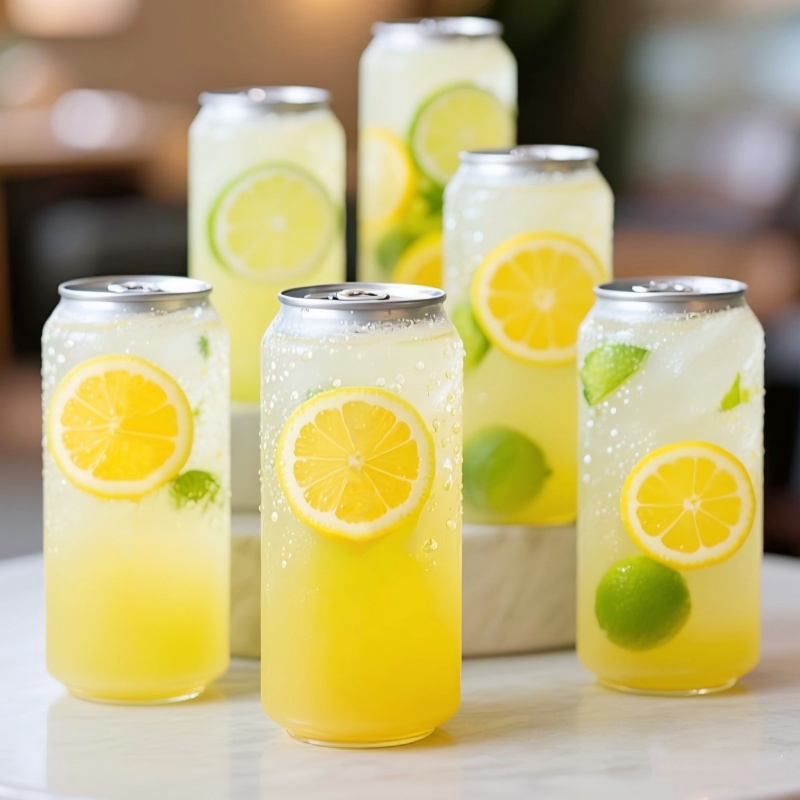
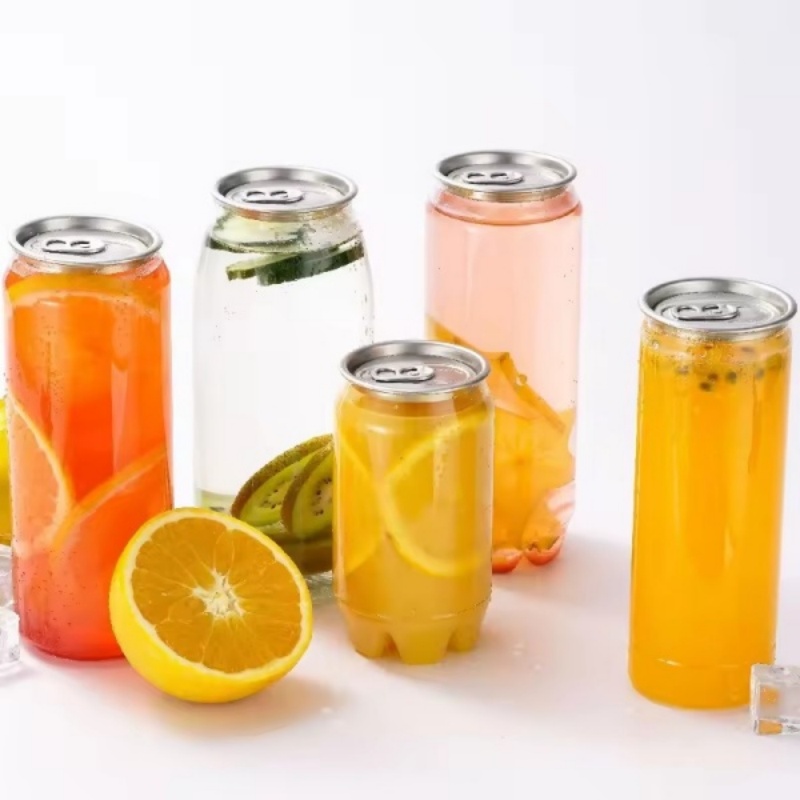
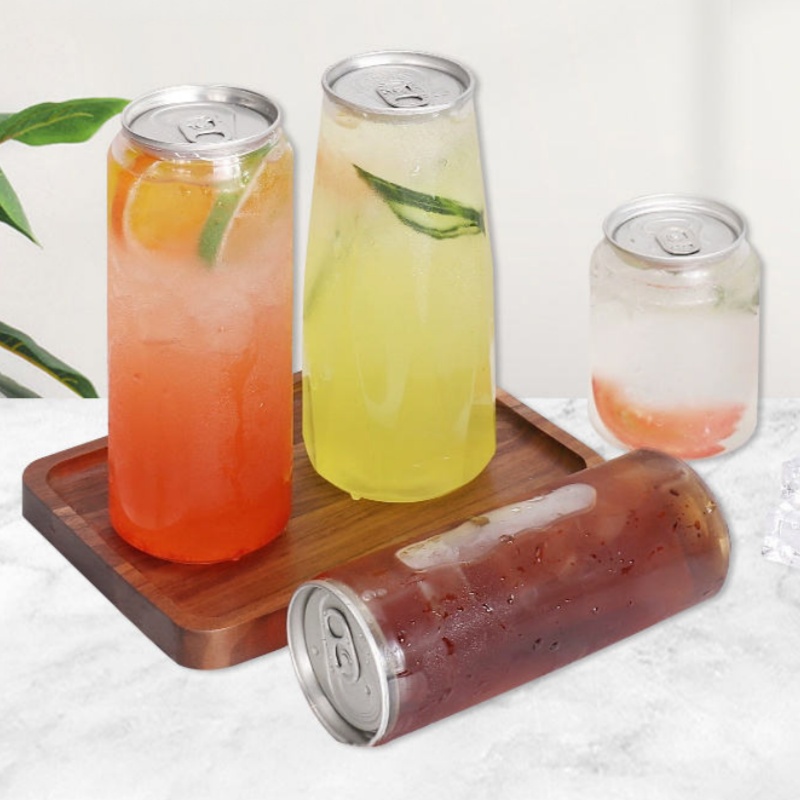
Explore our premium range of RPET plastic soda cans designed specifically for carbonated soft drinks
Understanding the transformative impact of recycled PET plastic soda cans on the beverage industry
The global carbonated soft drinks market continues to experience robust growth, with packaging innovation playing a pivotal role in brand differentiation and sustainability initiatives. RPET (Recycled Polyethylene Terephthalate) plastic soda cans have emerged as a game-changing solution, combining the traditional appeal of aluminum cans with the sustainability benefits of recycled materials and the design flexibility of plastic packaging.
According to recent market analysis, the global PET packaging market for beverages is projected to reach $68.5 billion by 2028, with carbonated soft drinks representing a significant portion of this growth. RPET plastic soda cans are increasingly preferred by major beverage brands seeking to meet consumer demands for sustainable packaging while maintaining product integrity and visual appeal.
The shift toward RPET packaging is driven by several key factors: enhanced recyclability rates, reduced carbon footprint compared to virgin PET production, improved barrier properties for carbonation retention, and the ability to incorporate up to 100% recycled content without compromising structural integrity or safety standards.
Circular Economy Integration: Leading beverage manufacturers are increasingly adopting closed-loop recycling systems, where RPET soda cans are collected, processed, and remanufactured into new packaging. This circular approach significantly reduces waste and environmental impact while creating economic value from recycled materials.
Advanced Barrier Technologies: Modern RPET plastic soda cans incorporate sophisticated multi-layer structures and barrier coatings that effectively preserve carbonation levels, extend shelf life, and protect beverage quality. These innovations ensure that RPET cans perform comparably to or better than traditional aluminum alternatives.
Lightweight Design Innovation: Through advanced engineering and material optimization, RPET soda cans achieve significant weight reduction compared to glass and aluminum packaging, resulting in lower transportation costs, reduced fuel consumption, and decreased overall environmental footprint throughout the supply chain.
Exploring the diverse uses of RPET plastic soda cans across the carbonated beverage industry
RPET plastic soda cans are ideally suited for classic carbonated beverages including colas, lemon-lime sodas, orange drinks, and root beers. The excellent barrier properties maintain carbonation levels throughout the product's shelf life while the transparent design showcases the beverage's appealing color.
The energy drink segment has rapidly embraced RPET packaging due to its modern aesthetic appeal and sustainability credentials that resonate with health-conscious, environmentally aware consumers. The packaging's durability ensures safe handling during active lifestyles and sports activities.
The booming sparkling water market benefits significantly from RPET cans' crystal-clear appearance, which communicates purity and natural ingredients. The packaging's lightweight nature aligns perfectly with the health-focused positioning of these beverages while maintaining excellent carbonation retention.
Retail and Convenience Stores: RPET plastic soda cans are optimized for retail environments with eye-catching designs, stackable formats, and secure sealing systems that prevent tampering. Their shatter-resistant properties reduce product loss and enhance safety in high-traffic retail settings.
Food Service and Hospitality: Restaurants, cafeterias, and entertainment venues increasingly adopt RPET cans for their convenience, portion control, and premium presentation. The packaging eliminates the need for glassware while maintaining an upscale appearance suitable for various service environments.
Vending Machine Distribution: The standardized dimensions and durable construction of RPET plastic soda cans make them ideal for automated vending systems, ensuring reliable dispensing while the transparent design allows consumers to clearly identify products before purchase.
Event and Festival Catering: Large-scale events benefit from RPET cans' safety advantages over glass and aluminum, reducing injury risks while supporting event sustainability goals. The lightweight packaging also simplifies logistics and waste management at temporary venues.
Advancing RPET technology to meet evolving industry demands and sustainability objectives
Cutting-edge research in polymer engineering has led to the development of enhanced RPET formulations with improved mechanical properties, superior barrier performance, and increased heat resistance. These innovations enable RPET plastic soda cans to withstand hot-fill processes and pasteurization, expanding their application range to include beverages requiring thermal treatment.
Nanotechnology integration is revolutionizing RPET packaging through the incorporation of nano-scale barrier layers that dramatically enhance oxygen and carbon dioxide impermeability. This technology extends product shelf life while maintaining the material's recyclability and sustainability credentials.
The convergence of RPET packaging with digital technologies is creating intelligent packaging solutions that enhance consumer engagement and supply chain visibility. QR codes, NFC tags, and temperature-sensitive indicators can be seamlessly integrated into RPET cans, providing real-time product information, authentication, and freshness monitoring.
Augmented reality (AR) enabled RPET packaging transforms consumer interaction by delivering immersive brand experiences, nutritional information, and recycling instructions through smartphone applications, strengthening brand loyalty while promoting responsible disposal practices.
Advanced manufacturing techniques including precision injection molding, optimized blow molding, and energy-efficient production systems are reducing the environmental footprint of RPET can production. These processes minimize material waste, lower energy consumption, and enable higher recycled content incorporation.
Chemical recycling technologies are emerging as complementary solutions to mechanical recycling, breaking down contaminated or mixed plastic waste into molecular building blocks that can be repolymerized into virgin-quality RPET, creating truly circular material flows.
Industry analysts project that RPET plastic soda cans will capture an increasingly significant market share over the next decade, driven by stringent environmental regulations, corporate sustainability commitments, and evolving consumer preferences. The European Union's Single-Use Plastics Directive and similar legislation worldwide are accelerating the transition toward recyclable and recycled packaging materials.
Beverage manufacturers are investing heavily in RPET infrastructure, with major brands committing to achieve 25-50% recycled content in their packaging by 2025 and 100% recyclable packaging by 2030. These commitments are creating substantial demand for high-quality RPET materials and advanced manufacturing capabilities.
Emerging markets in Asia-Pacific and Latin America represent significant growth opportunities as rising disposable incomes, urbanization, and environmental awareness drive demand for premium, sustainable beverage packaging. Local production facilities and regional supply chains are being established to serve these expanding markets efficiently.
Meeting international standards for food-grade packaging and environmental responsibility
RPET plastic soda cans manufactured for carbonated beverages must comply with rigorous food contact material regulations established by authorities including the U.S. FDA (Food and Drug Administration), European Food Safety Authority (EFSA), and equivalent agencies worldwide. These regulations ensure that packaging materials do not migrate harmful substances into beverages and maintain product safety throughout the distribution chain.
Comprehensive testing protocols evaluate RPET materials for migration limits of specific substances, overall migration levels, sensory properties, and compatibility with various beverage formulations including acidic, carbonated, and flavored drinks. Third-party laboratory certification provides independent verification of compliance with applicable standards.
ISO 9001 quality management systems ensure consistent production processes and continuous improvement. ISO 14001 environmental management certification demonstrates commitment to minimizing environmental impact throughout manufacturing operations.
HACCP (Hazard Analysis Critical Control Points) certification ensures systematic food safety management. BRC (British Retail Consortium) and FSSC 22000 certifications validate comprehensive food safety and quality management systems.
RecyClass certification verifies packaging recyclability and compatibility with existing recycling infrastructure. Carbon footprint certifications quantify and validate greenhouse gas emissions reduction achievements.

Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
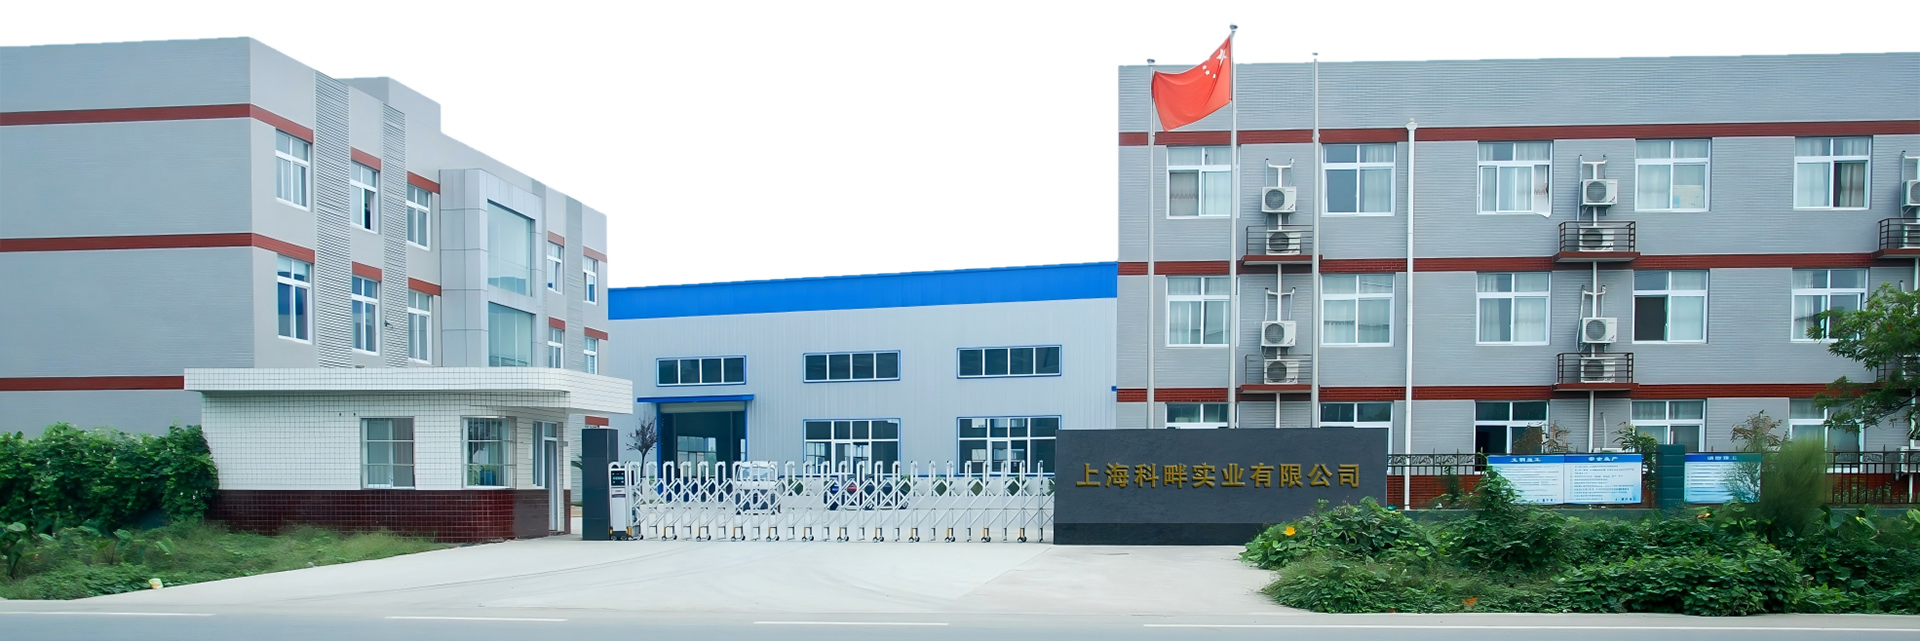
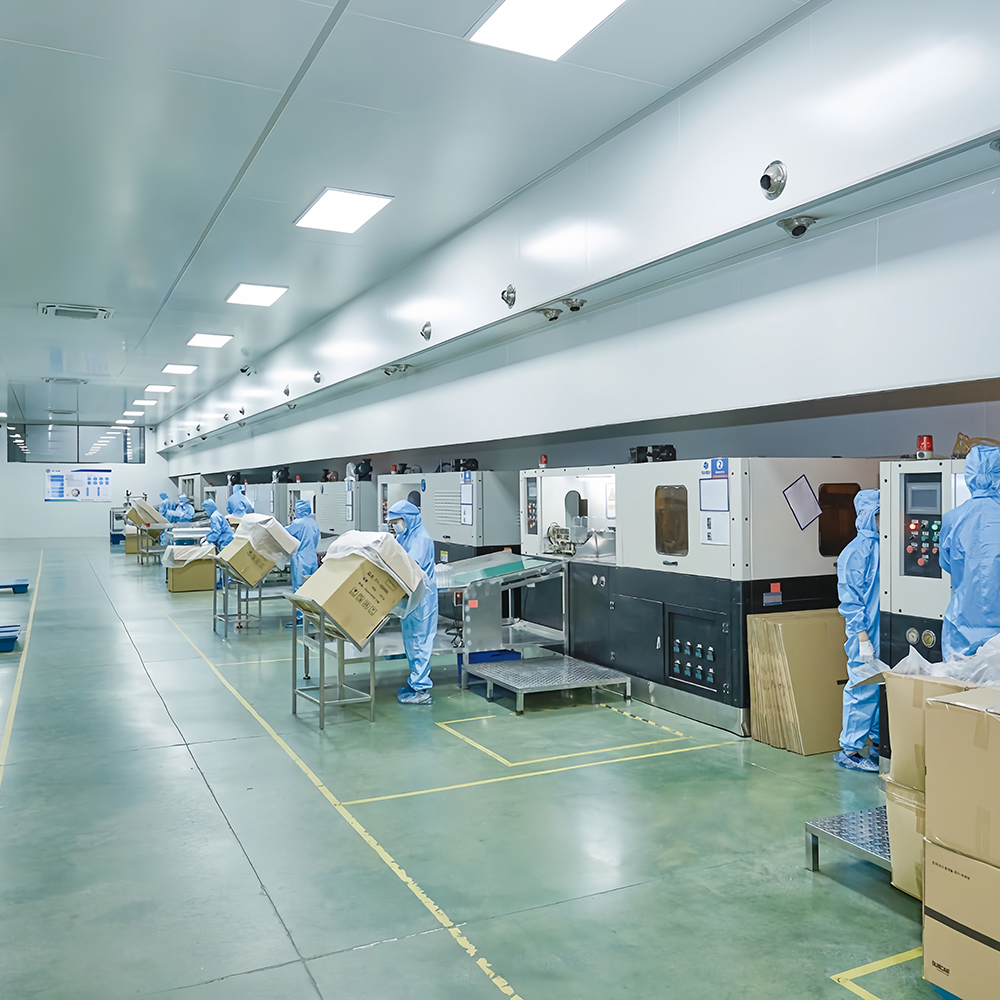
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
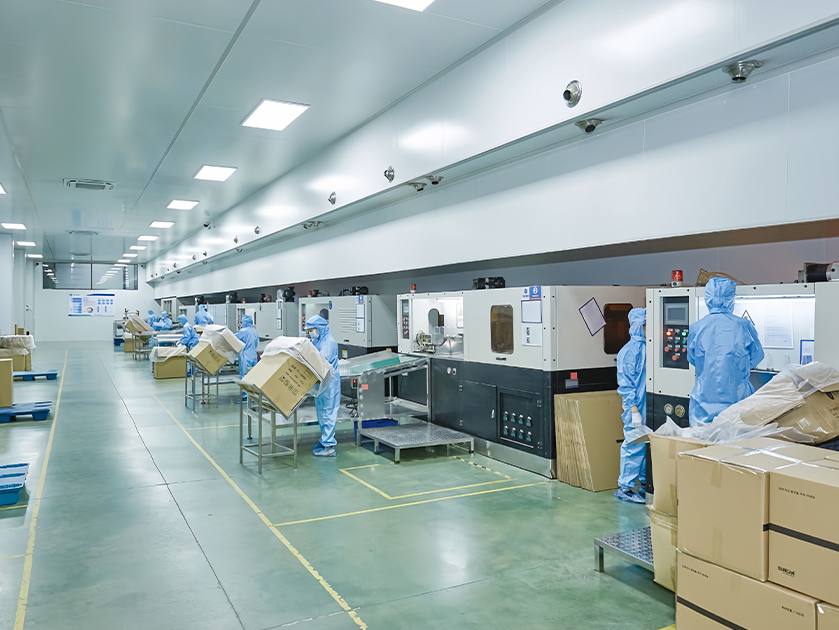
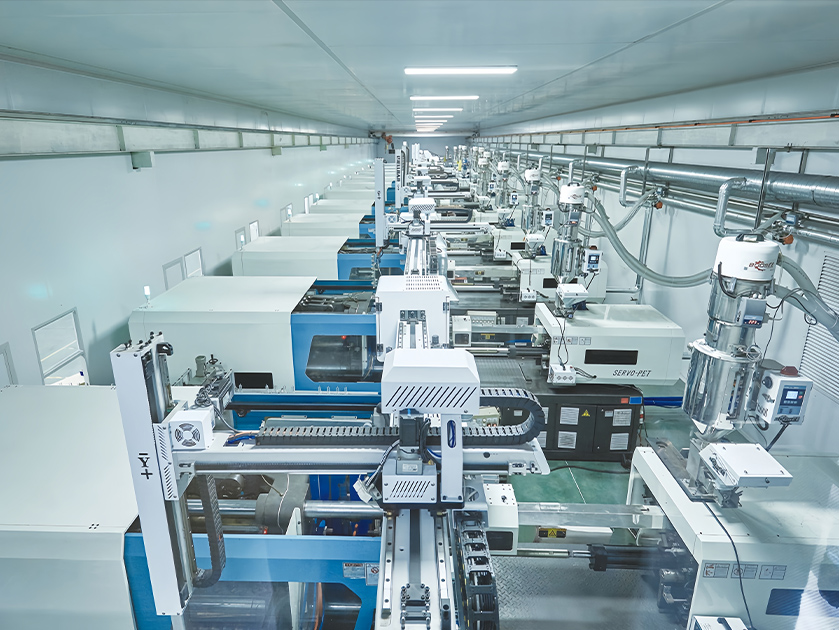
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
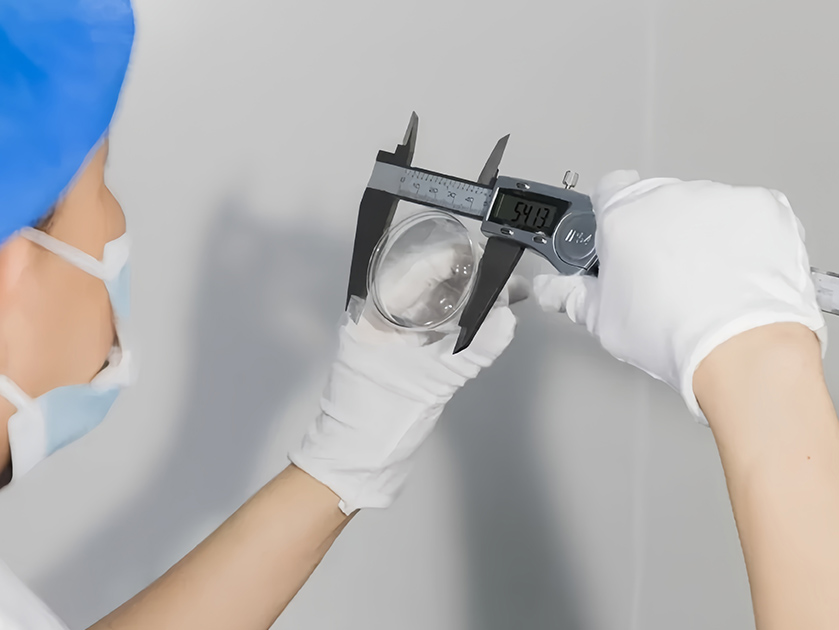
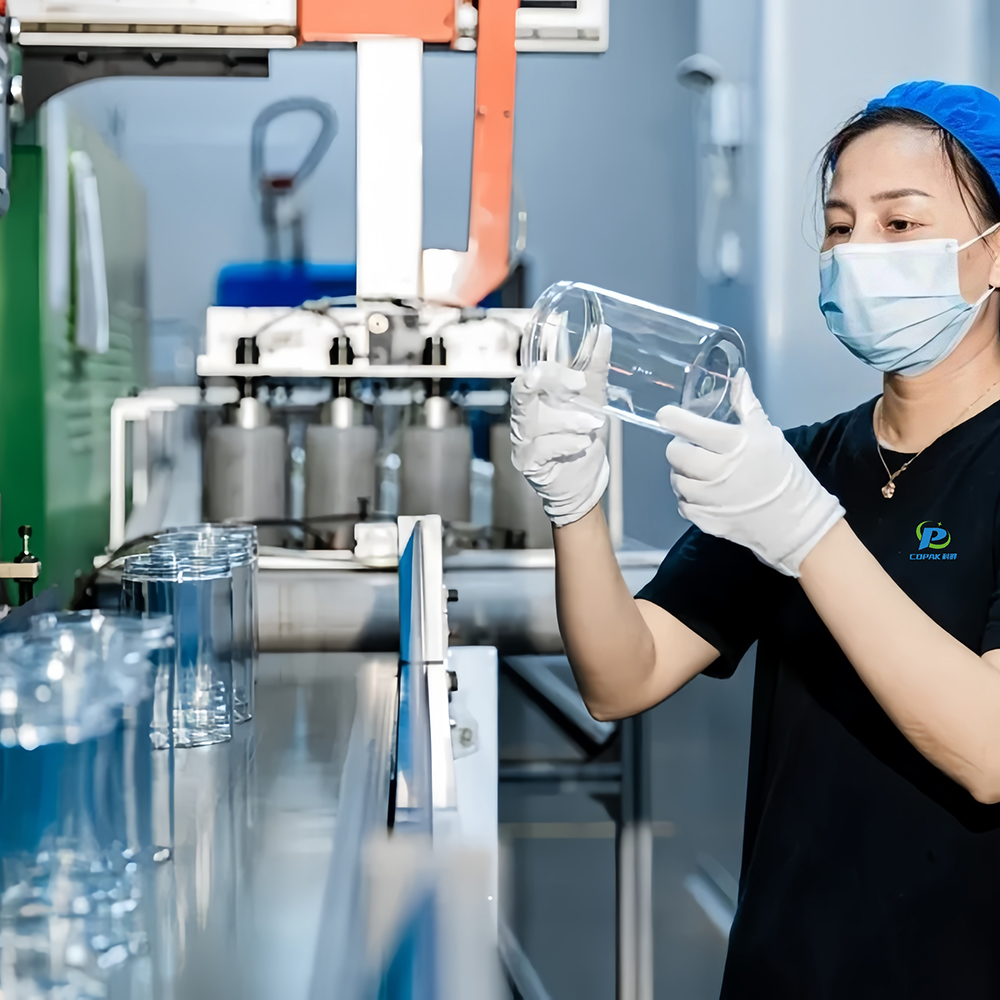
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsAdhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Discover our comprehensive range of PET packaging solutions for diverse beverage applications
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.