

Leave Your Message
In recent years, the beverage packaging industry has witnessed a significant shift towards sustainability and environmental responsibility. Among emerging innovations, recyclable PET (Polyethylene Terephthalate) cans have captured increasing attention as a viable alternative to traditional aluminum cans and glass bottles, especially for beverages like sparkling mineral water. These recyclable PET cans combine the benefits of lightweight design, durability, and full recyclability, aligning perfectly with both consumer demands and regulatory trends across global markets.
As governments worldwide implement stricter packaging waste regulations and consumers increasingly prefer eco-friendly options, manufacturers and beverage brands are eagerly adapting their packaging strategies. Recyclable PET cans provide a sustainable packaging solution that meets both environmental and performance criteria:
The sparkling mineral water segment is at the forefront of adopting recyclable PET cans, influenced by several key trends:
Beyond standard retail packaging, recyclable PET cans are unlocking novel applications that benefit producers, suppliers, and consumers alike:
Recyclable PET cans represent a step forward in circular economy principles. Key advantages include:
While recyclable PET cans present many benefits, industry players are actively innovating to address challenges such as:
Looking ahead, recyclable PET cans are expected to gain larger market share in sparkling mineral water packaging due to their blend of sustainability, convenience, and innovation. Industry experts predict:
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities — from 1oz to 32oz — available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
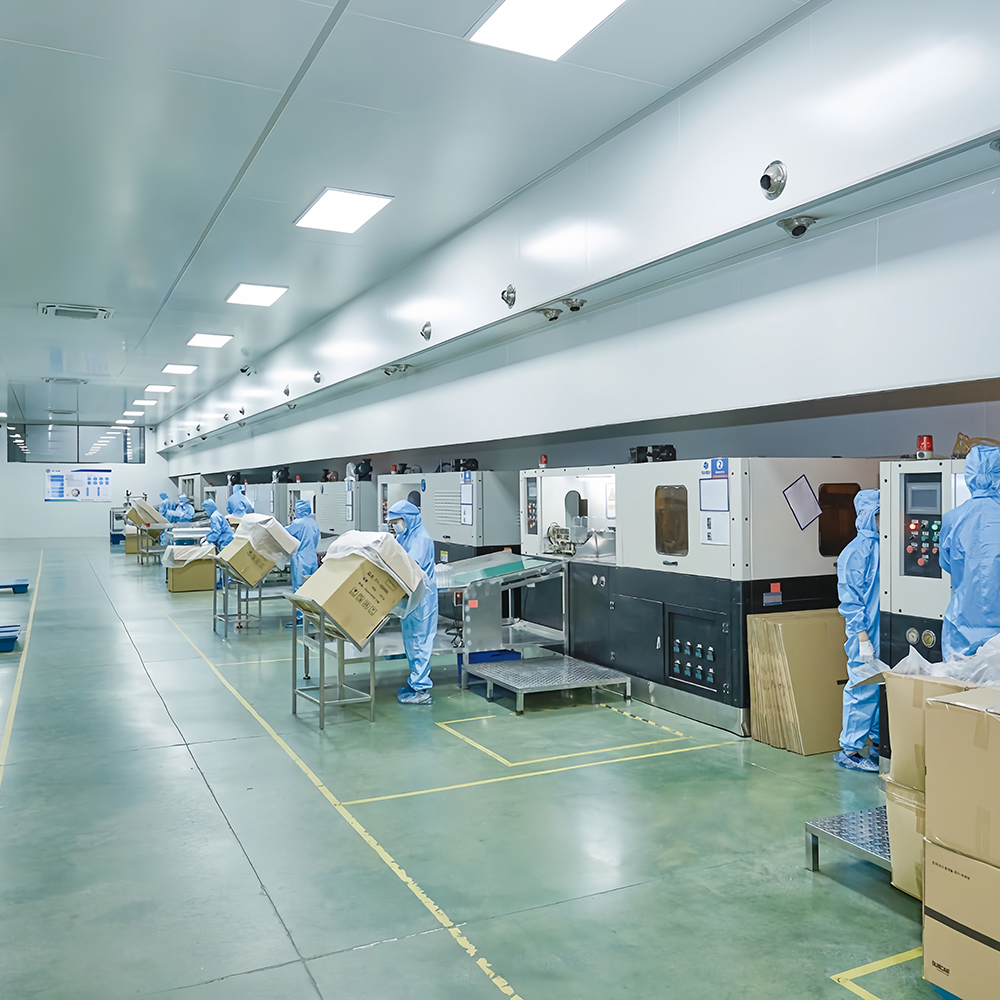
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production.
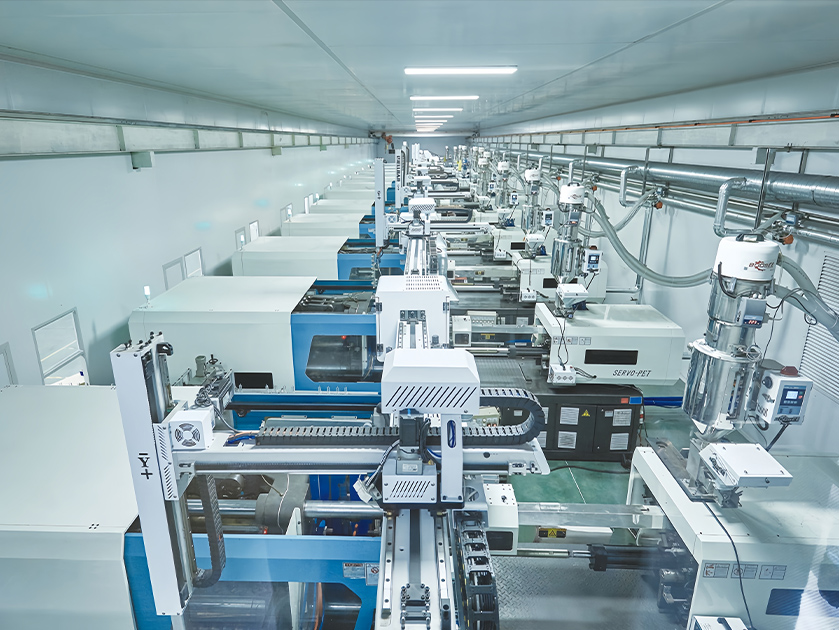
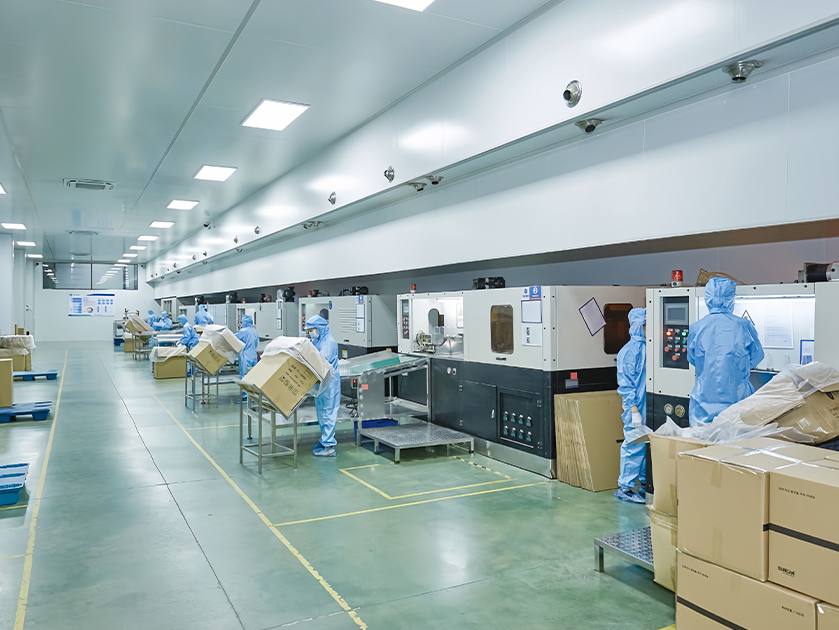
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
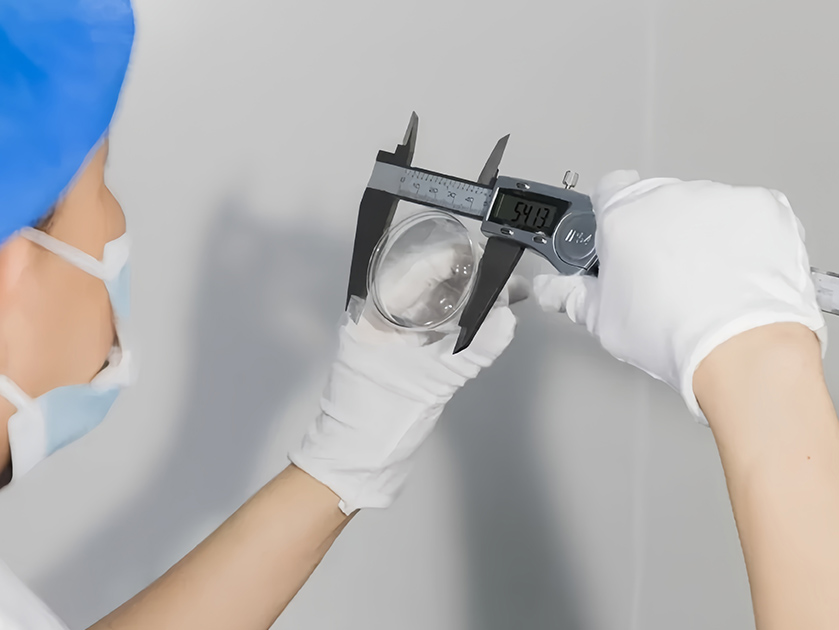
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
We offer extensive customization options to meet the unique requirements of beverage brands and clients, including tailored shapes, sizes, and capacities for PET cups and cans. Additionally, we provide full support for custom mold development and personalized printing solutions.
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
 Contact us
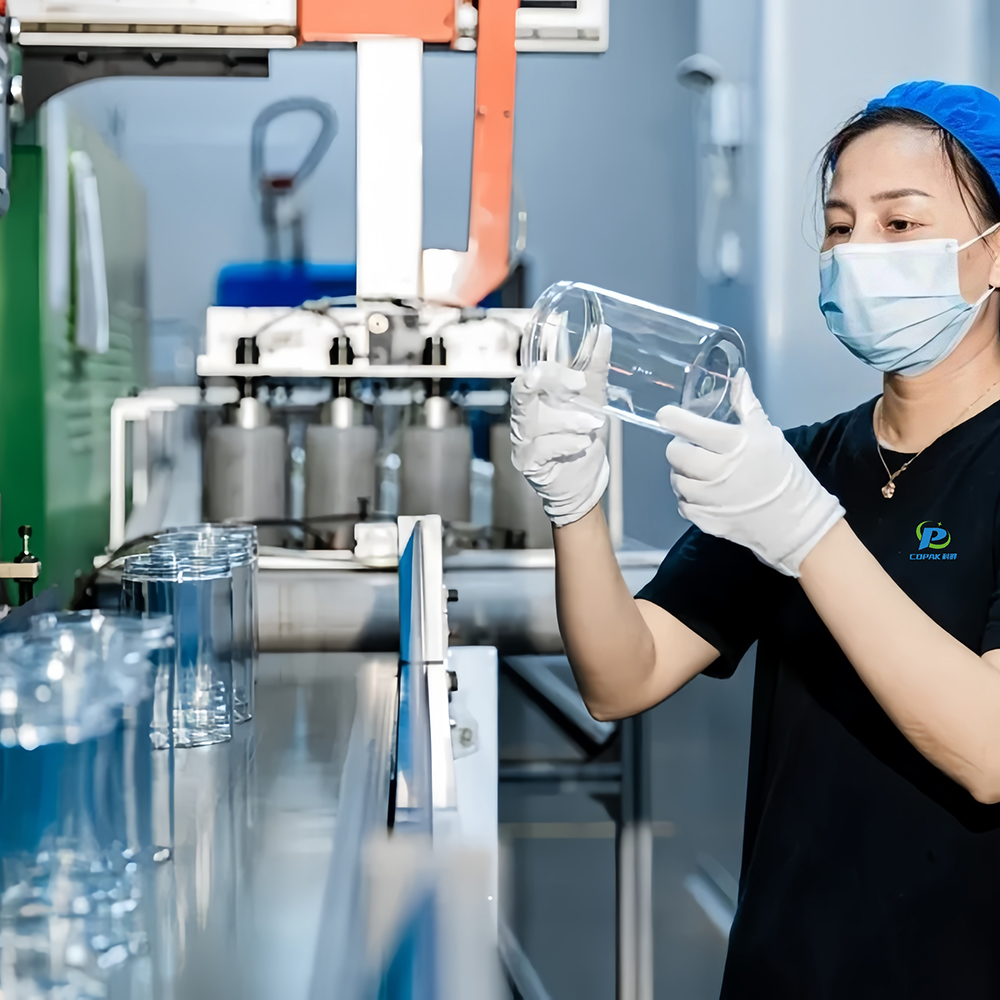
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
 Contact us
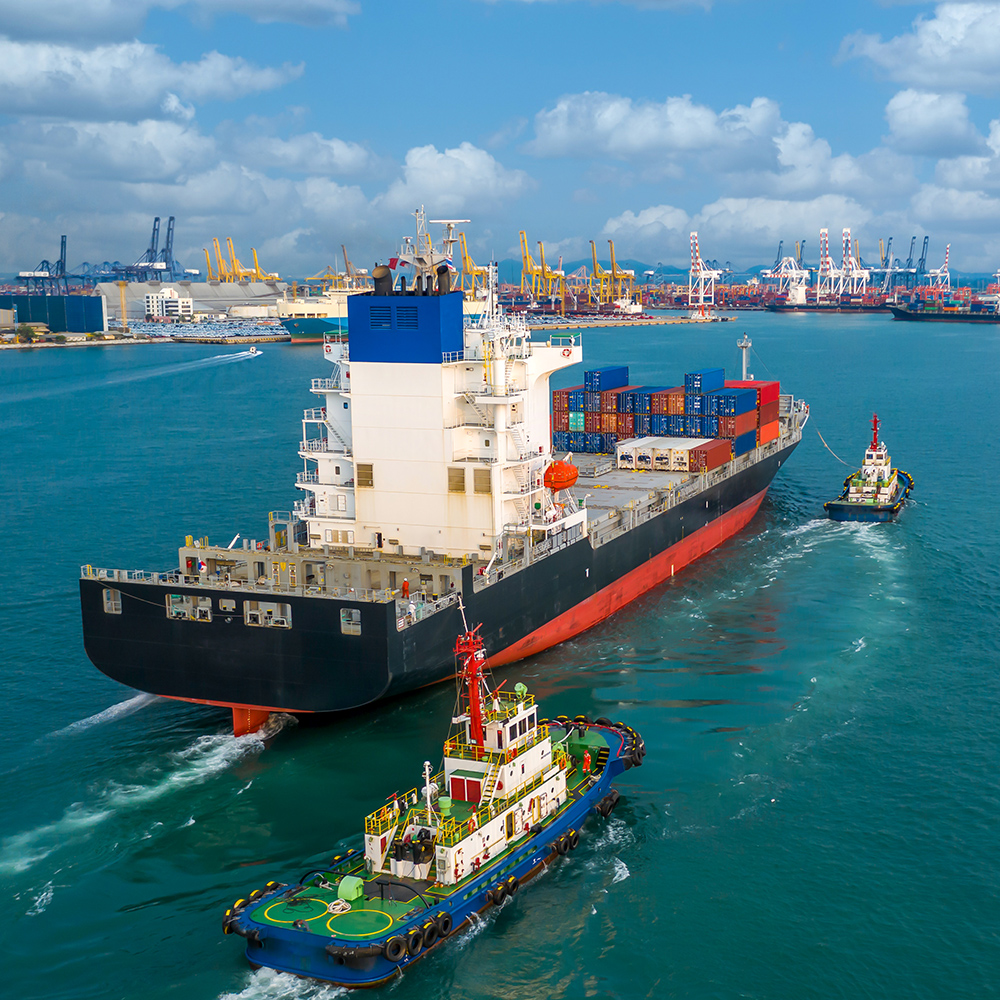
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
 Contact us

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Having supplied PET cups and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
 55mm PET cold cups with 202# lids
 Recycled PET Plastic Cups Wholesale
 500ml Pet Beverage Cans Wholesale
 16oz PET can for Cold Brew Coffee
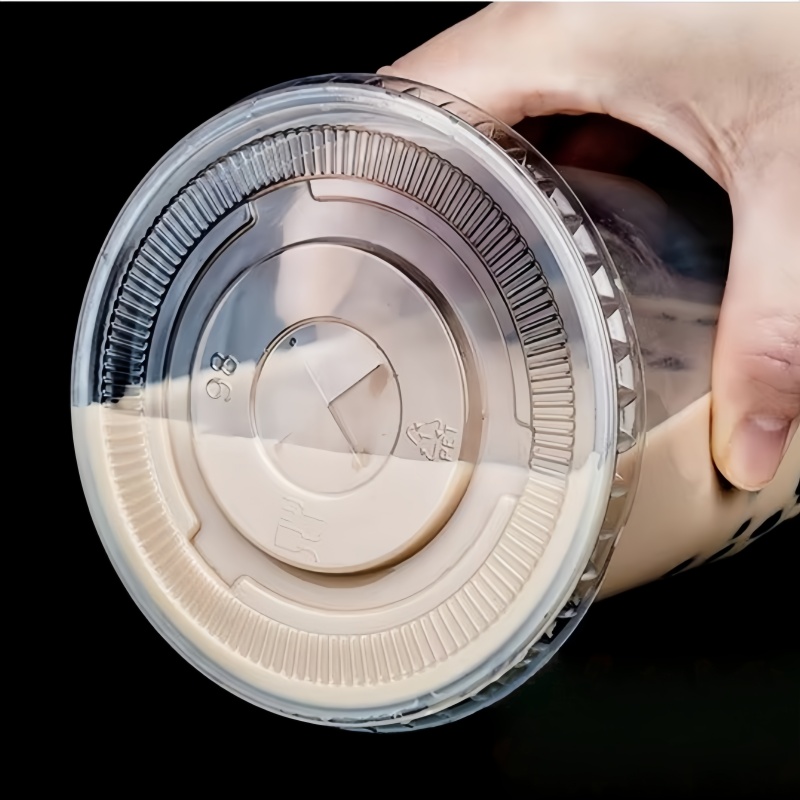 PET Flat Lid
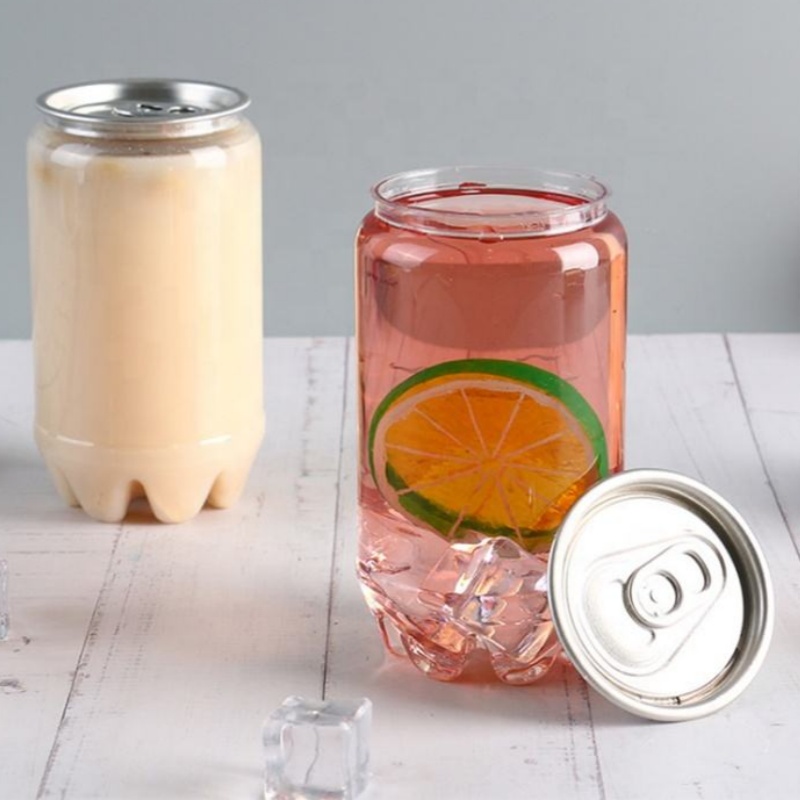 Factory Direct Price Pet Cans For Wholesale
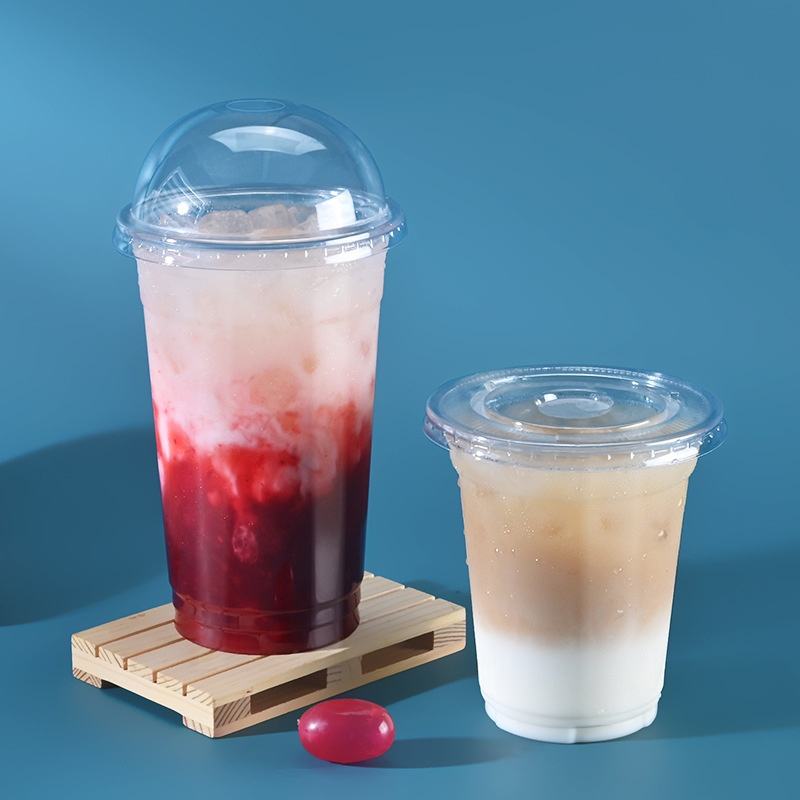 98mm PET Plastic Cups Wholesale
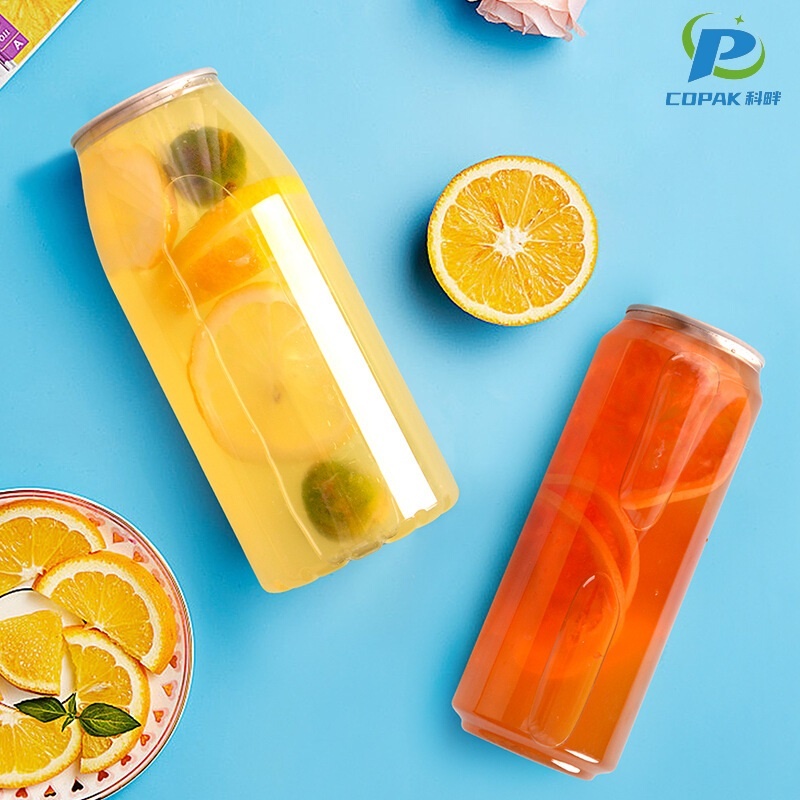 Custom PET Cans with aluminum lids