Leave Your Message
Premium recyclable PET cans and accessories designed specifically for artisanal cold brew coffee packaging
The artisanal cold brew coffee market has experienced exponential growth over the past decade, evolving from a niche specialty product to a mainstream beverage category. As consumer demand continues to surge, the packaging industry has responded with innovative solutions that balance functionality, sustainability, and brand appeal. Among these innovations, recyclable PET (polyethylene terephthalate) cans have emerged as a game-changing packaging format for cold brew coffee producers.
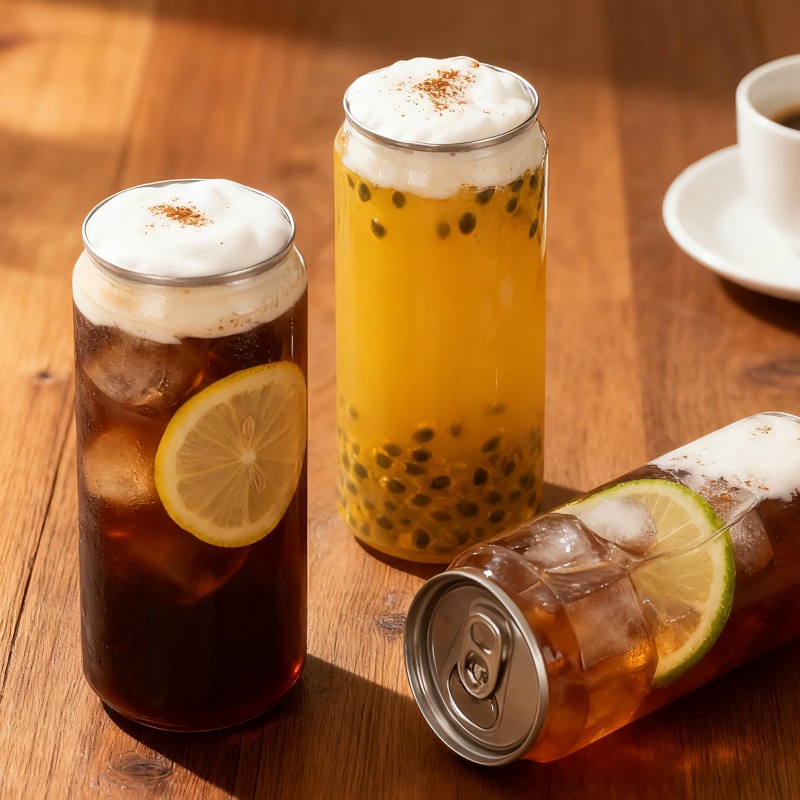
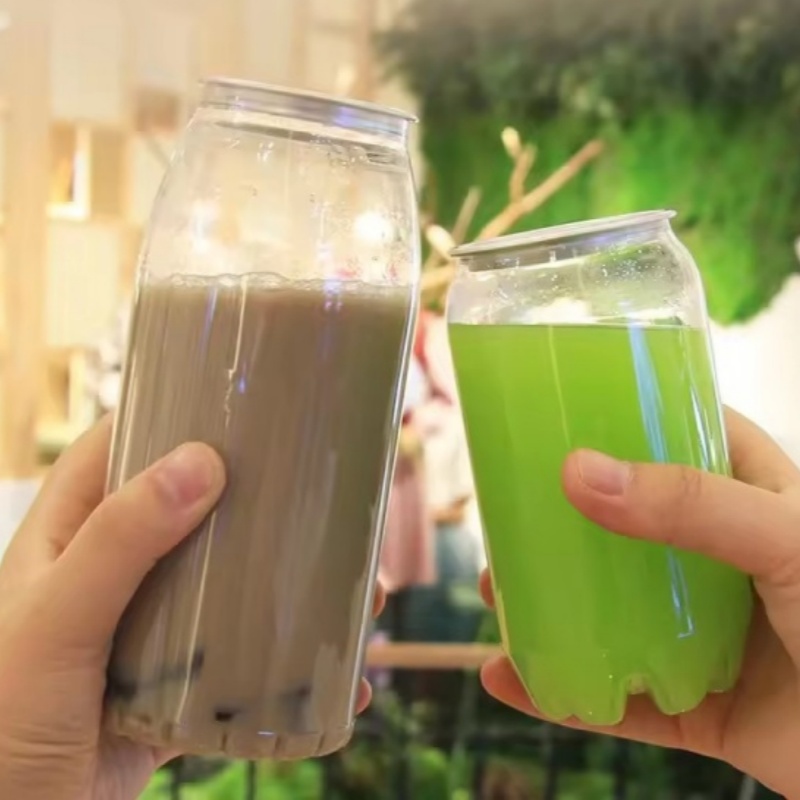
Recyclable PET cans represent a significant advancement in sustainable beverage packaging, offering coffee roasters and beverage brands an environmentally responsible alternative to traditional aluminum cans and single-use plastics. These transparent or semi-transparent containers not only showcase the rich, dark color of cold brew coffee but also communicate a brand's commitment to environmental stewardship—a value increasingly important to today's conscious consumers.
The global cold brew coffee market has witnessed remarkable expansion, with industry analysts projecting continued growth at a compound annual growth rate (CAGR) of over 20% through 2028. This explosive growth is driven by several factors: the beverage's smooth, less acidic flavor profile, higher caffeine content, convenience for on-the-go consumption, and the premiumization trend in the coffee industry.
As the cold brew segment expands, packaging requirements have become increasingly sophisticated. Artisanal coffee producers need containers that preserve freshness, maintain flavor integrity, provide extended shelf life, and align with sustainability values—all while standing out on crowded retail shelves. Recyclable PET cans address each of these requirements comprehensively.
According to recent consumer research, over 73% of coffee drinkers consider environmental impact when making purchasing decisions. This sustainability consciousness has accelerated the adoption of recyclable packaging solutions across the beverage industry, with PET cans leading the charge in the ready-to-drink coffee segment.
Recyclable PET cans offer numerous technical advantages that make them ideally suited for cold brew coffee packaging:
Oxygen Barrier Properties: Advanced PET formulations provide excellent oxygen barrier characteristics, crucial for maintaining the delicate flavor compounds in cold brew coffee. This protection prevents oxidation and preserves the beverage's signature smooth taste throughout its shelf life.
Light Protection: While offering visual appeal through transparency, PET cans can be manufactured with UV-blocking additives or amber tinting to protect light-sensitive coffee compounds from degradation. This balance between visibility and protection is particularly valuable for premium artisanal brands.
Structural Integrity: Modern PET can manufacturing techniques produce containers with exceptional structural strength, capable of withstanding the pressures of cold chain distribution, retail handling, and consumer use without compromising product integrity.
Temperature Resistance: PET cans maintain their shape and barrier properties across the temperature ranges typical in cold brew distribution and storage, from refrigerated warehouses to retail coolers to consumer refrigerators.
The environmental advantages of recyclable PET cans extend throughout their lifecycle, from production through end-of-life recycling. PET is one of the most successfully recycled plastics globally, with established collection and reprocessing infrastructure in most developed markets. This mature recycling system enables true circular economy applications where post-consumer PET cans can be reprocessed into new food-grade packaging materials.
The carbon footprint of PET can production is significantly lower than aluminum alternatives when considering the complete lifecycle. PET manufacturing requires less energy input, generates fewer greenhouse gas emissions, and the lightweight nature of PET containers reduces transportation-related emissions throughout the distribution chain.
Furthermore, advances in bio-based PET production are creating pathways toward even greater sustainability. Plant-derived PET polymers maintain identical performance characteristics to petroleum-based materials while offering reduced fossil fuel dependency and lower overall environmental impact.
For artisanal cold brew coffee producers, packaging serves as a critical brand communication tool. Recyclable PET cans offer unparalleled design flexibility that enables brands to create distinctive, eye-catching packages that convey their unique identity and quality positioning.
The transparency of PET allows consumers to see the product itself—a powerful selling point for high-quality cold brew coffee with its rich, appealing color. This visibility builds trust and communicates authenticity, particularly important in the artisanal segment where product quality is paramount.
Advanced printing technologies enable full-color graphics, gradient effects, and intricate designs that capture brand personality and shelf appeal while maintaining the recyclability of the container.
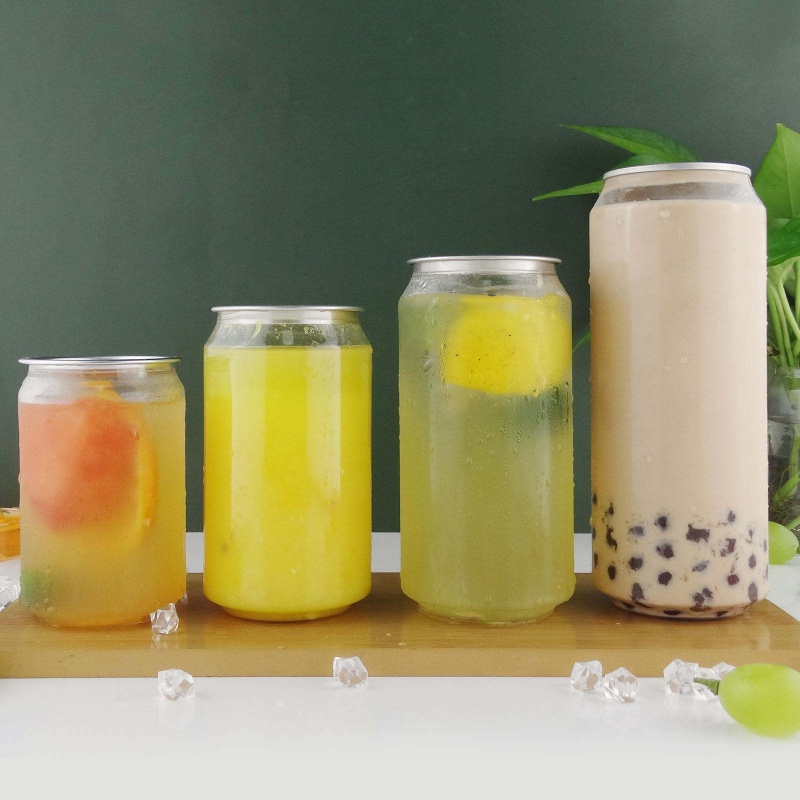
PET cans can be manufactured in various shapes and sizes—from sleek, tall formats to short, wide profiles—allowing brands to optimize for different consumption occasions and retail environments.
Whether using shrink sleeves, pressure-sensitive labels, or direct printing, PET cans accommodate diverse labeling approaches that support brand storytelling and regulatory compliance.
Specialty coatings, metallic effects, and matte or gloss finishes enable premium positioning and tactile differentiation that resonates with quality-focused consumers.
Recyclable PET cans have proven successful across diverse distribution channels and consumption occasions within the cold brew coffee market:
Retail Distribution: In grocery stores, convenience stores, and specialty food retailers, PET cans offer excellent shelf presence and product visibility. Their lightweight nature reduces transportation costs and enables efficient case packing, while their durability minimizes damage during handling and stocking.
Food Service Applications: Restaurants, cafes, and institutional food service operations increasingly offer packaged cold brew options for grab-and-go sales. PET cans provide the portion control, convenience, and premium presentation these channels require.
Direct-to-Consumer Channels: E-commerce and subscription services benefit from PET cans' lightweight properties and shipping durability. The containers withstand the rigors of direct shipping while minimizing freight costs and packaging material requirements.
Event and On-Premise Consumption: Festivals, conferences, sporting events, and other venues favor PET cans for their safety advantages over glass, recyclability, and ease of handling in high-volume serving environments.
The production of recyclable PET cans for cold brew coffee involves sophisticated manufacturing processes that ensure consistent quality, food safety, and performance. Modern blow molding technology creates containers with precise dimensional tolerances, uniform wall thickness, and excellent clarity.
Quality control throughout the manufacturing process addresses critical parameters including material purity, structural integrity, barrier performance, and compatibility with various sealing systems. Automated inspection systems identify and reject any containers that fail to meet stringent specifications.
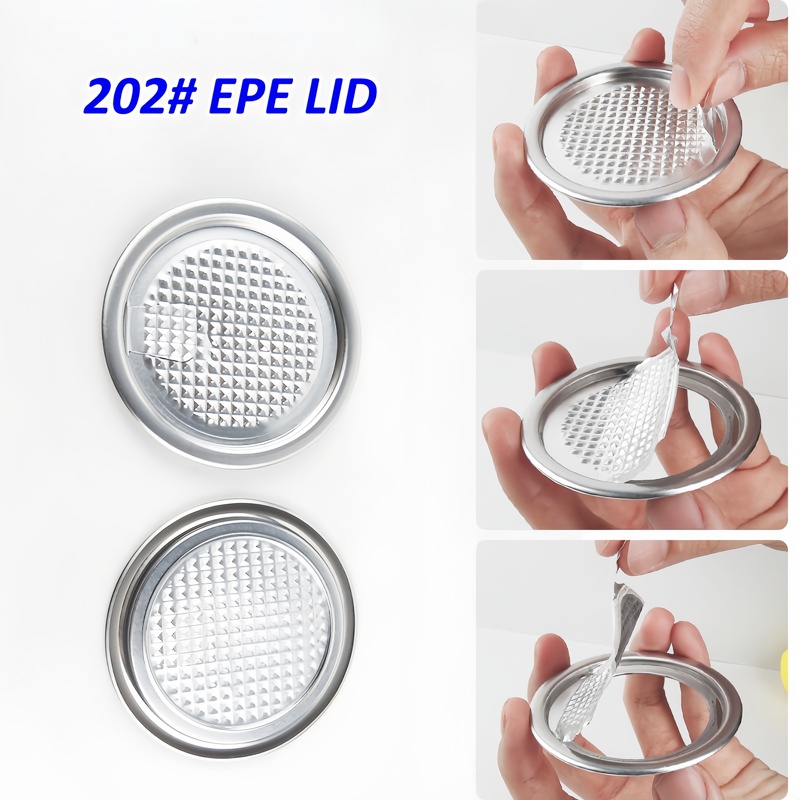
Sealing technology represents a crucial component of the complete packaging system. Easy-peel lids, such as the 202# EPE (Easy Peel End) systems, provide hermetic seals that preserve product freshness while offering consumer-friendly opening experiences. These sealing systems must maintain integrity throughout distribution and storage while enabling effortless opening when desired.
Recyclable PET cans for cold brew coffee must comply with comprehensive regulatory requirements governing food contact materials. In the United States, FDA regulations specify approved materials, additives, and manufacturing processes for food packaging. European markets require compliance with EU Regulation No. 10/2011 and related directives.
These regulatory frameworks ensure that PET containers do not impart unwanted flavors, odors, or substances to packaged beverages. Migration testing verifies that no harmful chemicals transfer from packaging to product under normal storage and use conditions. Reputable manufacturers maintain documentation demonstrating regulatory compliance and conduct ongoing testing to ensure continued adherence to evolving standards.
While sustainability and performance drive adoption of recyclable PET cans, economic factors also influence packaging decisions. PET cans offer favorable economics compared to alternative packaging formats when considering total cost of ownership.
The lightweight nature of PET reduces transportation costs throughout the supply chain—from raw material delivery to finished product distribution. Lower shipping weights translate directly to reduced freight expenses and carbon emissions, creating both economic and environmental benefits.
Manufacturing efficiency has improved dramatically as PET can production technology has matured. High-speed blow molding lines achieve impressive output rates with minimal waste generation. Automated quality control reduces labor requirements while ensuring consistent product quality.
For small and medium-sized artisanal coffee producers, contract packaging services and lower minimum order quantities make PET cans accessible without massive capital investments. This accessibility democratizes premium packaging, enabling craft producers to compete effectively with larger brands.
The future of recyclable PET cans in cold brew coffee packaging promises continued innovation across multiple dimensions. Material science advances are producing PET formulations with enhanced barrier properties, enabling even longer shelf life and expanded distribution possibilities.
Smart packaging integration represents an emerging frontier, with technologies like QR codes, NFC tags, and printed electronics enabling enhanced consumer engagement, supply chain transparency, and anti-counterfeiting measures. These digital enhancements transform packaging from passive containers into interactive brand experiences.
Lightweighting initiatives continue to reduce material usage without compromising performance. Each gram eliminated from container weight multiplies across millions of units, generating substantial resource conservation and cost savings.
The development of chemical recycling technologies promises to complement mechanical recycling, creating additional pathways for post-consumer PET to return to food-grade applications. These advanced recycling methods can process mixed or contaminated PET streams that mechanical recycling cannot handle, further strengthening circular economy systems.
Emerging multilayer PET structures and nano-coating technologies are achieving oxygen transmission rates comparable to glass and aluminum, potentially extending cold brew shelf life beyond 120 days while maintaining full recyclability through compatible material selection and layer design.
Artisanal cold brew coffee producers considering recyclable PET cans should evaluate several key factors to optimize packaging selection and implementation:
Supplier Selection: Partner with experienced PET can manufacturers who understand beverage packaging requirements and maintain appropriate quality certifications. Evaluate production capabilities, minimum order quantities, customization options, and technical support services.
Package Design: Invest in professional package design that balances aesthetic appeal with functional requirements. Consider how graphics, colors, and structural elements communicate brand values and product attributes while ensuring regulatory compliance.
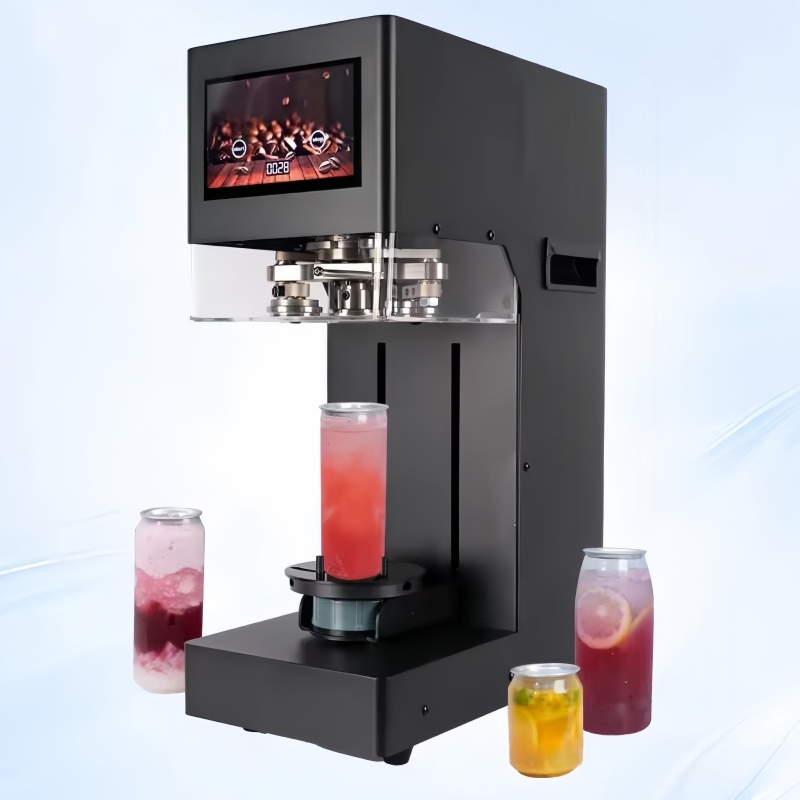
Fill and Seal Operations: Implement appropriate filling equipment and sealing systems that maintain product quality and package integrity. Whether using contract packaging services or in-house operations, ensure proper training, maintenance, and quality control procedures.
Supply Chain Management: Develop efficient inventory management and logistics strategies that account for PET cans' characteristics. Optimize storage conditions, handling procedures, and transportation methods to prevent damage and maintain quality.
Consumer Communication: Clearly communicate the recyclability and sustainability benefits of PET packaging through on-pack messaging and marketing materials. Educate consumers about proper recycling procedures to maximize environmental benefits.
Recyclable PET cans represent a mature, proven packaging solution that addresses the complex requirements of artisanal cold brew coffee producers. Their combination of sustainability, performance, design flexibility, and economic efficiency positions them as an ideal choice for brands seeking to balance environmental responsibility with business success.
As consumer demand for sustainable packaging continues to intensify and regulatory pressures encourage circular economy approaches, recyclable PET cans are poised to capture increasing market share in the cold brew coffee segment. Producers who embrace this packaging format position themselves advantageously for long-term growth while contributing to meaningful environmental progress.
The continued evolution of PET can technology promises even greater benefits in the years ahead, with innovations in materials, manufacturing, and recycling creating ever more sustainable and effective packaging solutions. For artisanal cold brew coffee brands, recyclable PET cans offer a pathway to packaging excellence that serves both business objectives and planetary wellbeing.

Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
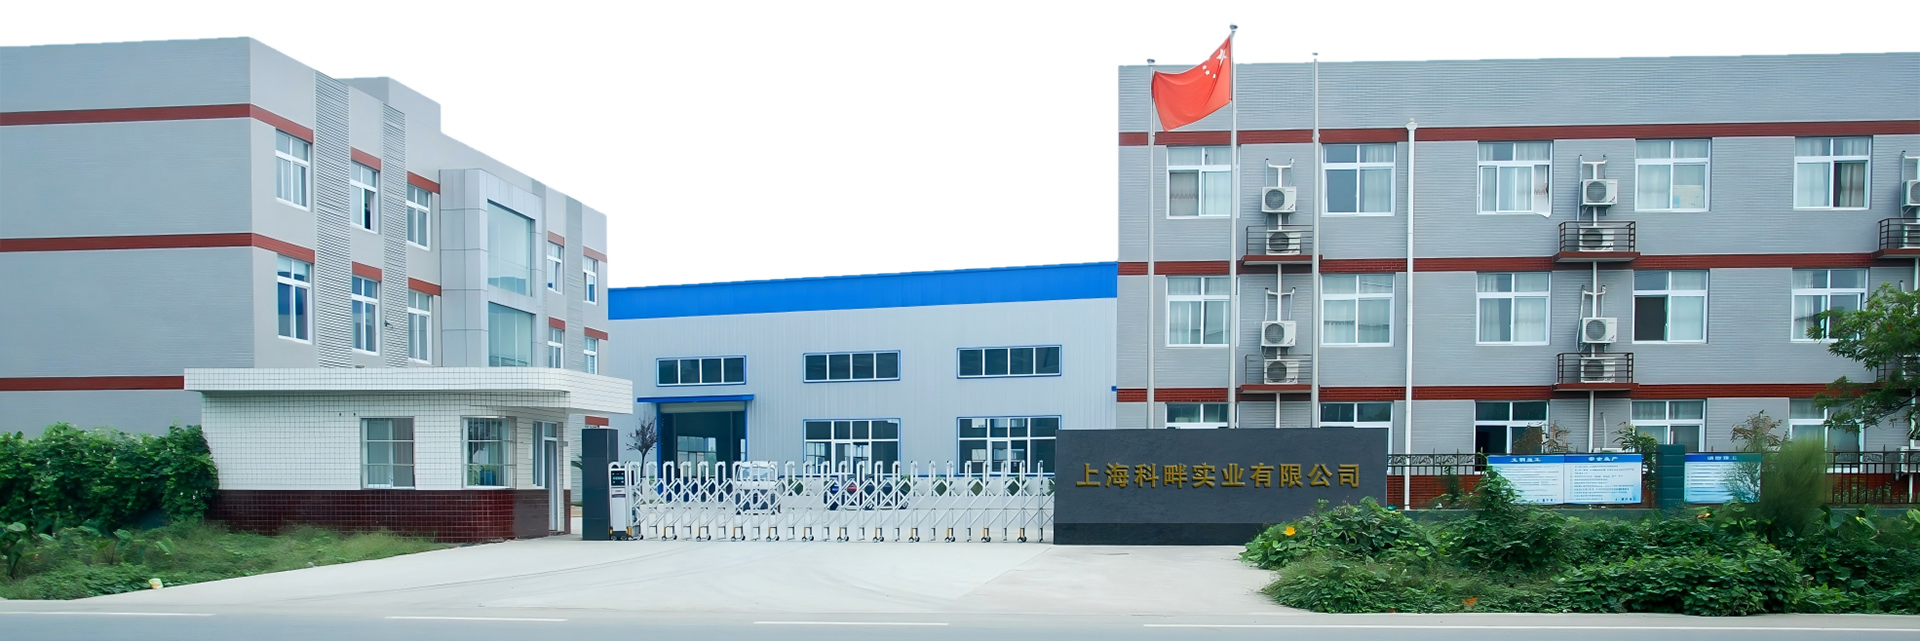
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
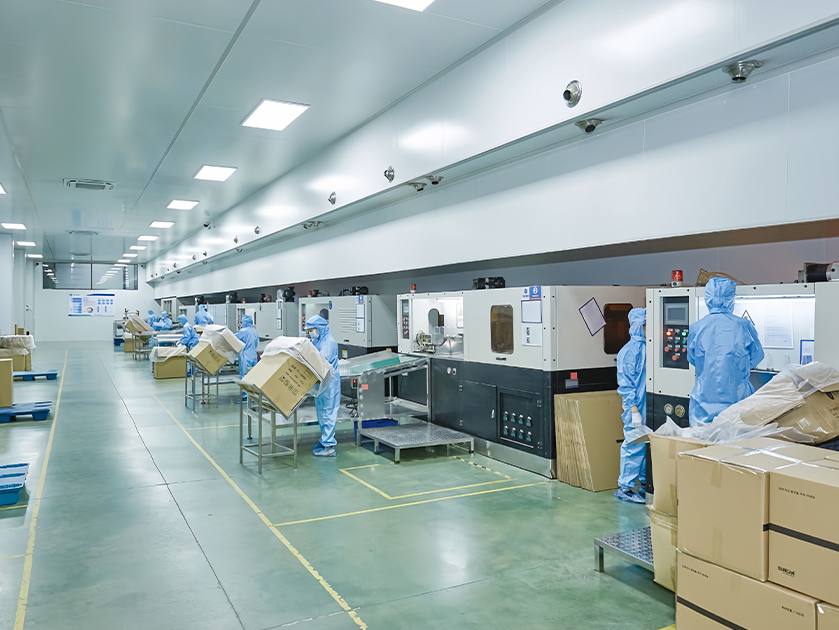
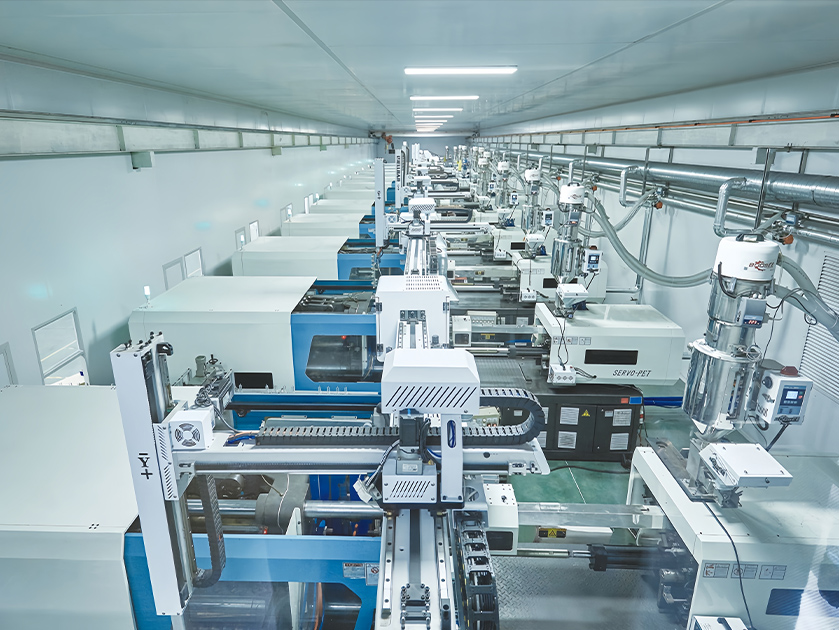
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
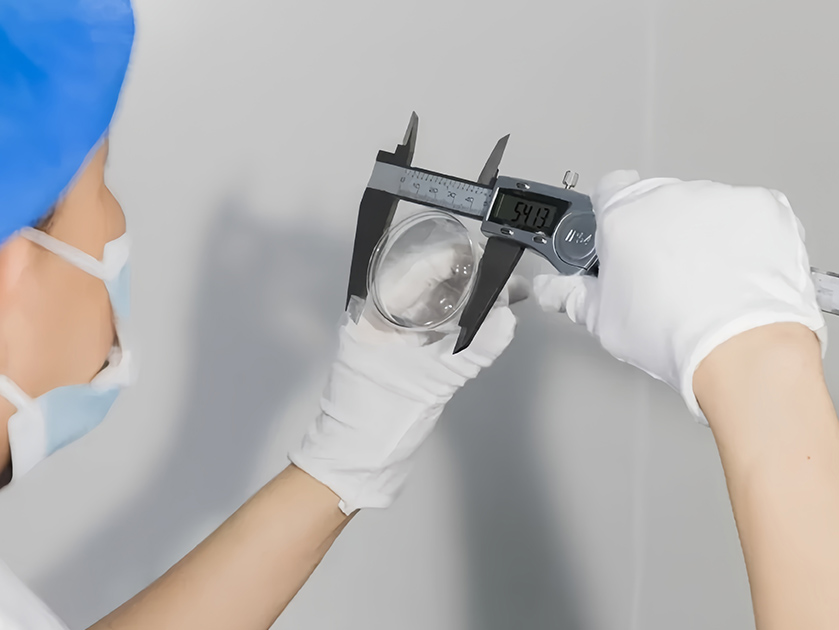
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsAdhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
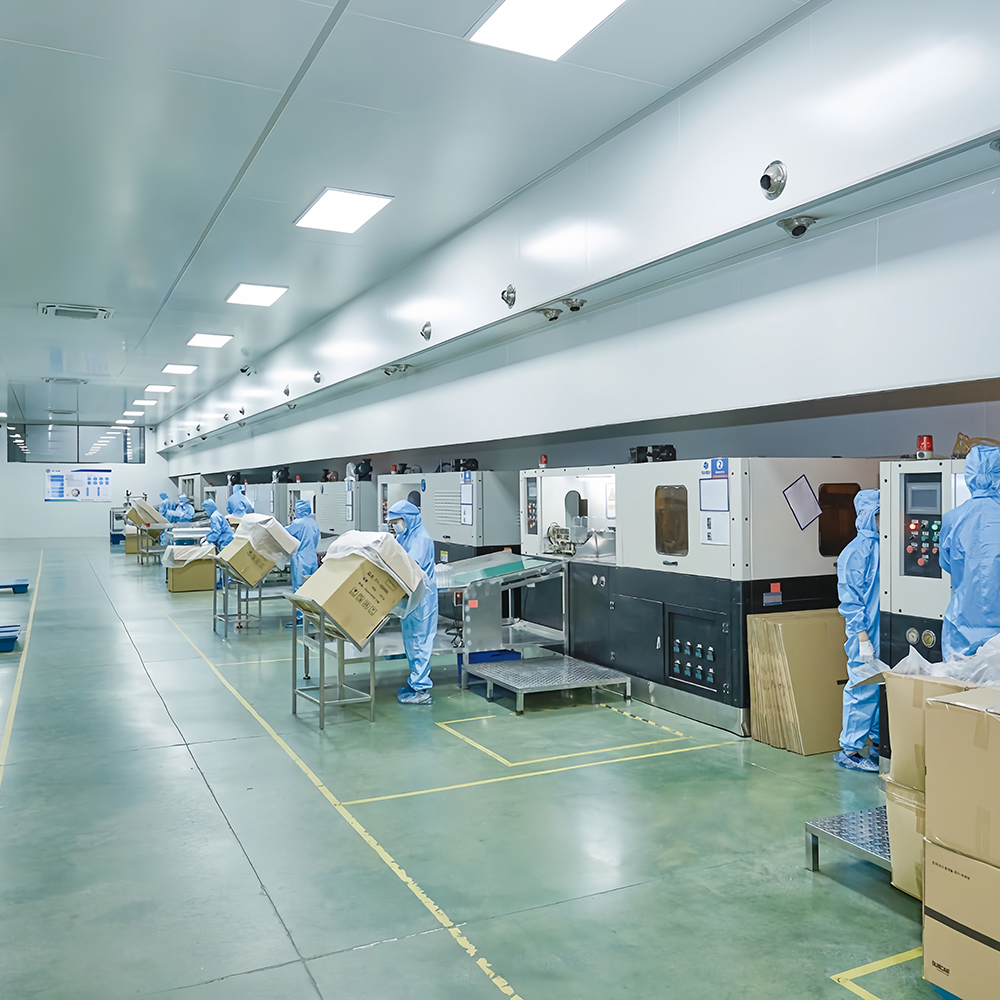
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
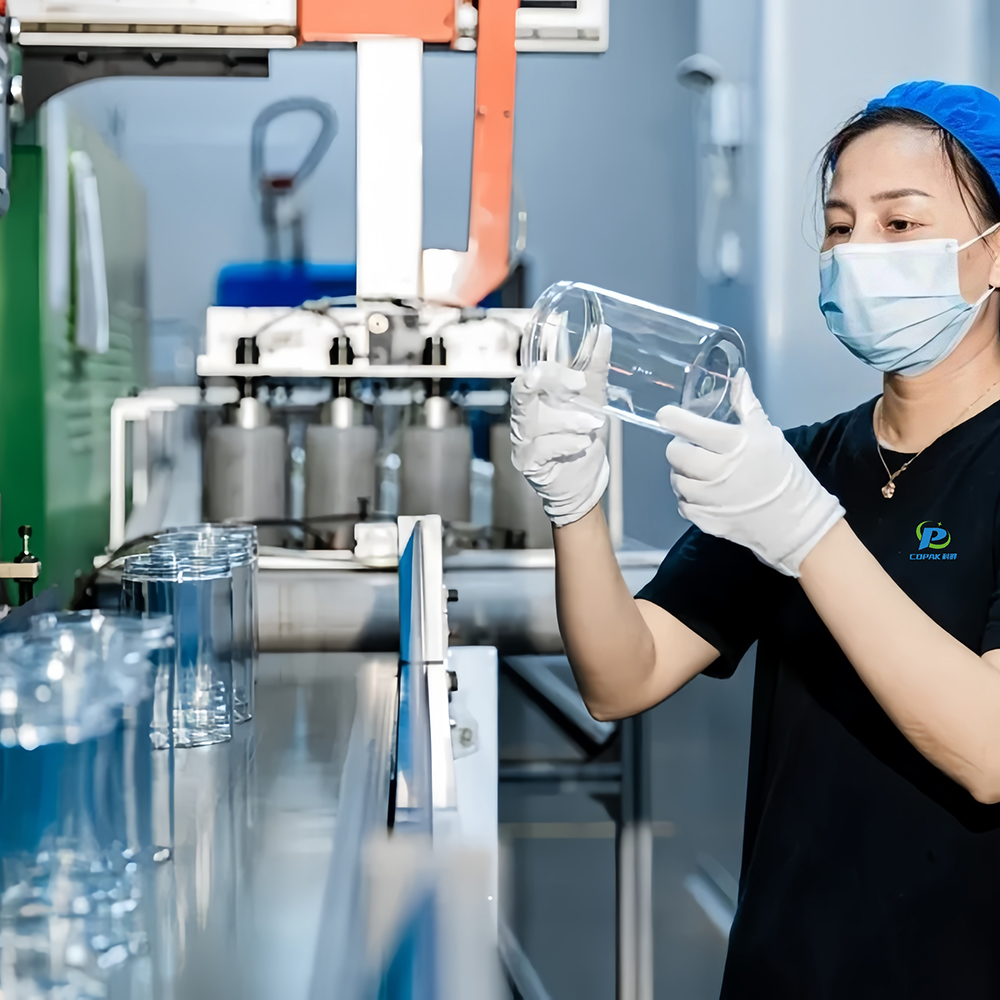
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Explore our comprehensive selection of PET packaging solutions for cold brew coffee and beverages
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.