Leave Your Message
Explore our state-of-the-art transparent packaging designed specifically to maintain carbonation and freshness for sparkling mineral water brands.
The global beverage market is experiencing a profound paradigm shift. As health-conscious consumers transition away from sugary sodas, the demand for clean, crisp, and refreshing sparkling mineral water has surged. Historically, carbonated beverages were packaged exclusively in aluminum cans or glass bottles. However, the modern beverage landscape demands innovation. Enter the PET Can for Sparkling Mineral Water—a hybrid packaging solution that combines the crystal-clear product visibility of glass with the lightweight, shatterproof, and cost-effective advantages of aluminum cans.
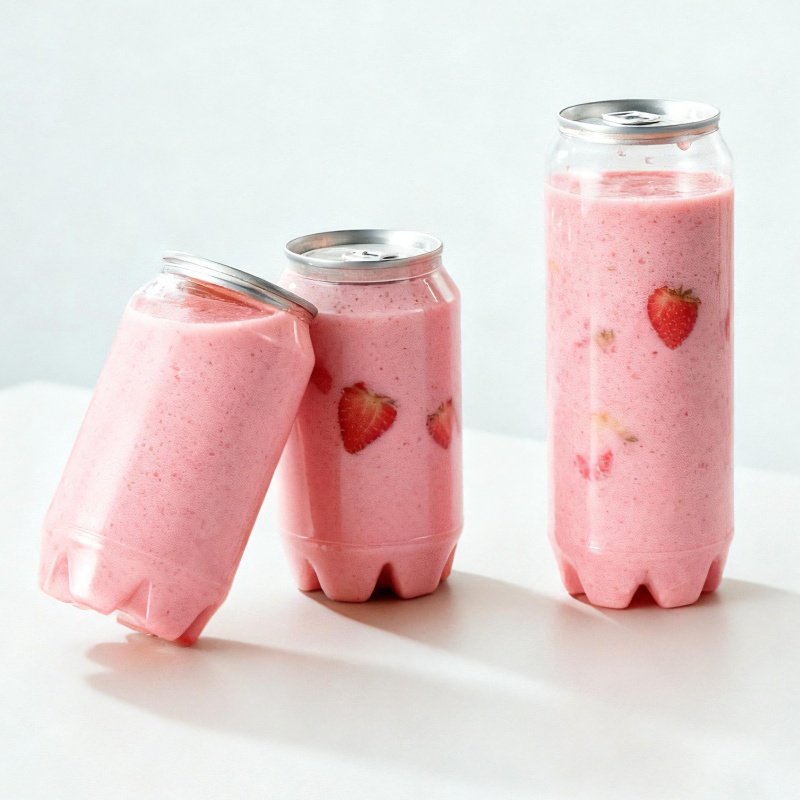
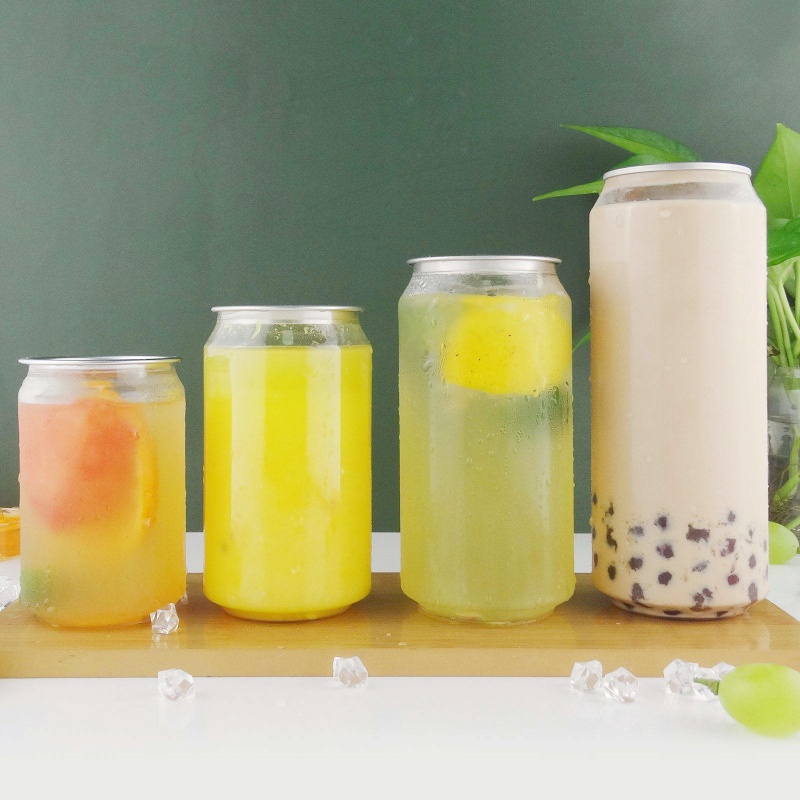
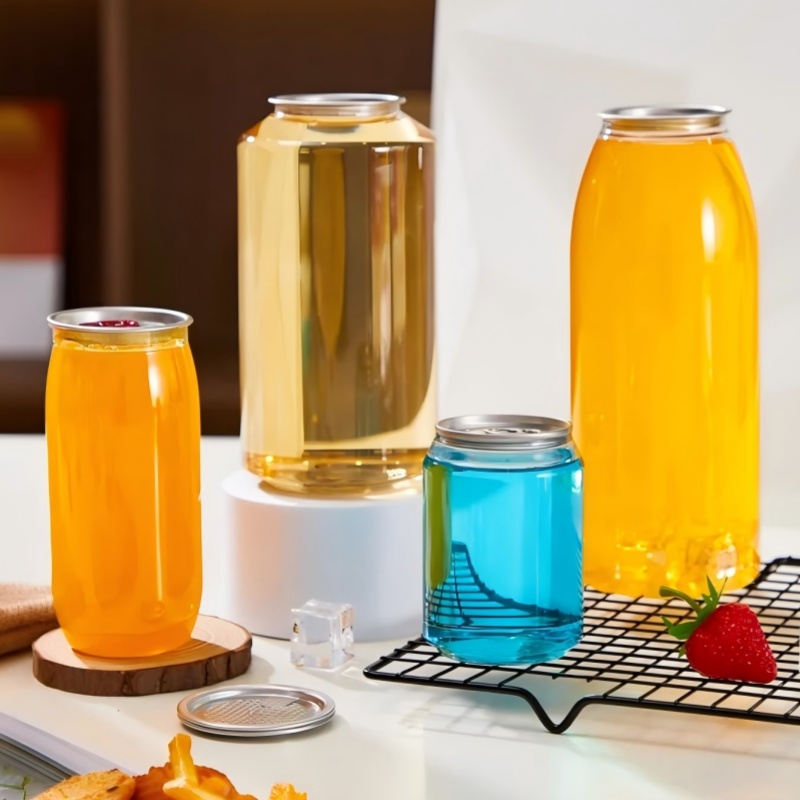
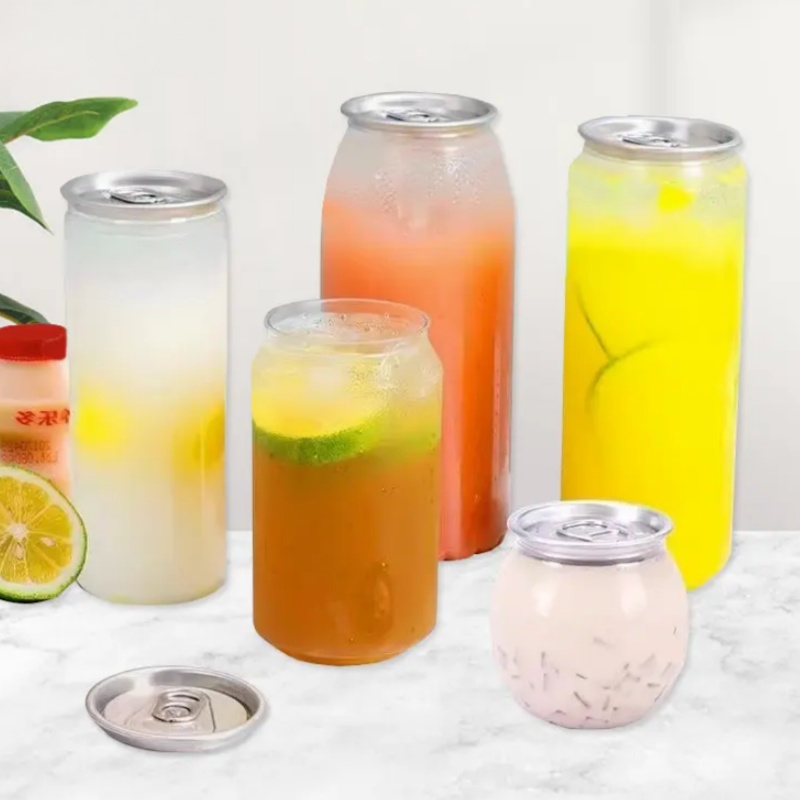
Today's consumers want to see what they are drinking. The transparency of polyethylene terephthalate (PET) allows the natural purity and effervescence of sparkling mineral water to shine through. The visual appeal of rising bubbles behind a pristine, clear plastic wall acts as a powerful point-of-sale marketing tool. This aesthetic advantage, paired with the tactile satisfaction of an aluminum easy-open end (SOT lid), makes the PET can the ultimate modern vessel for carbonated mineral waters, functional seltzers, and infused sparkling beverages.
From an industrial perspective, PET cans have transitioned from a niche packaging alternative to a mainstream commercial powerhouse. Beverage brands globally are adopting clear PET cans to differentiate themselves on crowded retail shelves. The commercial appeal is driven by several key factors:
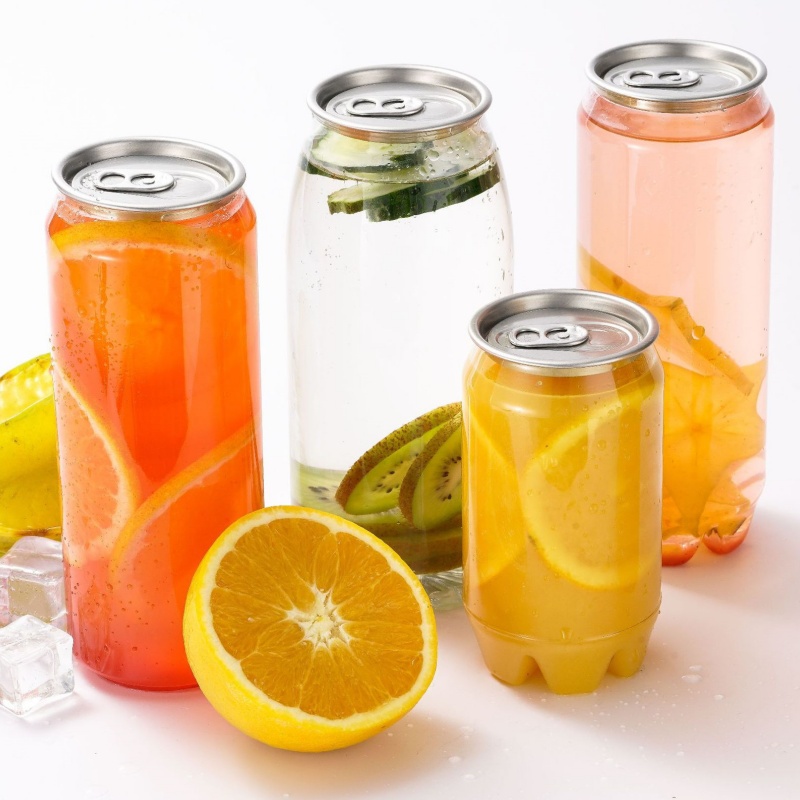
Furthermore, the rise of Ready-to-Drink (RTD) carbonated waters infused with vitamins, botanicals, and natural fruit flavors has created a high-value category where product presentation is critical. The PET can allows brands to showcase vibrant product colors and natural ingredients, reinforcing the healthy, clean-label identity of the beverage.
Packaging sparkling mineral water in plastic presents unique engineering challenges. Unlike still beverages, carbonated water exerts continuous internal pressure (typically between 2.5 to 4.0 volumes of CO2). To prevent the packaging from expanding, deforming, or losing carbonation over time, advanced material science must be deployed.
High-quality PET cans are manufactured using precision injection stretch blow molding (ISBM). This process aligns the polymer chains both axially and radially, dramatically increasing the tensile strength of the plastic. The base of the PET can is typically designed with a petaloid or reinforced structure to absorb internal pressure without bulging, ensuring the can remains perfectly stable on retail shelves and in cup holders.
Carbon dioxide loss (flatness) and oxygen ingress (oxidation) are the primary enemies of sparkling water quality. Leading manufacturers utilize multi-layer PET structures or specialize barrier additives (such as nylon blends or oxygen scavengers) within the PET matrix. These technologies significantly reduce gas permeability, ensuring that the sparkling water retains its crisp carbonation and fresh taste throughout its designated shelf life.
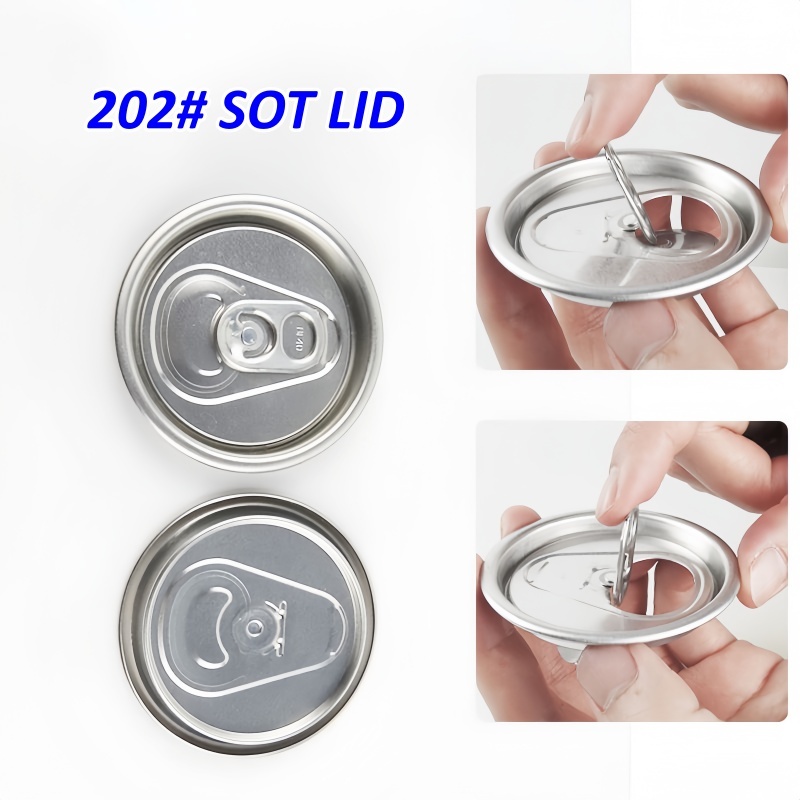
The combination of a PET body with a metal lid (typically a 202# Stay-On-Tab aluminum lid) requires a highly precise seaming process. The top neck of the PET can is structurally reinforced to withstand the mechanical forces of double-seaming machines. When sealed correctly, this hybrid interface provides a 100% airtight, leak-proof barrier that rivals conventional all-aluminum cans.
As the beverage packaging industry faces intense environmental scrutiny, the future of the PET can for sparkling mineral water is intrinsically linked to sustainable innovation. The industry is rapidly moving toward a circular economy model, marked by the following trends:
Integration of rPET (Recycled PET): Leading manufacturers are incorporating high percentages of post-consumer recycled PET (rPET) into their can preforms. Utilizing rPET reduces carbon emissions, minimizes landfill waste, and aligns with the strict sustainability targets set by global governments and environmentally conscious consumers.
Lightweighting Designs: Through advanced computer-aided engineering (CAE) and finite element analysis (FEA), designers are reducing the amount of plastic resin required per can without compromising structural integrity. Lightweighting reduces transport emissions, lowers material costs, and improves the overall ecological footprint of the product.
Design for Circularity: Modern PET cans are engineered to be fully recyclable. The aluminum lid and PET body are easily separated during standard recycling sorting processes. Once processed, the PET can be recycled back into food-grade packaging, closing the loop on plastic waste.
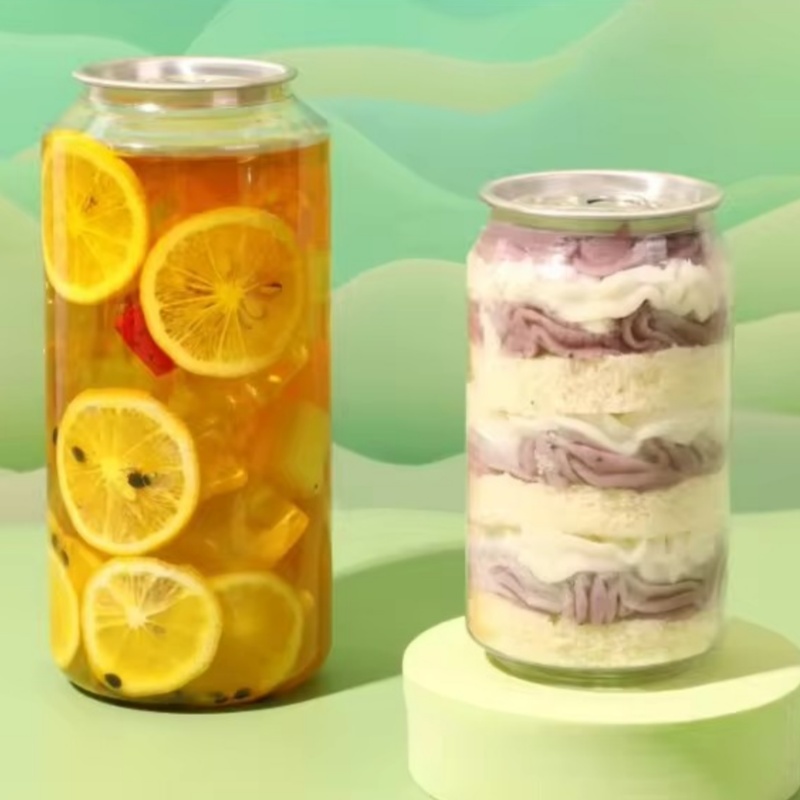
The versatility of the PET can makes it suitable for a wide range of specialized market applications. Here are some of the most prominent scenarios where transparent carbonated packaging excels:
Luxury hospitality venues place a premium on aesthetics. Serving sparkling mineral water in a sleek, transparent PET can matches the clean, minimalist vibe of high-end wellness centers. Guests can appreciate the visual purity of the water, enhancing their sensory experience while maintaining safety around wet pool areas where glass is banned.
Whether hiking, camping, or attending an outdoor concert, active consumers require durable, lightweight packaging. The PET can offers the convenience of a can but with the visual appeal of a premium bottled beverage. It fits perfectly into backpack side pockets and bicycle cages, resisting impact and keeping the carbonation locked in until opened.
In premium grocery stores and trendy urban cafes, shelf appeal is everything. Clear PET cans containing sparkling water infused with colorful natural fruit juices stand out dramatically under retail lighting. This visual transparency directly influences impulse buying behavior, as consumers perceive transparent packaging as more honest and natural.
SHANGHAI COPAK INDUSTRY CO., LTD.
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
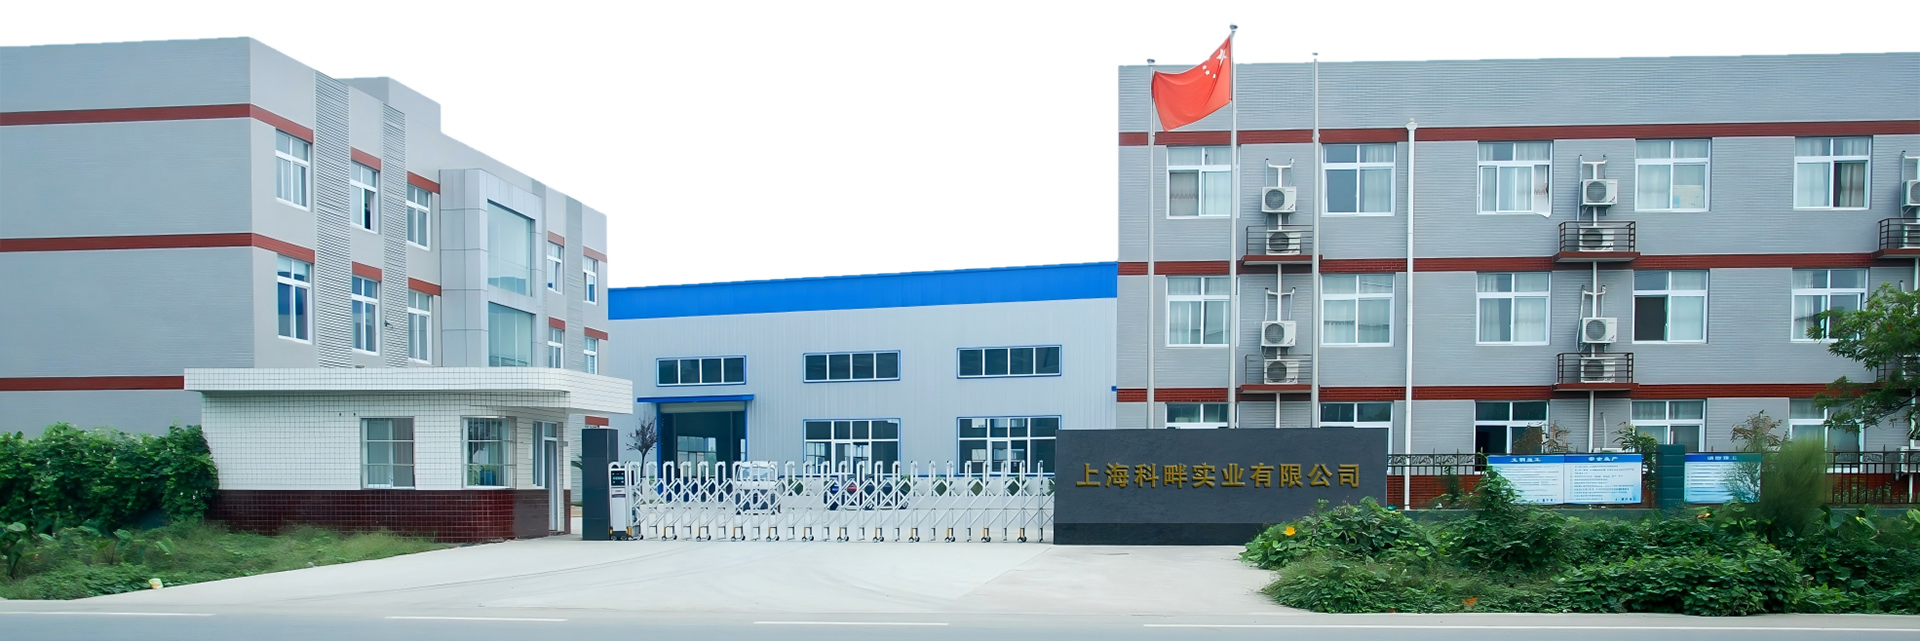
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production.
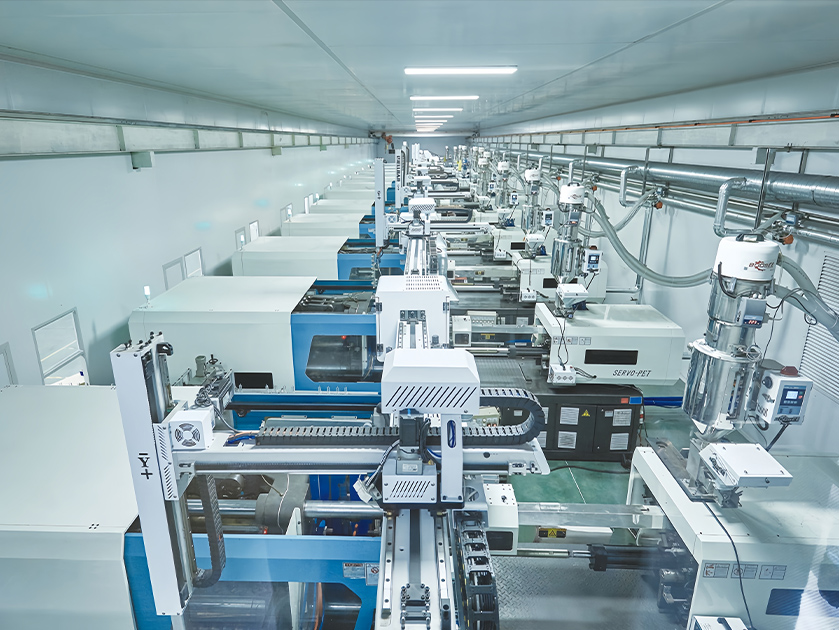
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
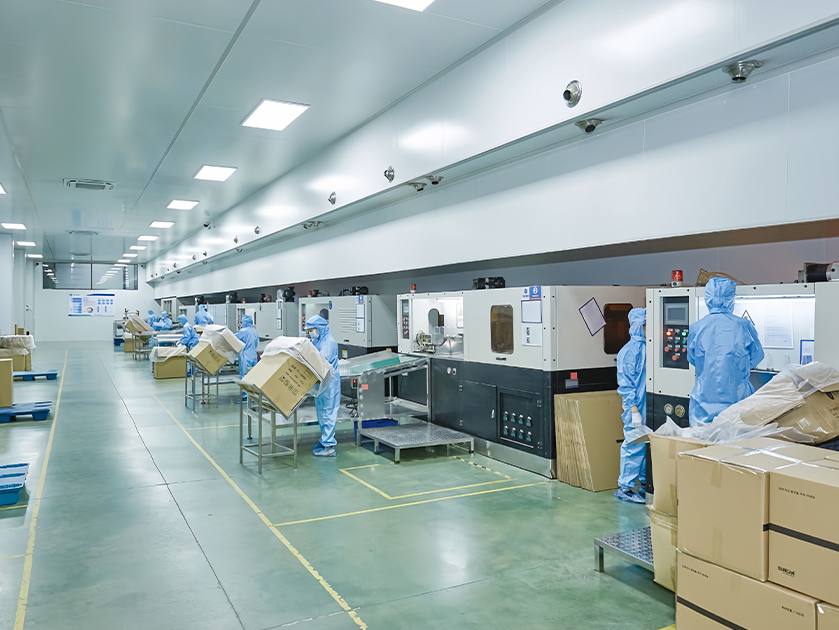
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
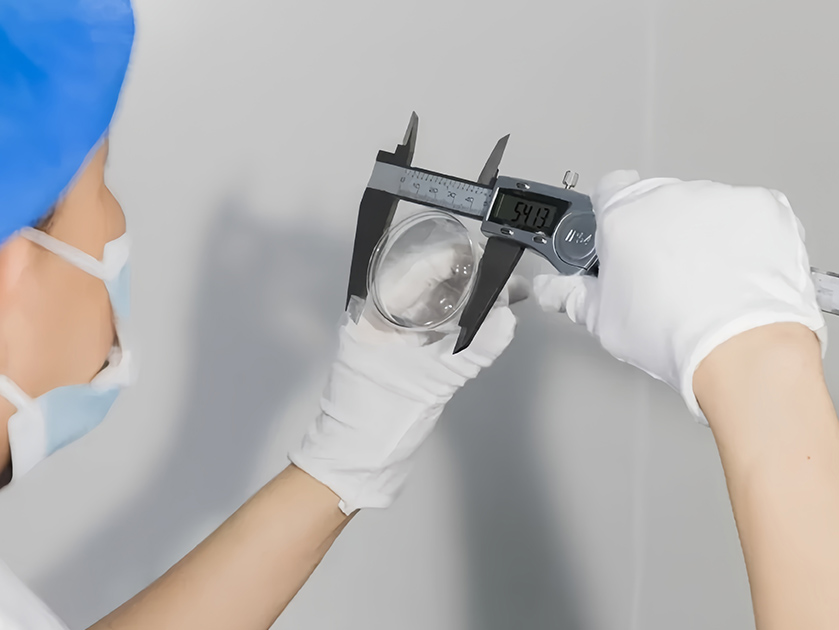
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsWe offer extensive customization options to meet the unique requirements of beverage brands and clients, including tailored shapes, sizes, and capacities for PET cups and cans. Additionally, we provide full support for custom mold development and personalized printing solutions.
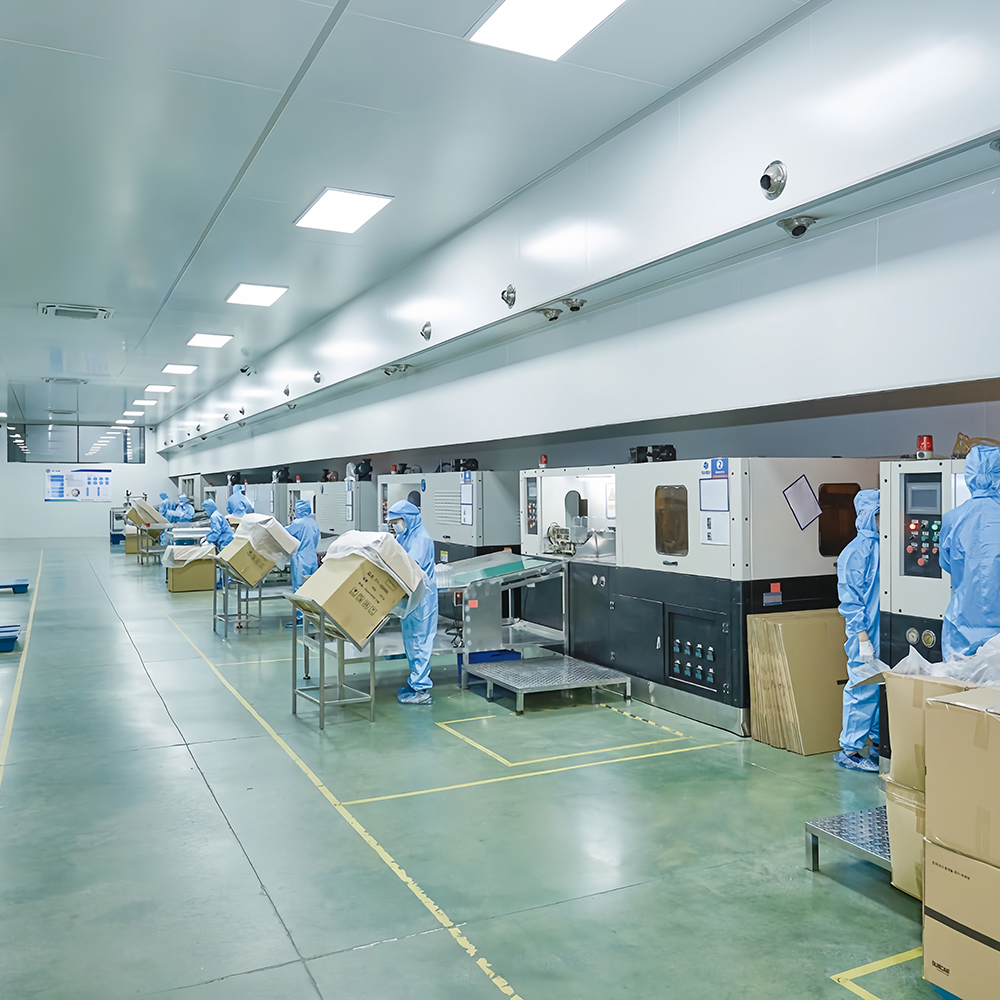
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.

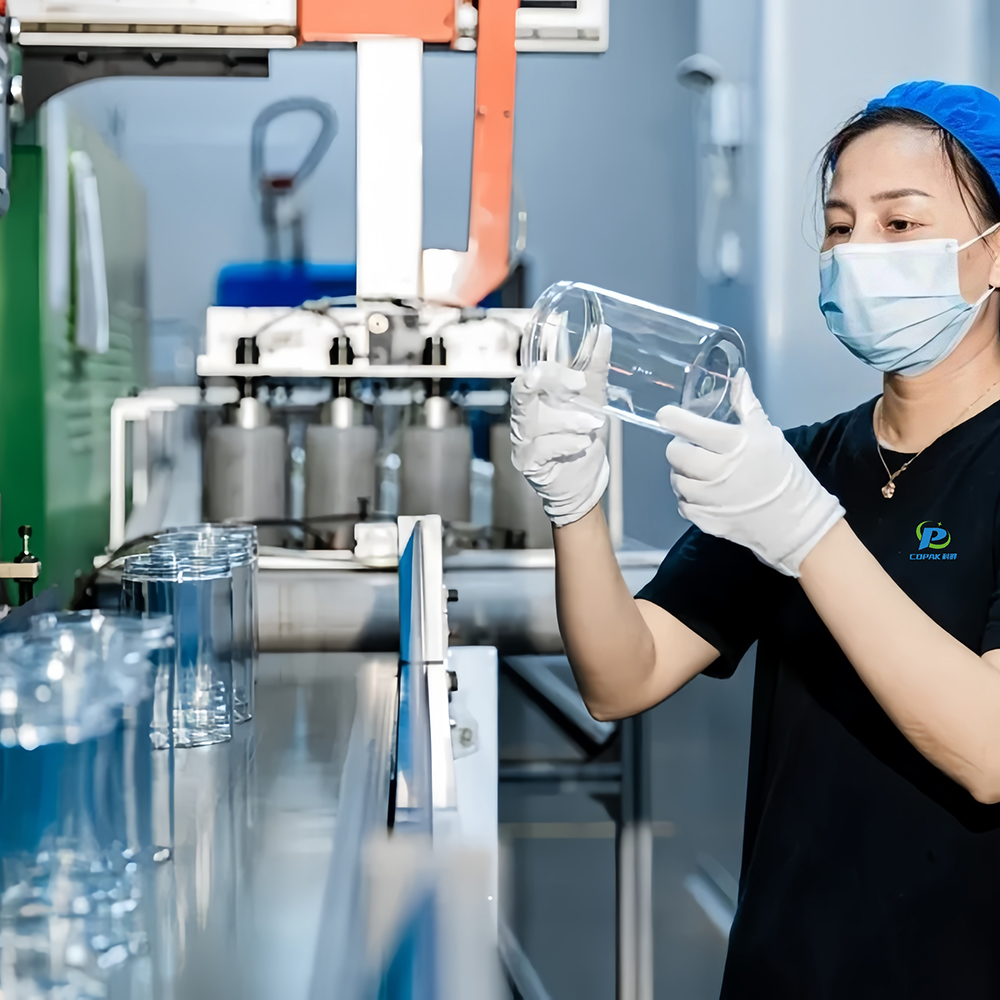
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
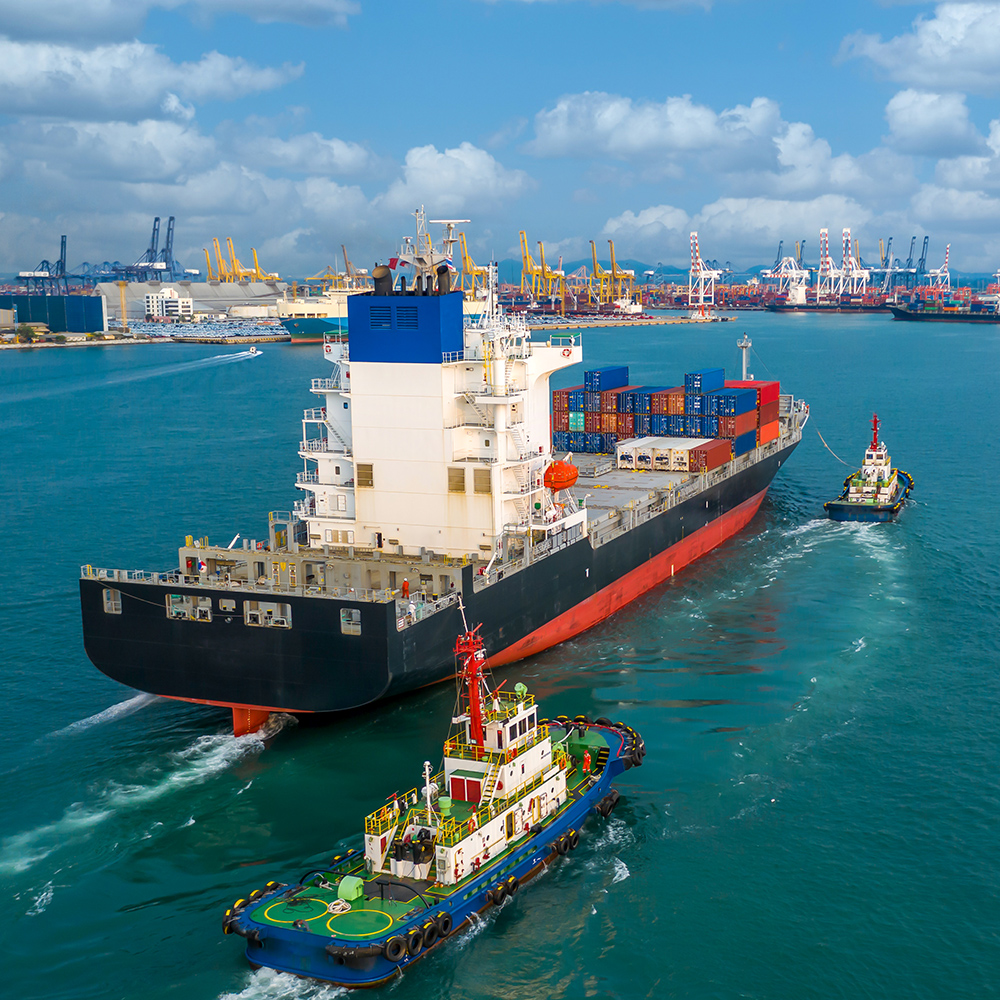
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
Discover the strategic and operational advantages of partnering with Shanghai COPAK for your beverage packaging needs.


Explore our full line of PET cans, aluminum lids, and cups tailored for sparkling mineral water and other beverage applications.
Having supplied PET cups and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
INQUIRY NOW