Leave Your Message
Exploring the transformation of coffee packaging and the pivotal role of PET cans in shaping modern beverage culture
The artisanal cold brew coffee market has experienced exponential growth over the past decade, evolving from a niche specialty product to a mainstream beverage category. This transformation has been accompanied by significant innovations in packaging technology, with PET beverage cans emerging as the preferred choice for premium cold brew coffee brands worldwide. The convergence of consumer preferences, sustainability demands, and technological advancements has positioned PET cans as the ideal packaging solution for this dynamic market segment.
Cold brew coffee, characterized by its smooth, low-acid profile and extended brewing process, requires packaging that preserves its unique flavor characteristics while providing convenience and visual appeal. Traditional aluminum cans, while functional, present limitations in terms of transparency, customization, and environmental impact. PET beverage cans address these challenges by offering superior clarity, lightweight construction, and enhanced recyclability—attributes that resonate strongly with the environmentally conscious, quality-focused demographic that drives artisanal coffee consumption.
The global cold brew coffee market is projected to reach $1.63 billion by 2025, with a compound annual growth rate (CAGR) of 25.1%. PET packaging accounts for approximately 35% of this market, with projections indicating continued expansion as brands seek differentiation through innovative packaging solutions.
Market CAGR
PET Packaging Share
Market Value 2025
Consumer Preference
The commercial landscape for PET beverage cans in the artisanal cold brew coffee sector is characterized by intense competition, rapid innovation, and evolving consumer expectations. Leading coffee brands such as Stumptown, La Colombe, and Blue Bottle have pioneered the use of PET cans, demonstrating their effectiveness in preserving coffee quality while enhancing brand visibility through transparent packaging that showcases the beverage's rich color and clarity.
Manufacturing capabilities have advanced significantly, with specialized production facilities now capable of producing PET cans with wall thickness precision of ±0.05mm, ensuring consistent quality and structural integrity. Modern blow molding technology enables production speeds exceeding 40,000 units per hour, meeting the high-volume demands of major coffee retailers and distribution networks.
PET cans enable brands to command 15-25% price premiums compared to traditional packaging, driven by perceived quality and sustainability attributes.
Cold brew coffee in PET cans has achieved placement in over 75,000 retail locations across North America, with continued expansion into convenience stores and specialty outlets.
Advanced manufacturing processes have reduced production costs by 30% over five years while improving quality consistency and customization capabilities.
The industrial ecosystem supporting PET beverage cans for cold brew coffee encompasses raw material suppliers, preform manufacturers, blow molding facilities, printing companies, and filling operations. This integrated supply chain ensures consistent quality, rapid turnaround times, and scalability to meet fluctuating market demands.
Preform production represents a critical stage, with manufacturers utilizing injection molding technology to create PET preforms with precise specifications. These preforms are subsequently heated and blown into final can shapes using stretch blow molding equipment, achieving optimal material distribution and structural integrity. Advanced quality control systems monitor wall thickness, dimensional accuracy, and visual defects throughout the production process, ensuring compliance with stringent food-grade packaging standards.
Environmental sustainability represents the most significant driver of innovation in PET beverage can development. The industry is witnessing accelerated adoption of recycled PET (rPET) content, with leading manufacturers now producing cans containing 50-100% post-consumer recycled material without compromising structural integrity or visual clarity. This transition addresses consumer concerns regarding plastic waste while reducing carbon footprint by up to 60% compared to virgin PET production.
Emerging bio-based PET alternatives, derived from renewable resources such as sugarcane, offer further environmental benefits. These materials maintain identical performance characteristics to conventional PET while reducing dependence on fossil fuels. Several major coffee brands have committed to transitioning to 100% bio-based or recycled PET packaging by 2025, driving industry-wide adoption of sustainable materials.
The integration of smart packaging technologies represents a frontier innovation area. QR codes, NFC tags, and augmented reality features embedded in PET can labels enable brands to provide consumers with detailed product information, brewing stories, and interactive experiences. These technologies also facilitate supply chain tracking, authentication verification, and consumer engagement analytics.
Temperature-sensitive inks and freshness indicators are being incorporated into PET can designs, providing visual cues regarding optimal consumption timing and storage conditions. These innovations enhance consumer confidence while reducing product waste through improved inventory management and consumption guidance.
Oxygen barrier properties remain critical for preserving cold brew coffee quality during extended shelf life periods. Advanced coating technologies, including plasma deposition and nano-layer applications, enhance PET's inherent barrier characteristics, extending product freshness from 90 to 180+ days without refrigeration requirements.
Multi-layer PET structures incorporating EVOH (ethylene vinyl alcohol) barriers provide superior oxygen and moisture protection, enabling distribution through ambient temperature channels while maintaining flavor integrity. These technological advances expand market opportunities and reduce cold chain logistics costs.
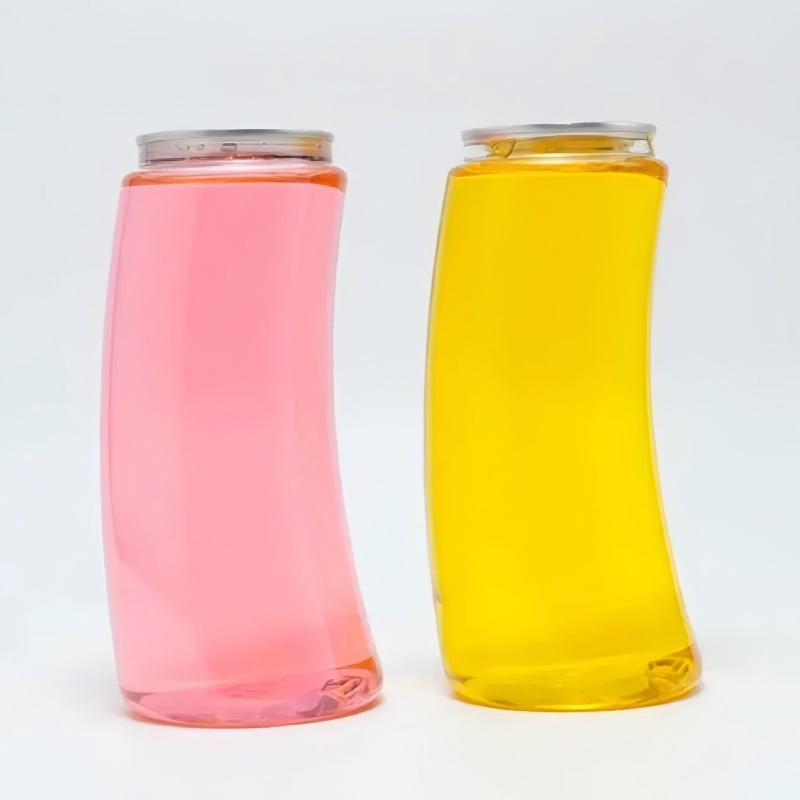
Aesthetic differentiation through innovative can designs has become a competitive imperative. Manufacturers now offer extensive customization options including embossed textures, metallic finishes, gradient colors, and complex geometric shapes. Digital printing technology enables short-run production of limited edition designs, supporting seasonal releases and regional market variations without significant tooling investments.
Ergonomic considerations are driving can shape innovations, with contoured profiles and grip-enhancing features improving handling and consumption experiences. Slim-line formats (sleek 250ml cans) appeal to health-conscious consumers seeking portion control, while larger formats (473ml and 500ml) target value-oriented segments and sharing occasions.
PET beverage cans have revolutionized cold brew coffee distribution across diverse retail environments. In premium grocery chains, transparent PET cans enable visual merchandising strategies that highlight product quality and differentiation. The lightweight nature of PET reduces transportation costs and carbon emissions, while shatter-resistance minimizes product loss during handling and display.
Convenience store applications benefit from PET's durability and space-efficient stacking characteristics. The ability to produce cans in various sizes accommodates different consumption occasions—single-serve formats for immediate consumption and multi-serve options for home storage. Enhanced graphics and brand visibility drive impulse purchases, with studies indicating 40% higher conversion rates for transparent PET packaging compared to opaque alternatives.
Restaurants, cafes, and catering operations increasingly utilize PET-canned cold brew for consistent quality and operational efficiency, eliminating on-site brewing requirements while maintaining premium positioning.
Lightweight PET construction reduces shipping costs by 25-35% compared to glass alternatives, while impact resistance minimizes damage rates in direct-to-consumer distribution channels.
Outdoor festivals, sporting venues, and hospitality environments benefit from PET's safety profile—no glass breakage risks—while maintaining premium presentation standards.
Transparent PET cans serve as powerful brand-building tools, enabling coffee roasters to showcase product authenticity and quality visually. The ability to observe coffee color, clarity, and crema layer creates emotional connections with consumers who value transparency—both literal and metaphorical—in their purchasing decisions.
Limited edition releases and seasonal variations leverage PET's customization capabilities to create collectible packaging that drives repeat purchases and social media engagement. Brands report 60-80% increases in user-generated content when utilizing distinctive PET can designs, amplifying marketing reach through organic consumer advocacy.
Research indicates that 73% of cold brew coffee consumers consider packaging sustainability when making purchase decisions, while 68% prefer transparent packaging that enables product visualization. PET cans uniquely address both preferences, positioning brands for competitive advantage in increasingly crowded markets.
Coffee roasters and beverage producers benefit from PET can compatibility with existing filling equipment, minimizing capital investment requirements for format transitions. Standard filling line modifications enable PET can processing at speeds comparable to aluminum cans, maintaining production efficiency while accessing new packaging benefits.
Shelf life optimization through nitrogen flushing and modified atmosphere packaging techniques extends product freshness, reducing waste and enabling broader geographic distribution. Cold brew coffee packaged in barrier-enhanced PET cans maintains flavor profiles for 120-180 days, compared to 60-90 days for standard packaging, significantly improving inventory management flexibility and reducing spoilage costs.
Food-grade PET used in beverage can manufacturing exhibits exceptional clarity (>90% light transmission), chemical resistance, and structural integrity across temperature ranges from -20°C to +60°C. The material's inherent properties include excellent moisture barrier characteristics (WVTR
Density optimization achieves wall thickness ranging from 0.25mm to 0.45mm depending on can size and application requirements, balancing material efficiency with structural performance. Burst pressure ratings exceed 150 PSI for standard configurations, accommodating carbonated cold brew formulations and ensuring safety during transportation and handling.
The production of PET beverage cans involves sophisticated multi-stage processes beginning with resin selection and preform injection molding. Precision temperature control during the stretch blow molding phase ensures uniform wall thickness distribution and optimal molecular orientation, enhancing mechanical properties and barrier performance.
Quality assurance protocols include automated visual inspection systems utilizing machine vision technology to detect surface defects, dimensional variations, and contamination at inspection speeds exceeding 60,000 units per hour. Statistical process control methodologies maintain production consistency with defect rates below 0.1%, ensuring reliable supply of premium-quality packaging.
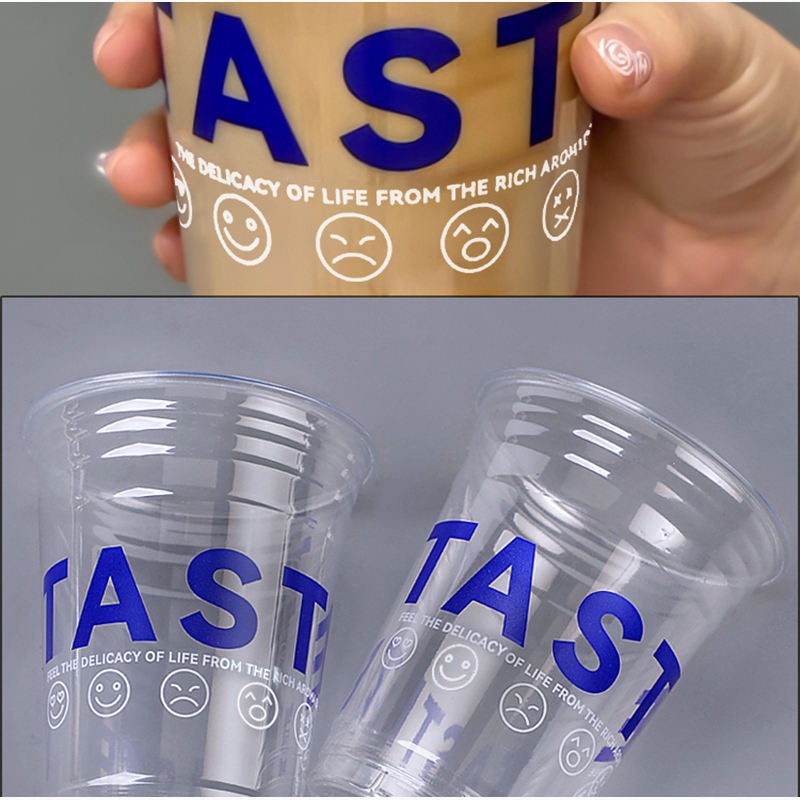
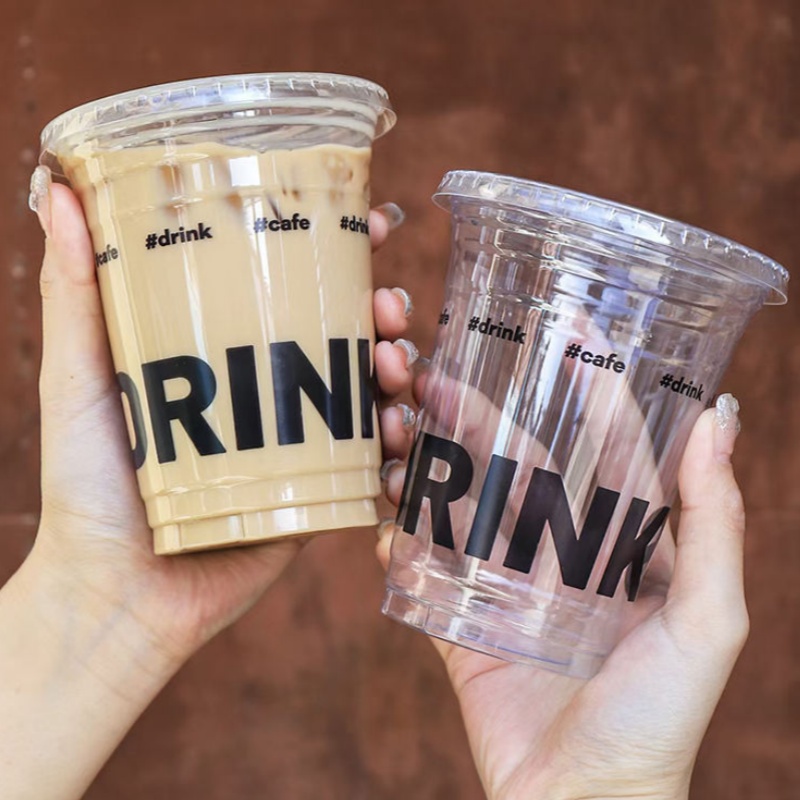
Advanced decoration techniques including direct digital printing, shrink sleeve labeling, and in-mold labeling provide extensive design flexibility. UV-curable inks deliver vibrant colors with excellent adhesion and abrasion resistance, maintaining visual appeal throughout distribution and consumption.
Tactile finishes, metallic effects, and matte coatings enable premium positioning while maintaining recyclability. Water-based coating systems enhance sustainability profiles without compromising performance characteristics or visual impact.
PET cans for cold brew coffee utilize various closure technologies including easy-open ends (EOE), resealable caps, and pull-tab systems. Aluminum EOE lids provide hermetic seals maintaining product freshness while offering convenient opening mechanisms familiar to consumers.
Threaded plastic closures enable resealing for multi-serve formats, extending consumption occasions and reducing waste. Tamper-evident features integrated into closure designs ensure product integrity and consumer safety throughout the distribution chain.

Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
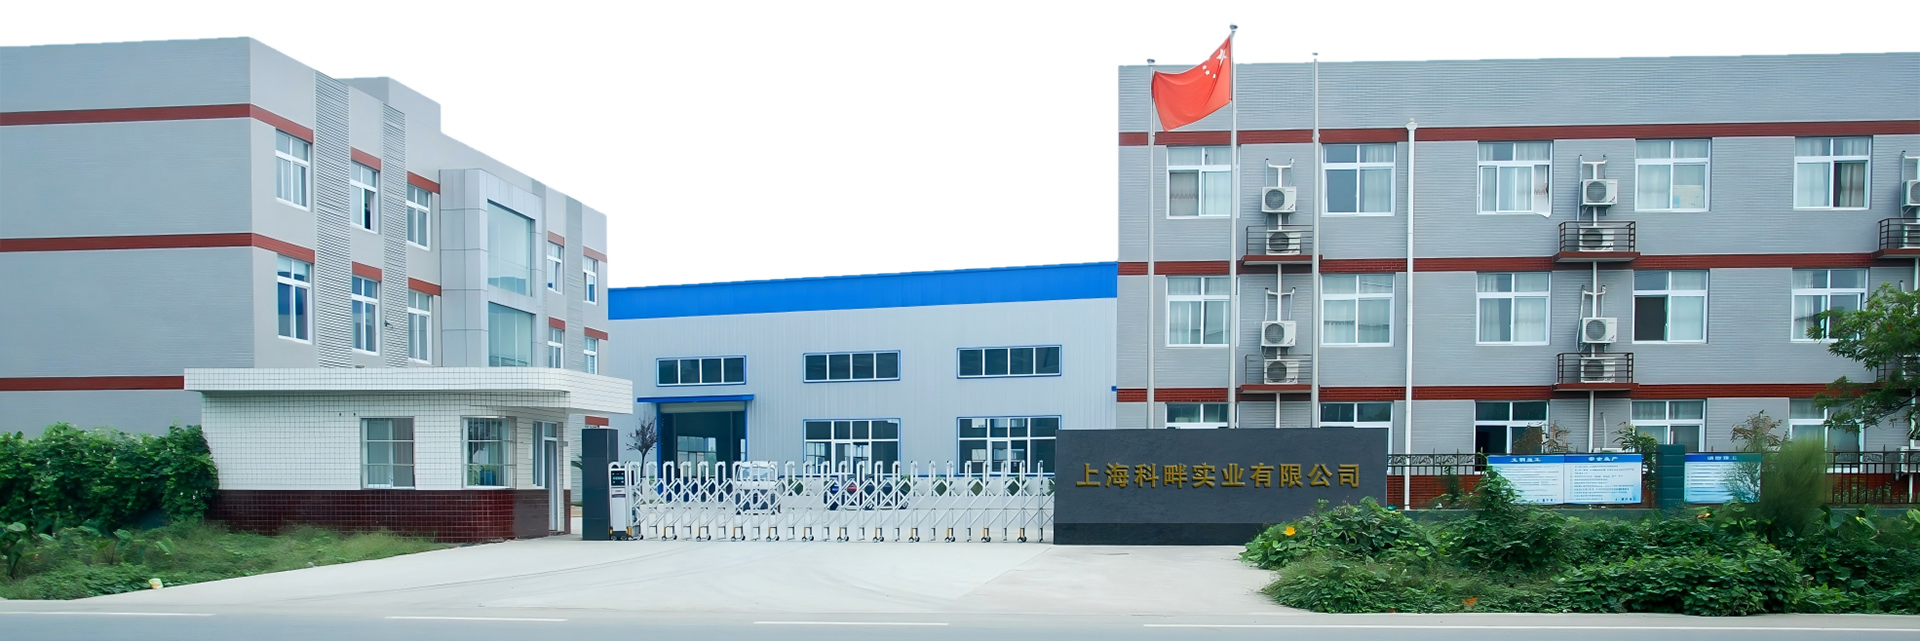
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
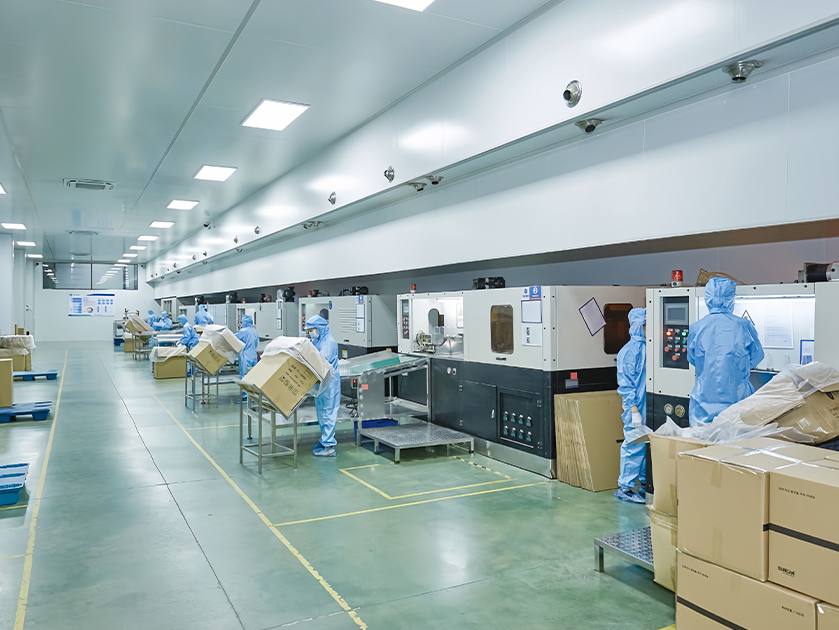
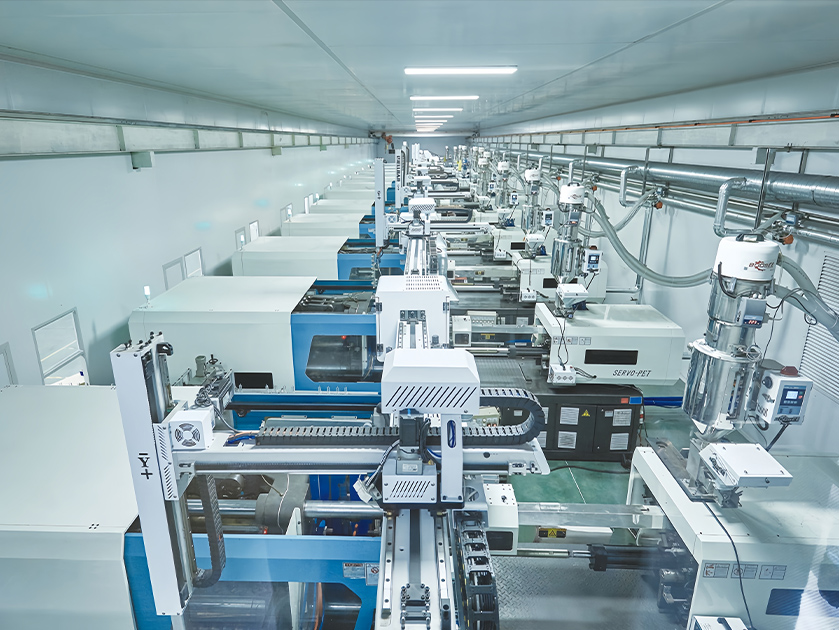
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
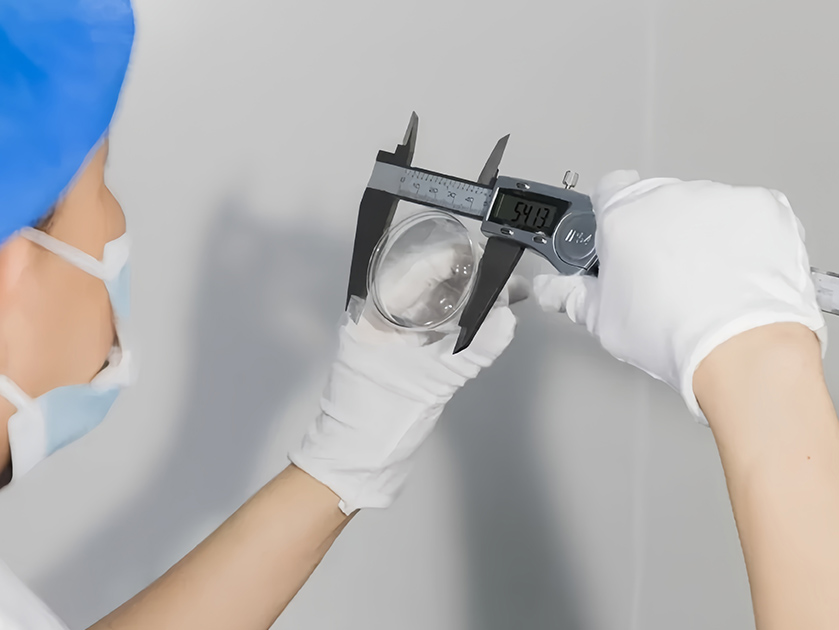
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
Contact UsAdhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
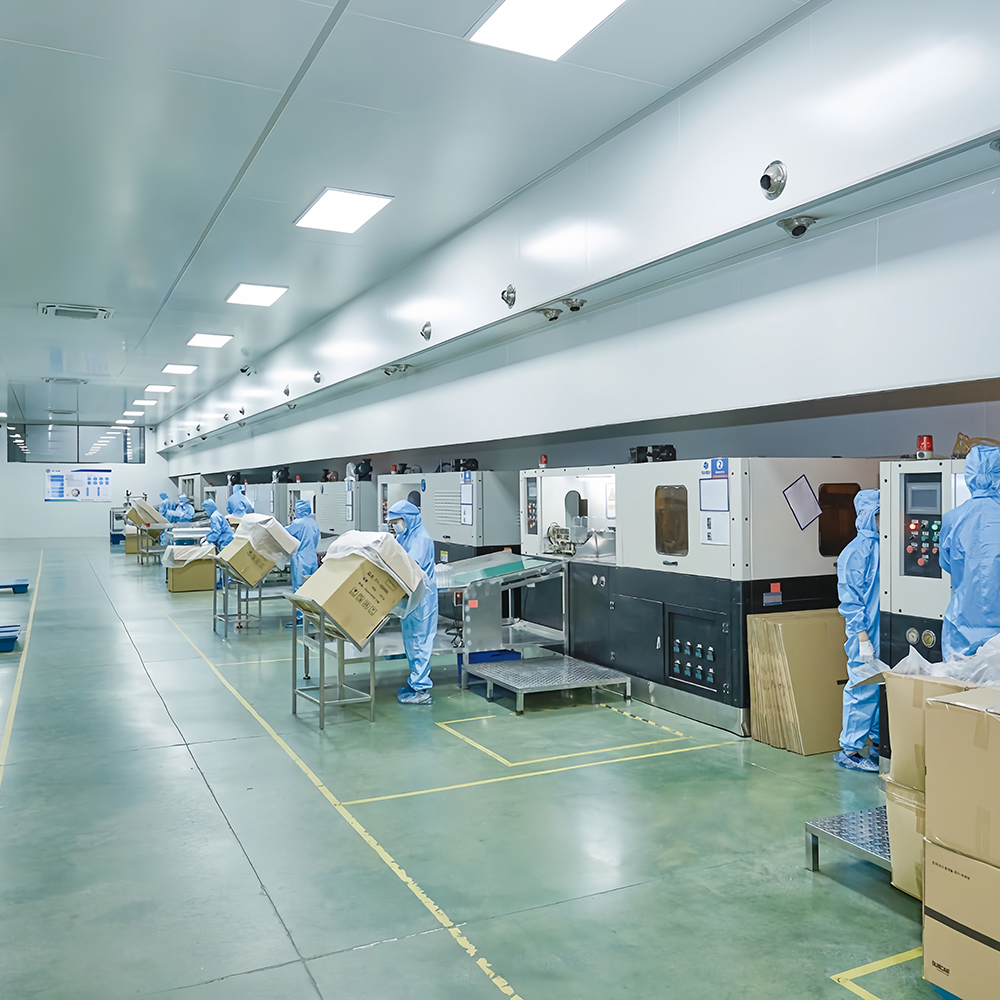
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
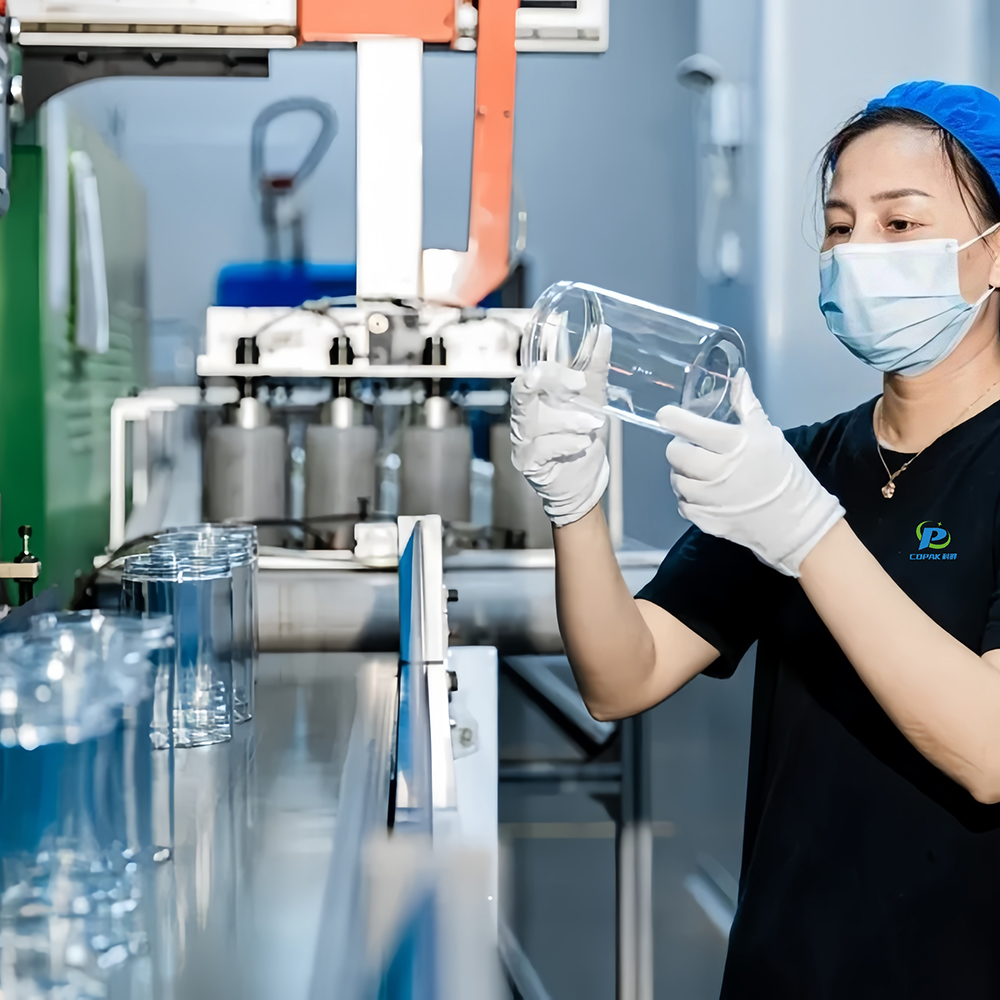
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
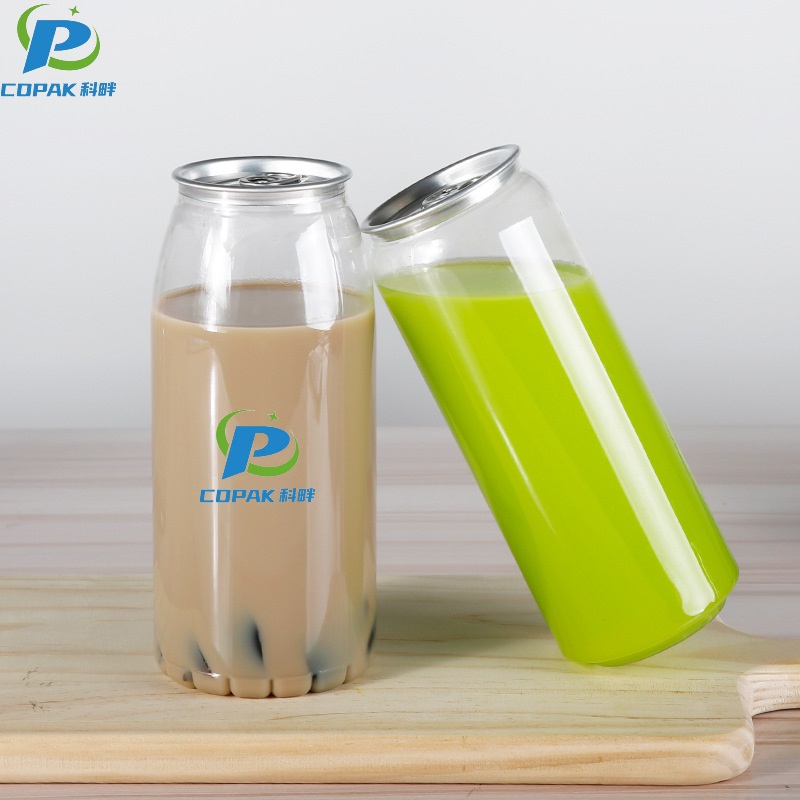
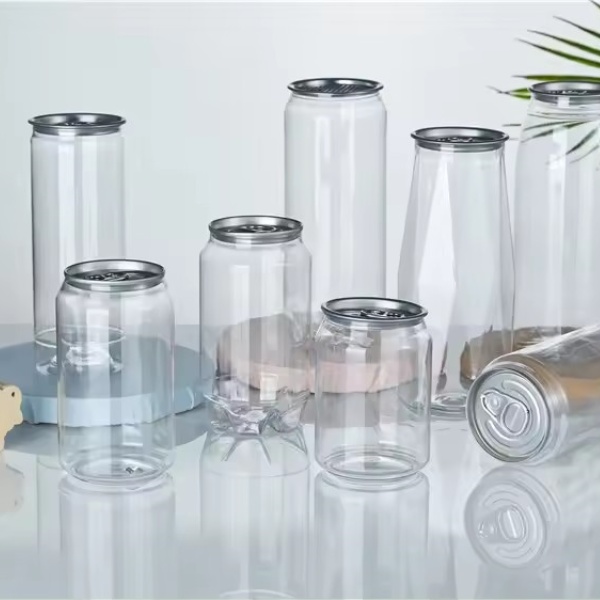
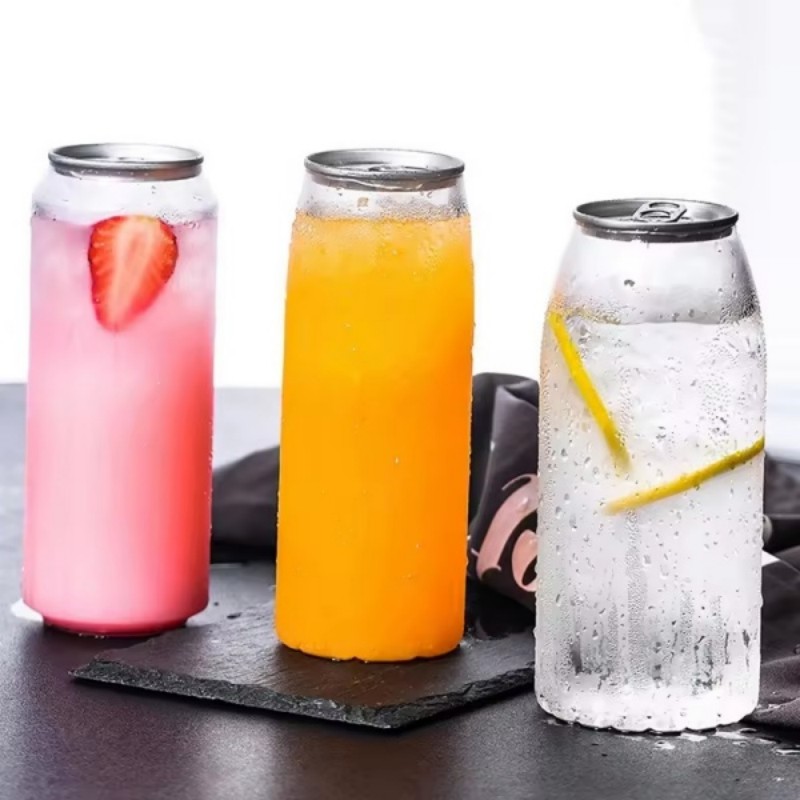
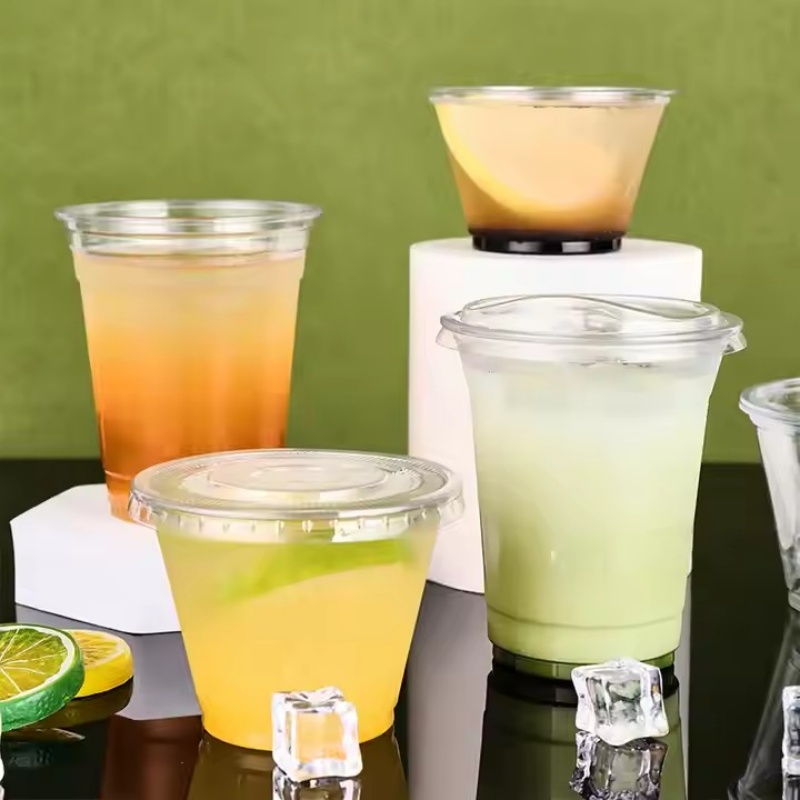
Explore our comprehensive range of PET beverage cans and cups designed specifically for artisanal cold brew coffee applications
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.