Leave Your Message
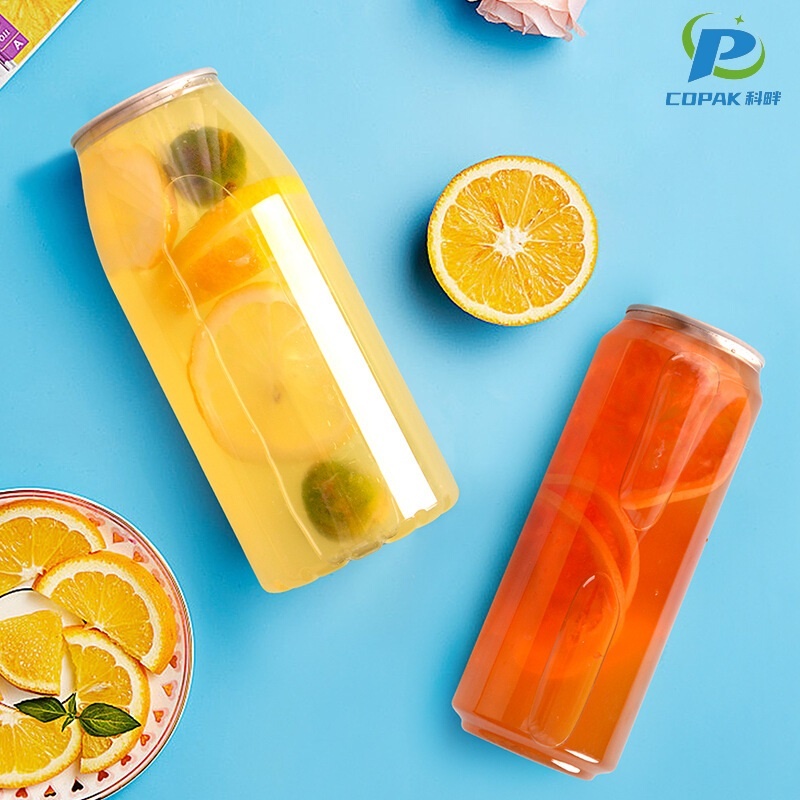
Explore our top-selling PET packaging solutions — purpose-built for carbonated and sparkling beverages with outstanding clarity and seal integrity.
Understanding the commercial landscape driving demand for transparent, pressure-resistant PET packaging solutions worldwide.
The global sparkling water market is projected to exceed USD 75 billion by 2030, with high clarity PET cans emerging as the fastest-growing packaging format — driven by consumer demand for product visibility, sustainability, and premium brand experience.
The global sparkling mineral water segment has witnessed a compound annual growth rate (CAGR) exceeding 8% over the past five years. Premiumization trends, health-conscious consumer behavior, and the shift away from sugary sodas have collectively accelerated demand for sparkling water. High clarity PET cans are now a preferred packaging choice for both established brands and emerging craft beverage producers looking to differentiate on shelf.
Major beverage manufacturers across North America, Europe, and Asia-Pacific are rapidly transitioning from traditional aluminum cans and glass bottles to high clarity PET cans. The ability to visually showcase sparkling water's effervescence and purity has become a powerful marketing asset. Industrial filling lines are being upgraded globally to accommodate PET can formats, reflecting a structural shift in beverage packaging infrastructure.
Environmental regulations and ESG commitments are reshaping packaging choices across the beverage industry. High clarity PET cans offer a compelling sustainability profile — they are fully recyclable, lighter than glass, and compatible with recycled PET (rPET) content. Leading brands are now specifying rPET-based clear cans to meet carbon reduction targets while maintaining the premium aesthetic demanded by sparkling mineral water consumers.
Innovation in materials science, barrier engineering, and smart packaging is reshaping what PET cans can deliver for sparkling mineral water brands.
One of the most critical technical challenges for PET cans in sparkling water applications is CO₂ retention. Next-generation multi-layer PET structures and active barrier coatings are dramatically extending shelf life, enabling carbonation retention comparable to aluminum — a milestone that is unlocking new retail channels and geographies for PET-packaged sparkling water.
Advances in PET resin formulation and blow-stretch molding processes are achieving near-glass optical clarity. Haze values below 2% are now achievable at commercial scale, allowing consumers to see the sparkle and purity of mineral water directly through the can wall — a feature that commands premium shelf positioning and higher retail price points.
Material reduction without compromising pressure resistance is a key engineering frontier. Finite element analysis and AI-assisted mold design are enabling thinner wall profiles that maintain the structural integrity required for carbonated beverages. Lightweighting reduces material costs, lowers carbon footprint per unit, and improves logistics economics across the entire supply chain.
The integration of NFC chips, QR codes, and digital watermarks into high clarity PET cans is enabling direct consumer engagement. Sparkling water brands are leveraging these technologies to deliver origin stories, sustainability credentials, and loyalty programs — all accessible through the transparent can surface that doubles as a digital canvas.
Regulatory pressure and brand sustainability pledges are driving rapid scaling of recycled PET content in clear cans. Achieving high rPET percentages while maintaining optical clarity is a technical challenge that leading suppliers are actively solving through advanced sorting, decontamination, and reprocessing technologies — with commercial solutions now reaching 50–100% rPET formulations.
The flexibility of PET blow molding is enabling unprecedented customization in can geometry. Brands are commissioning unique silhouettes, embossed patterns, and tapered profiles that are impossible to achieve in aluminum. For sparkling mineral water, distinctive can shapes are becoming a primary brand equity asset, driving investment in custom tooling and exclusive packaging designs.
From premium retail to high-volume hospitality, discover the diverse commercial and industrial applications driving adoption of clear PET cans.
High clarity PET cans enable sparkling mineral water brands to create compelling shelf displays where product purity and effervescence are visible to consumers. The glass-like appearance commands premium shelf positioning and supports higher retail price points in natural food stores, specialty grocers, and upscale supermarket chains.
The lightweight nature and shatter-proof properties of PET cans make them ideal for airline catering and airport retail. High clarity formats allow passengers to see the sparkling water quality they are consuming, while the reduced weight compared to glass contributes meaningfully to fuel efficiency and carbon reduction targets for aviation clients.
Five-star hotels and luxury resorts are increasingly specifying custom-branded high clarity PET cans for in-room sparkling water service. The ability to print photorealistic graphics on transparent PET creates a premium branded experience that aligns with luxury hospitality aesthetics, while eliminating the breakage risk associated with glass bottles.
Music festivals, sporting events, and outdoor venues benefit from the safety and portability of PET cans. Clear PET sparkling water cans serve as both a beverage container and a brand communication vehicle, with the transparent format allowing event organizers to showcase premium mineral water offerings to health-conscious attendees.
The functional beverage sector — including mineral-enriched sparkling waters, electrolyte drinks, and wellness-focused carbonated beverages — is a high-growth application for clear PET cans. Consumers in this segment actively seek product transparency, making the visual clarity of PET packaging a key purchasing driver aligned with ingredient transparency values.
High clarity PET cans are gaining traction in food service channels, where chefs and restaurateurs value the ability to present sparkling mineral water in packaging that complements the dining aesthetic. Custom-branded PET cans with restaurant logos are becoming a signature element of the premium dining experience across fine dining and boutique restaurant concepts.
The direct-to-consumer channel is driving rapid adoption of high clarity PET cans for sparkling water brands. The visual appeal of transparent packaging translates powerfully to product photography and online listings, while the shatter-proof nature of PET eliminates breakage losses that plague glass bottle shipments — a critical logistics advantage for e-commerce fulfillment.
Hospitals, wellness centers, and corporate campuses are specifying high clarity PET sparkling water cans as part of healthy lifestyle initiatives. The clean, clinical aesthetic of transparent packaging aligns with healthcare brand values, while the absence of BPA and compliance with FDA food-contact standards ensures suitability for health-sensitive environments and populations.
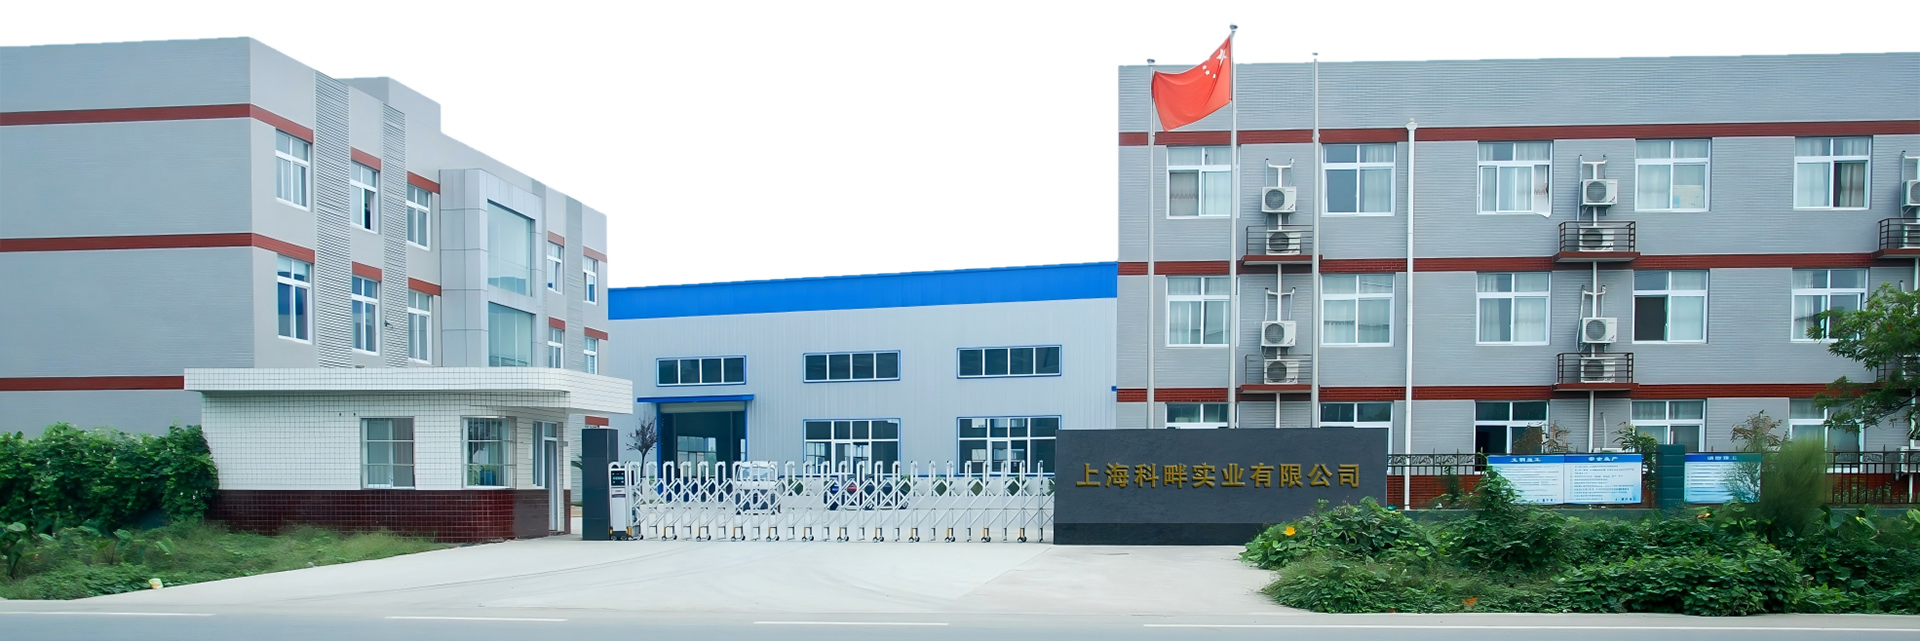
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities — from 1oz to 32oz — available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
Contact Us →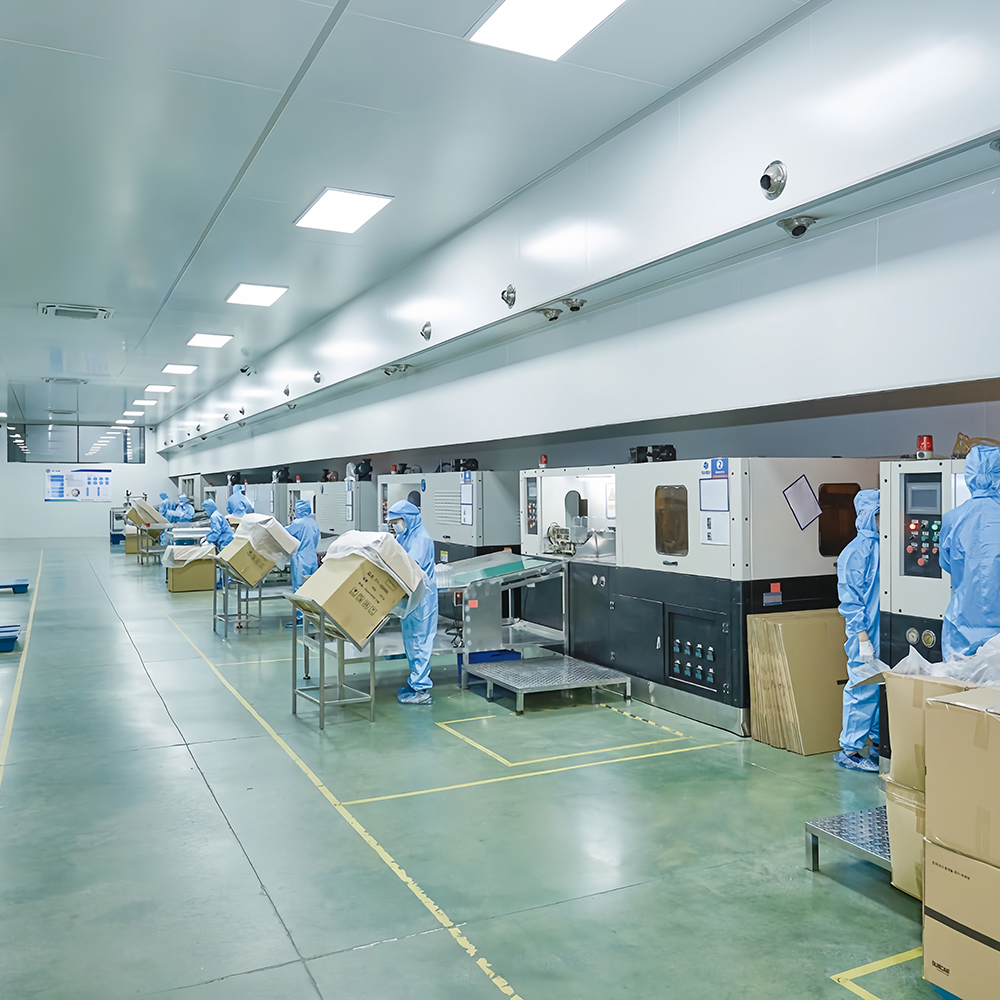
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production.
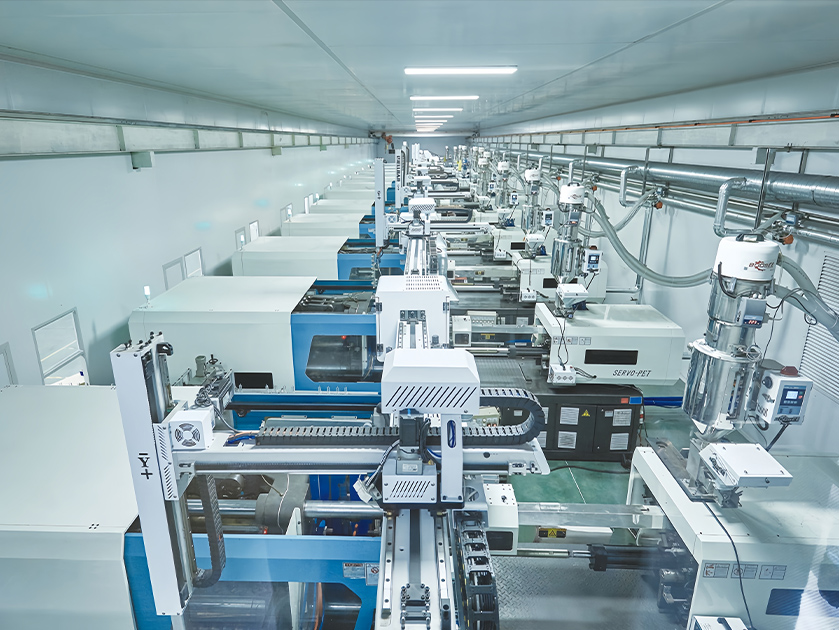
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
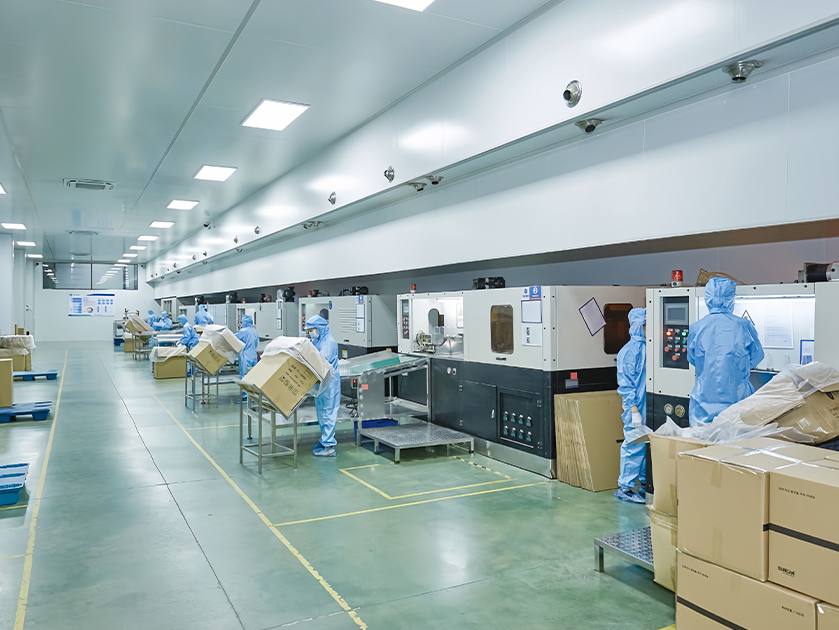
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
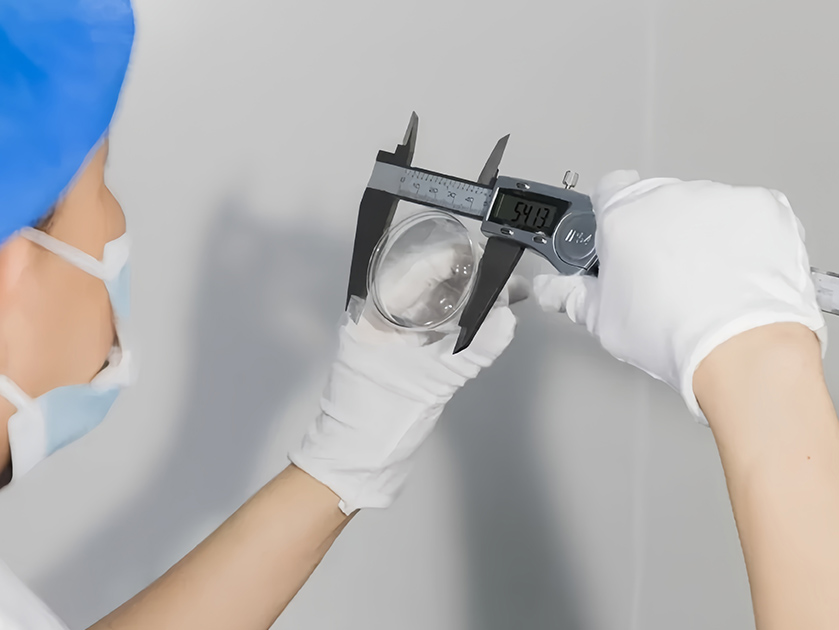
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
COPAK is committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET materials into our cup and can manufacturing.
For sparkling mineral water brands with ambitious sustainability targets, our rPET-compatible high clarity can solutions provide a direct pathway to measurable carbon reduction without compromising the premium visual experience that drives consumer preference.
Contact UsFrom energy-efficient blow molding processes to closed-loop material recycling programs, every aspect of our manufacturing is designed to minimize environmental impact. We partner with sparkling water brands to develop packaging solutions that meet the most demanding ESG criteria while delivering the clarity and carbonation performance the market demands.
We offer extensive customization options to meet the unique requirements of beverage brands and clients, including tailored shapes, sizes, and capacities for PET cups and cans. Additionally, we provide full support for custom mold development and personalized printing solutions.
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
Contact us →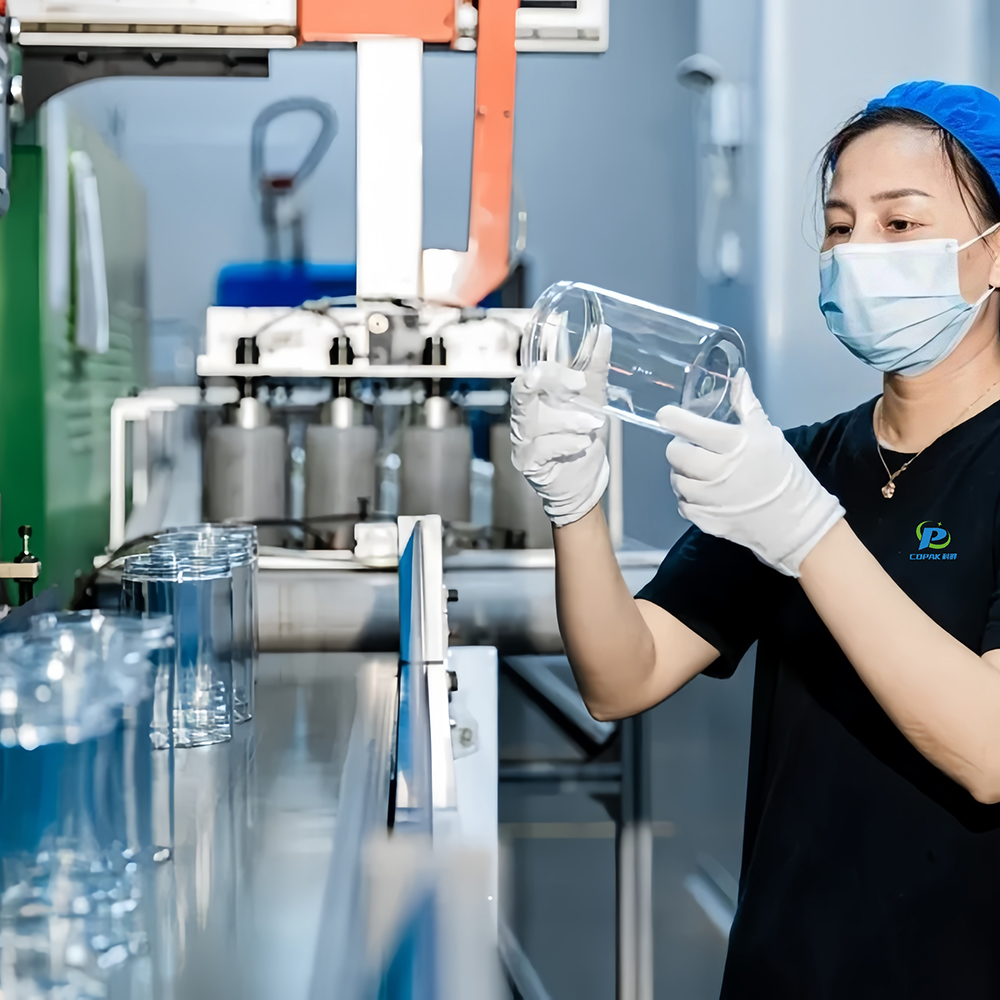
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
Contact us →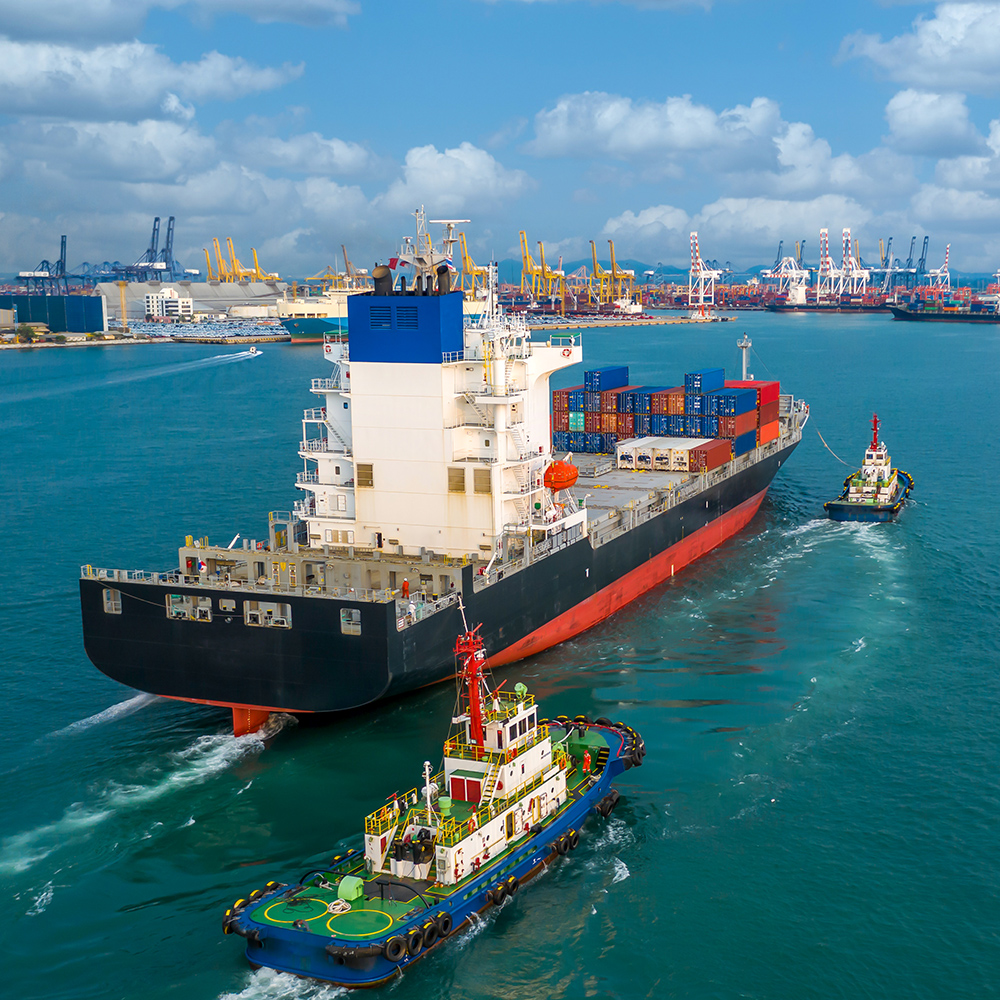
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
Contact us →
Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Having supplied PET cups and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
INQUIRY NOWBrowse our full range of high clarity PET cans and cups — available in custom sizes, shapes, and printed finishes for every sparkling beverage application.