

Leave Your Message
Explore our top-tier clear PET cans and recycled RPET solutions engineered specifically for carbonated beverages.
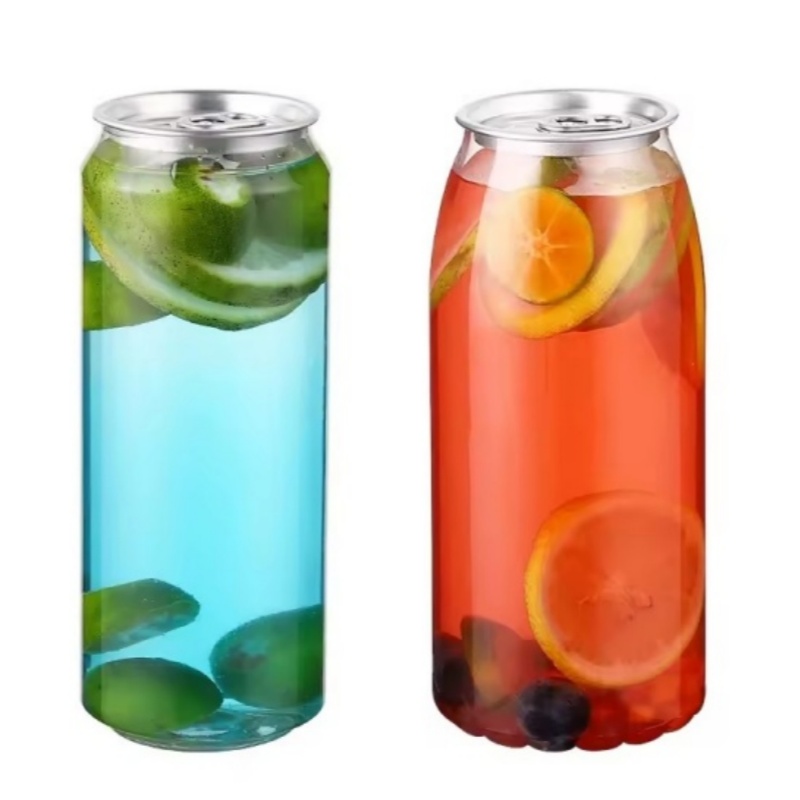
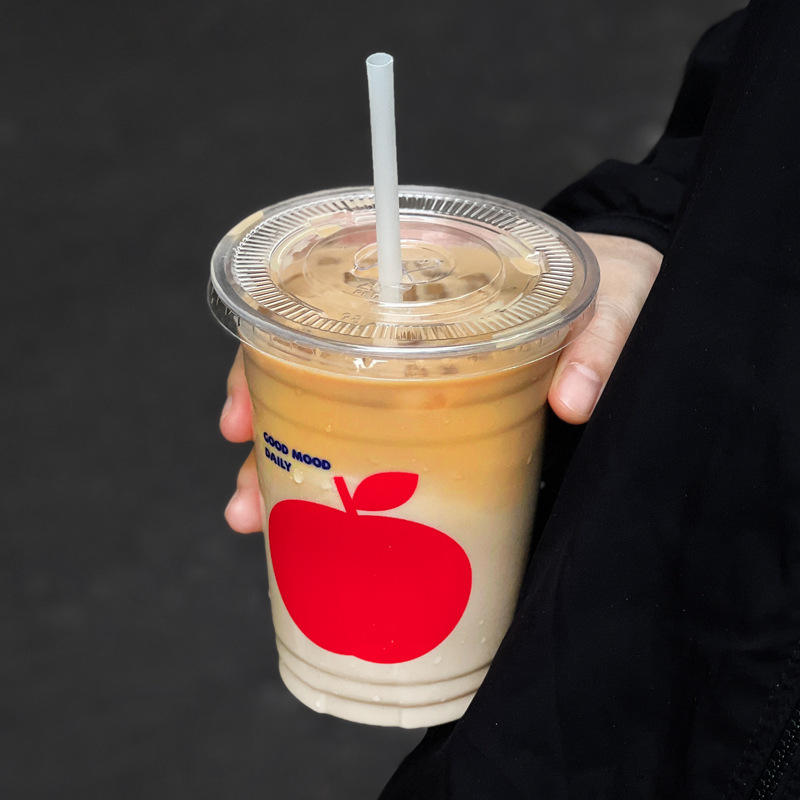
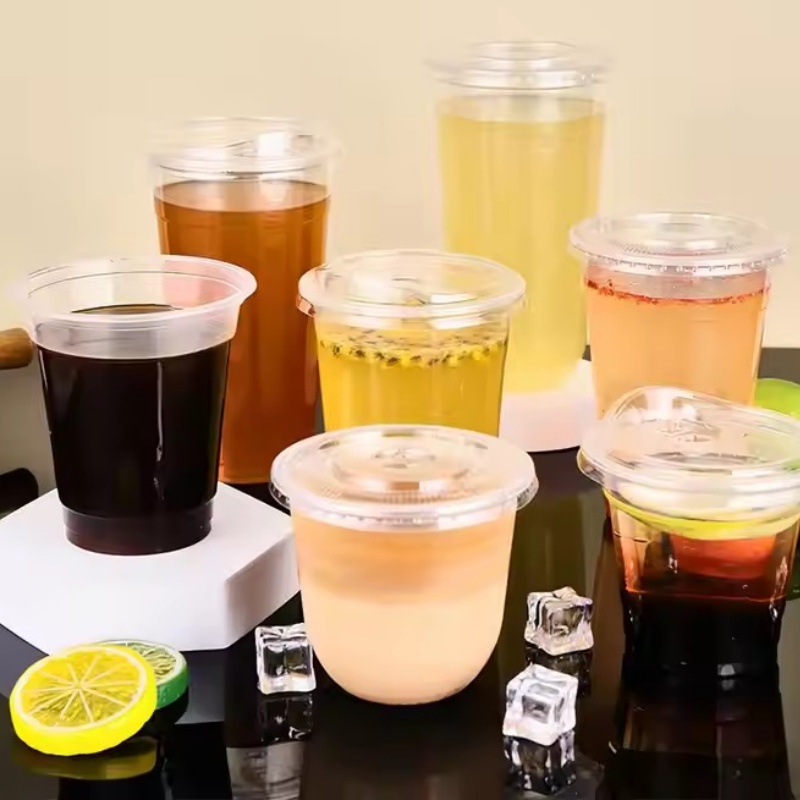
The global beverage market is experiencing a paradigm shift. Consumers are no longer satisfied with just taste; they demand transparency, aesthetic appeal, and environmental responsibility. The rise of Clear PET Cans for Sparkling Mineral Water sits at the intersection of these demands. Combining the structural advantages of traditional metal cans with the crystal-clear transparency of glass, PET cans have emerged as a disruptive packaging format that enhances brand visibility and consumer trust.
Historically, sparkling mineral water has been dominated by glass bottles and aluminum cans. While glass offers premium positioning, its weight, fragility, and high transport costs present significant logistical hurdles. Aluminum cans, on the other hand, offer excellent barrier properties but hide the visual purity of the product. The clear PET can bridges this gap, allowing the effervescent bubbles of sparkling mineral water to be fully visible on supermarket shelves. This visual transparency serves as a powerful marketing tool, directly communicating freshness, purity, and carbonation quality to the shopper.
From an industrial standpoint, the adoption of clear PET cans is accelerating rapidly. Beverage co-packers and brands are updating their filling lines to accommodate PET cans, utilizing hybrid seaming technologies that can seal aluminum easy-open ends (EOE) onto PET bodies. This compatibility lowers the barrier to entry for established brands looking to diversify their packaging portfolio without completely replacing their existing canning infrastructure.
One of the primary challenges in packaging sparkling mineral water in plastic is maintaining the carbonation. Carbon dioxide (CO2) molecules are highly permeating, and standard PET can allow gas to escape over time, leading to a flat beverage. To solve this, advanced injection stretch blow molding (ISBM) techniques are employed to optimize the molecular orientation of the PET material, significantly improving its gas barrier properties.
Modern clear PET cans are engineered with specialized barrier coatings or multi-layer structures that minimize CO2 loss and prevent oxygen ingress. This ensures that the sparkling water retains its crisp, fizzy texture throughout its target shelf life. Additionally, the integration of high-precision aluminum or PET easy-open lids creates a hermetic seal that withstands the internal pressure generated by carbonated waters, preventing leakage during transit and storage.
Showcase the sparkling bubbles and natural purity of your mineral water, driving impulsive purchases and reinforcing brand premiumization.
Optimized molecular structure designed to lock in carbonation (CO2) and prevent oxygen entry, maintaining beverage freshness.
Compatible with existing PET recycling streams worldwide, supporting circular economy initiatives and reducing carbon footprints.
The versatility of clear PET cans opens up new consumption occasions and distribution channels for sparkling mineral water brands:
SHANGHAI COPAK INDUSTRY CO., LTD.
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
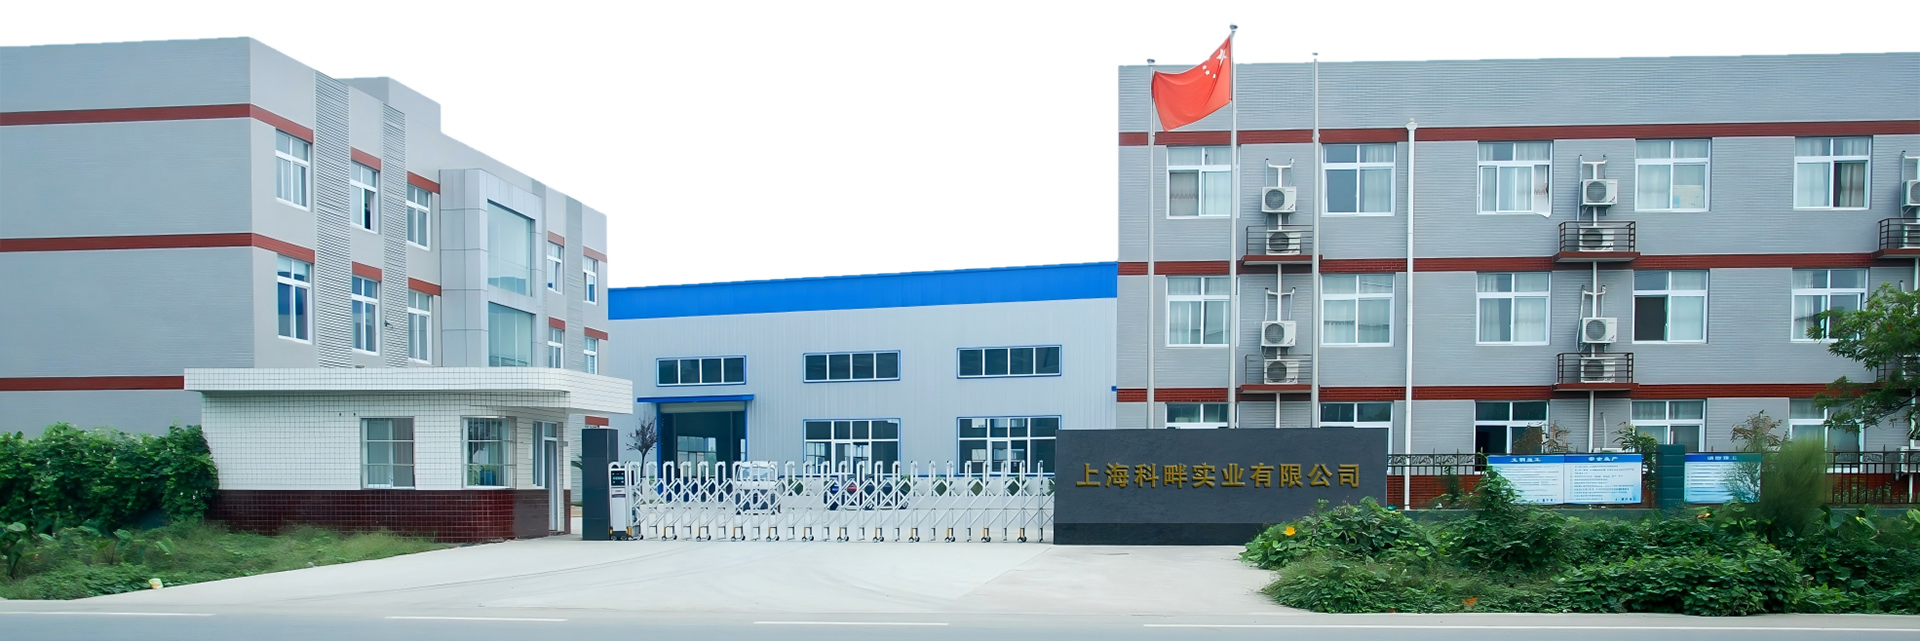
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production.
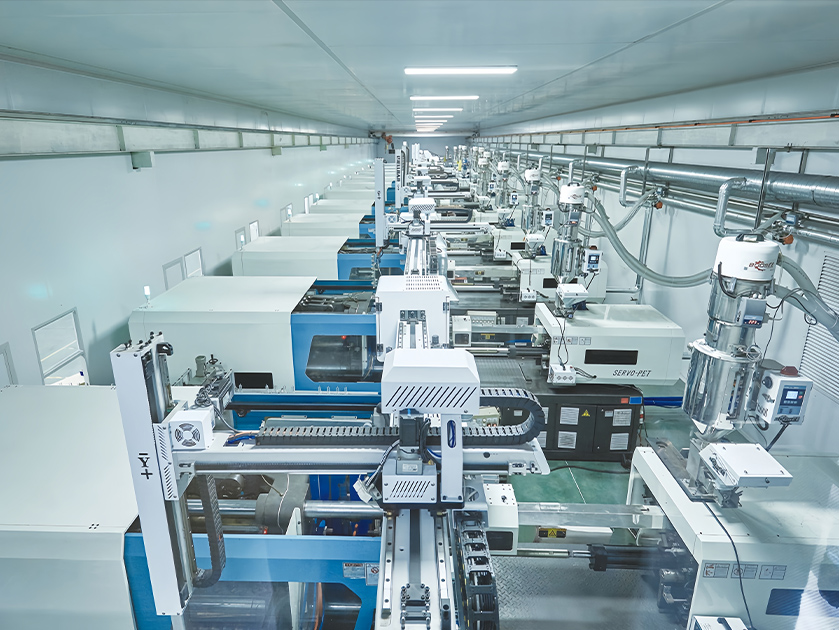
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
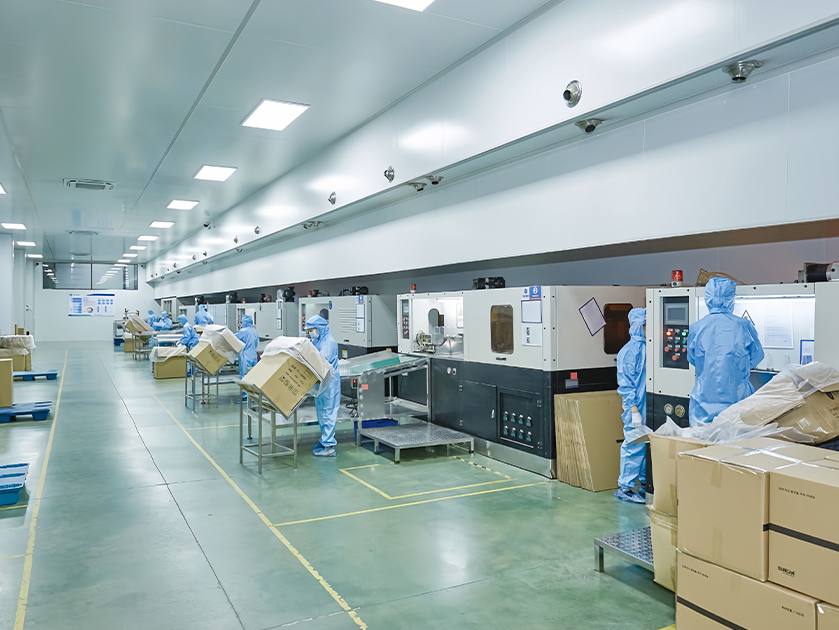
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
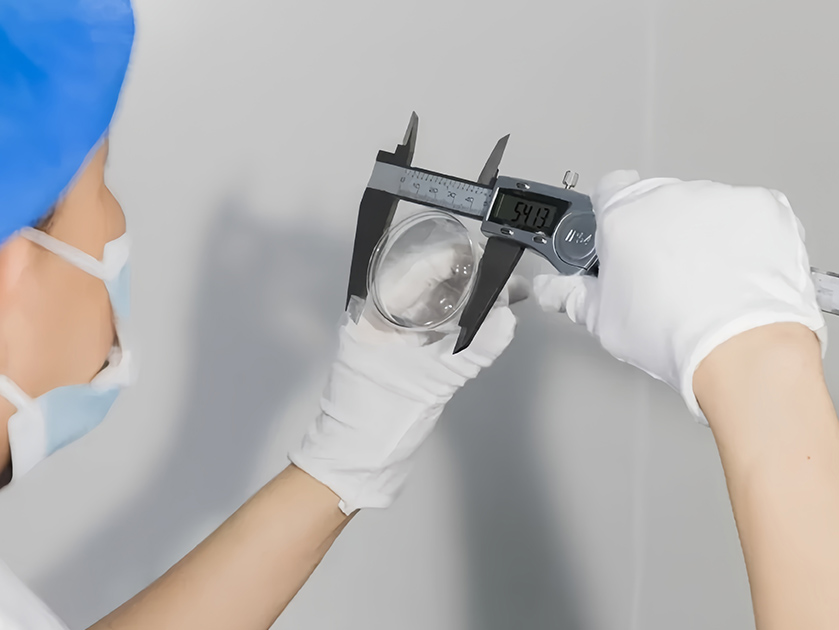
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
We offer extensive customization options to meet the unique requirements of beverage brands and clients, including tailored shapes, sizes, and capacities for PET cups and cans.
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
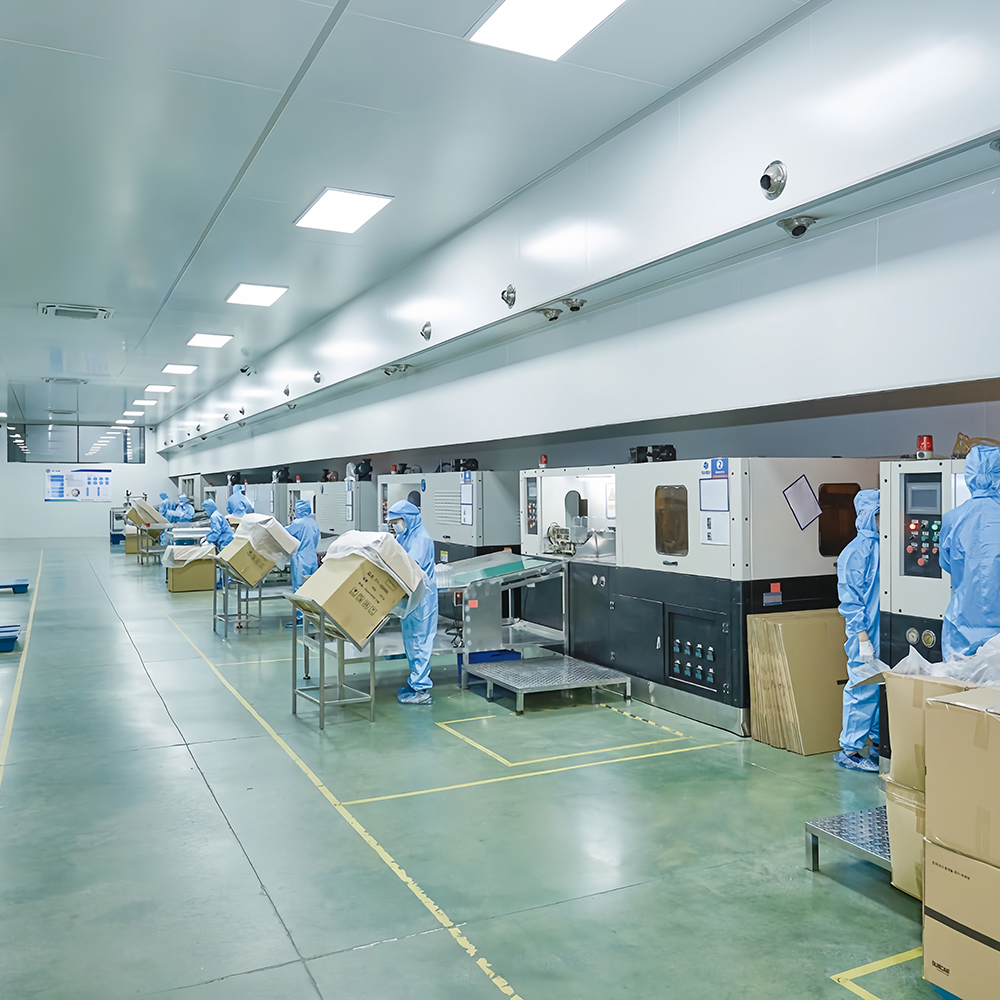
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
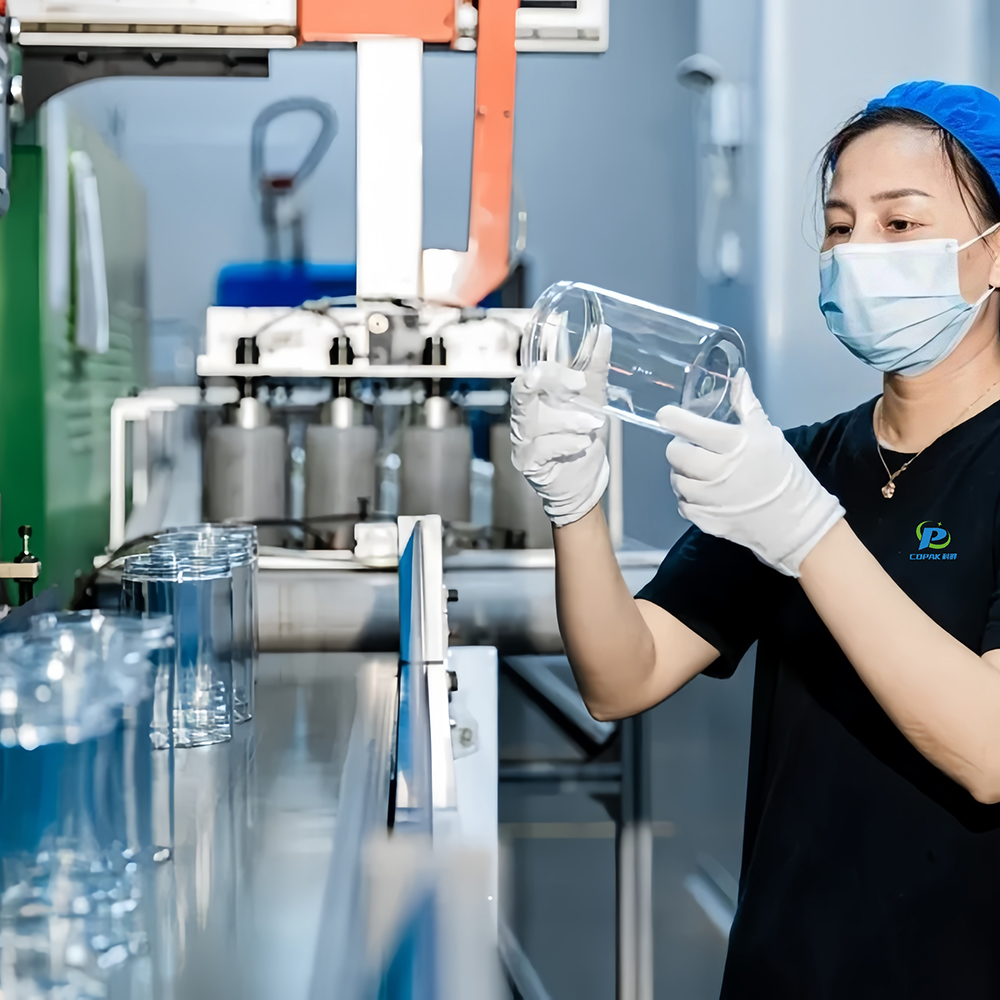
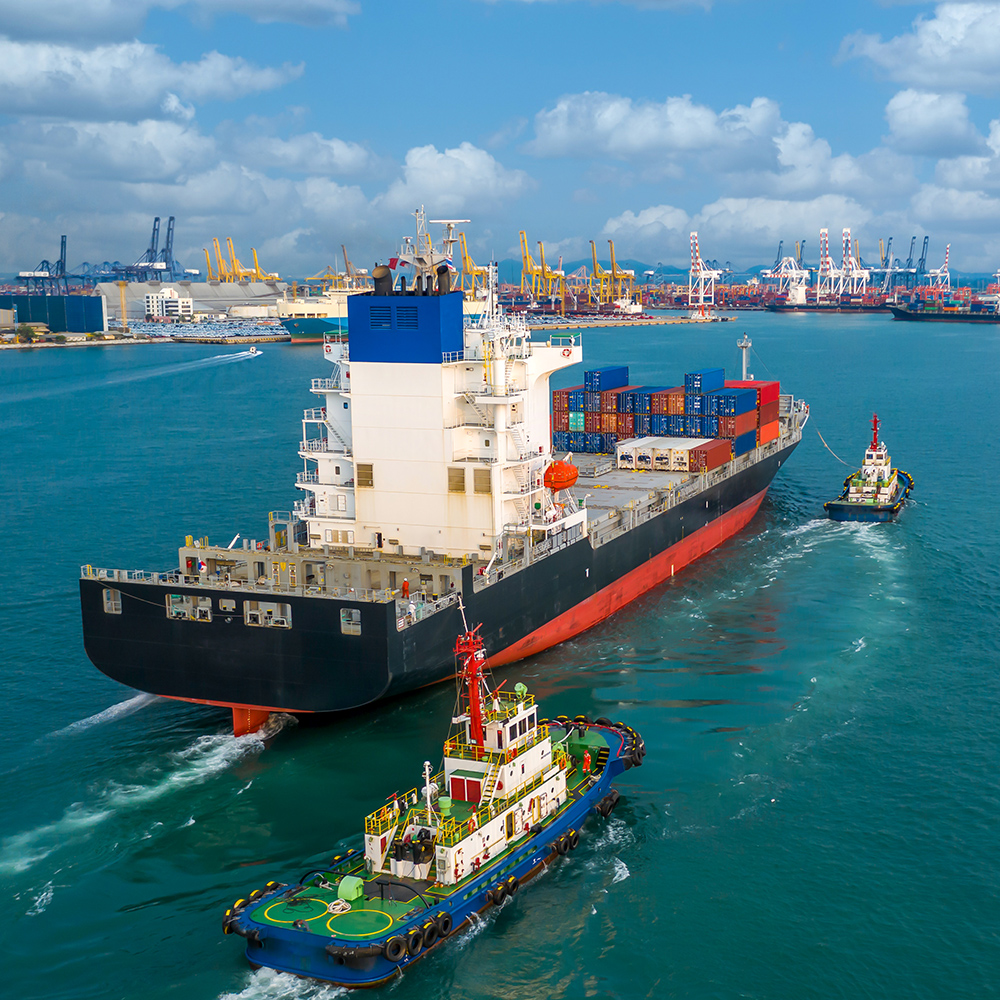
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
Why choose COPAK as your long-term packaging partner?

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
Browse our full range of high-quality PET packaging, recycled cups, and advanced automatic sealing machinery.
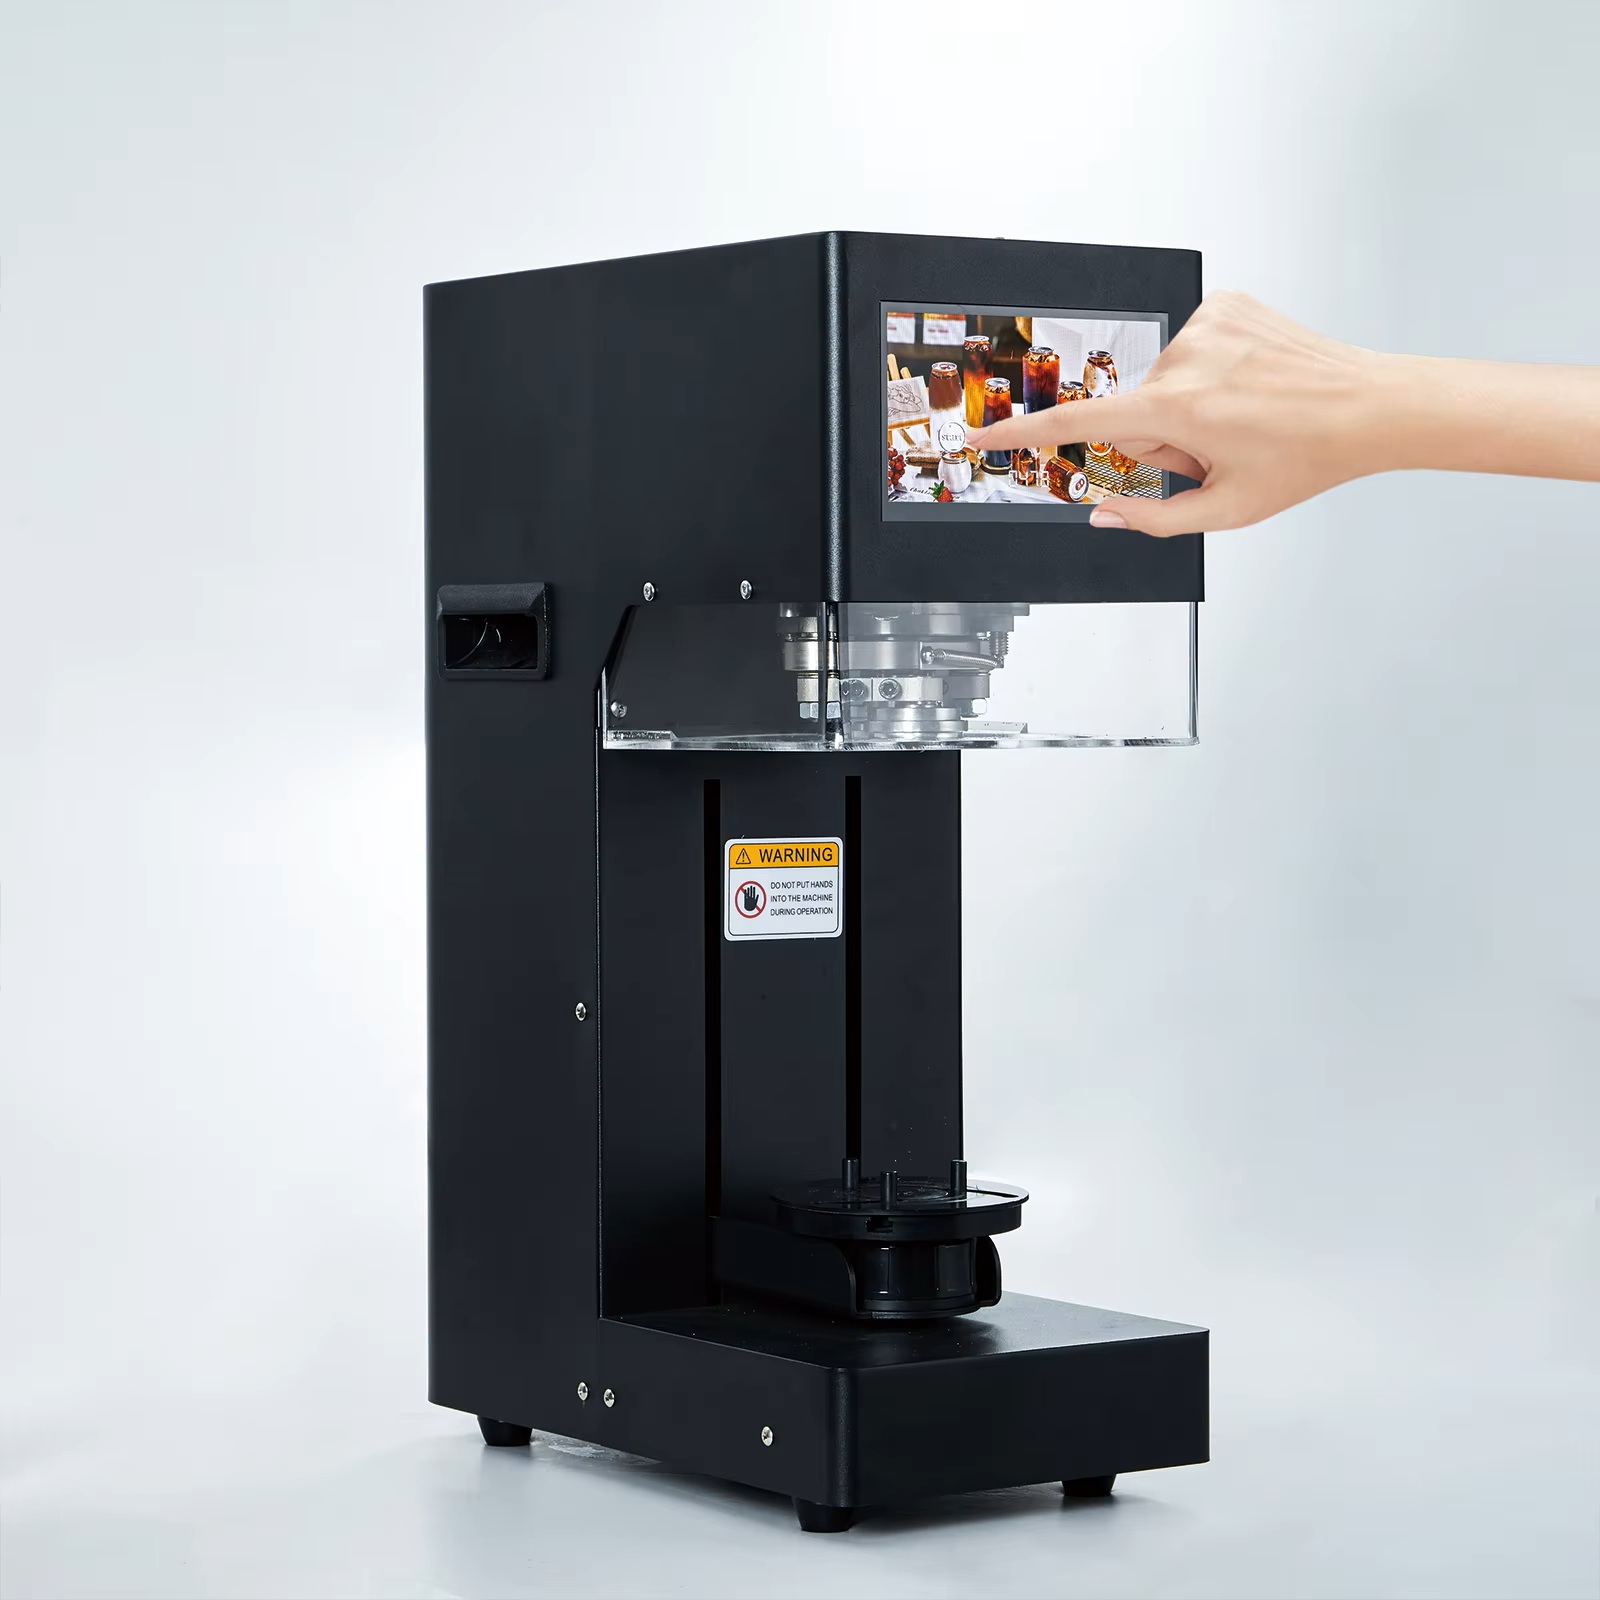
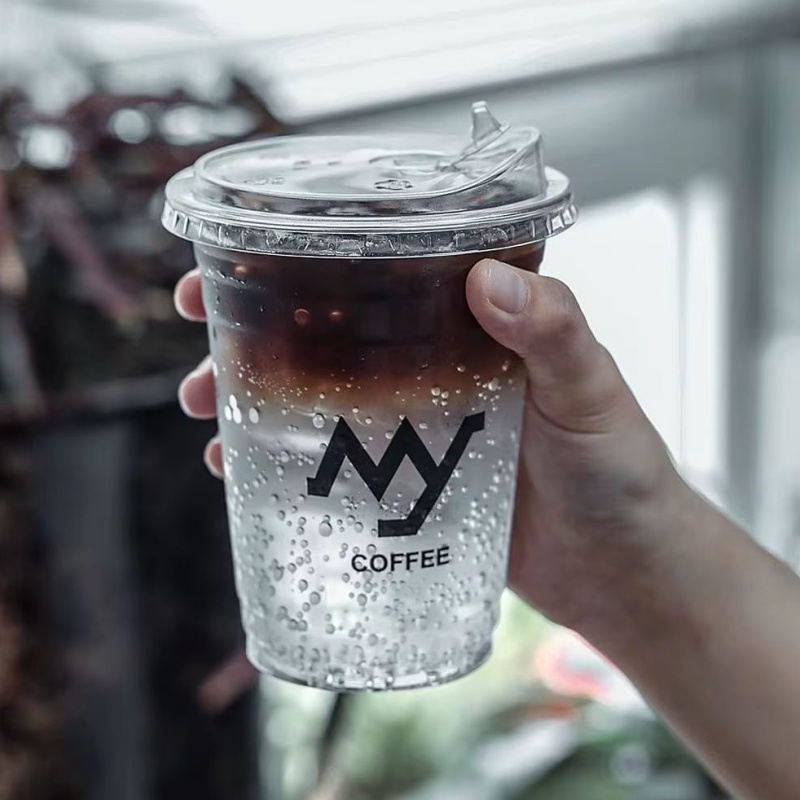
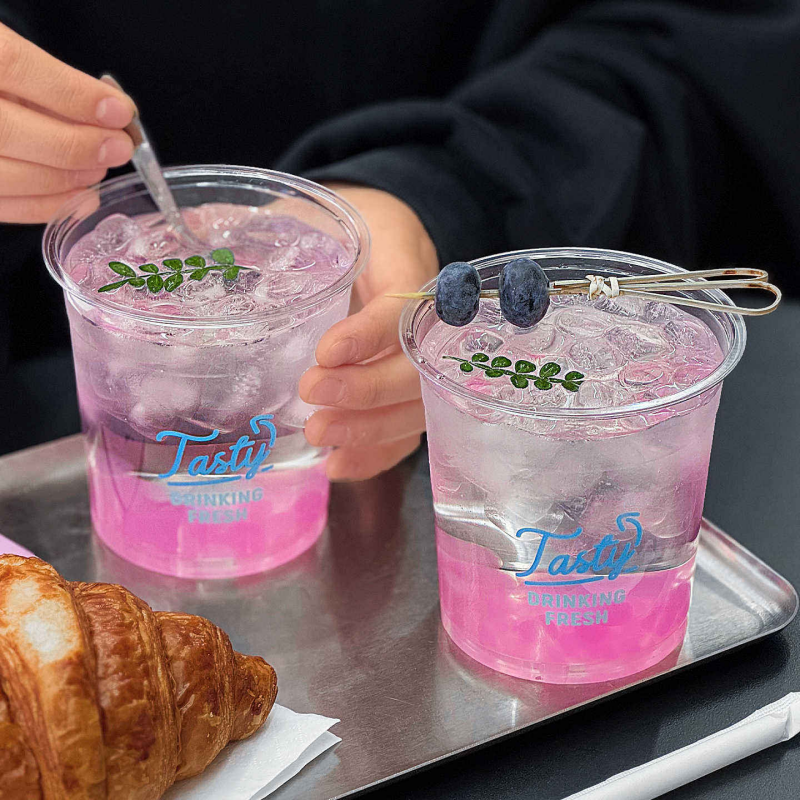
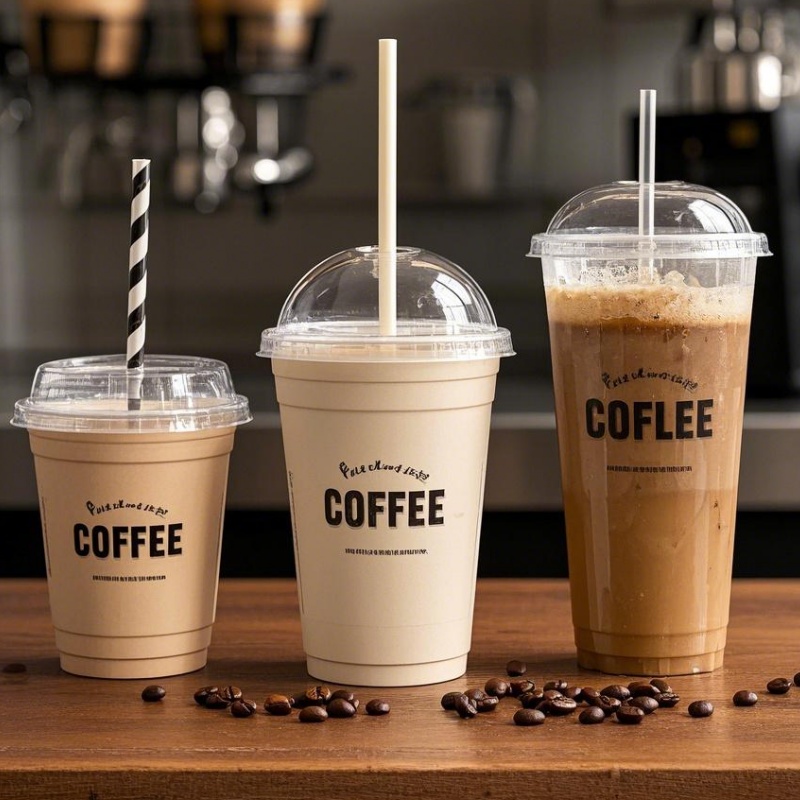
Having supplied PET cups and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
INQUIRY NOW