Leave Your Message
Explore our highly recommended PET cans and tasting cups designed to enhance brand appeal and preserve active probiotic cultures.
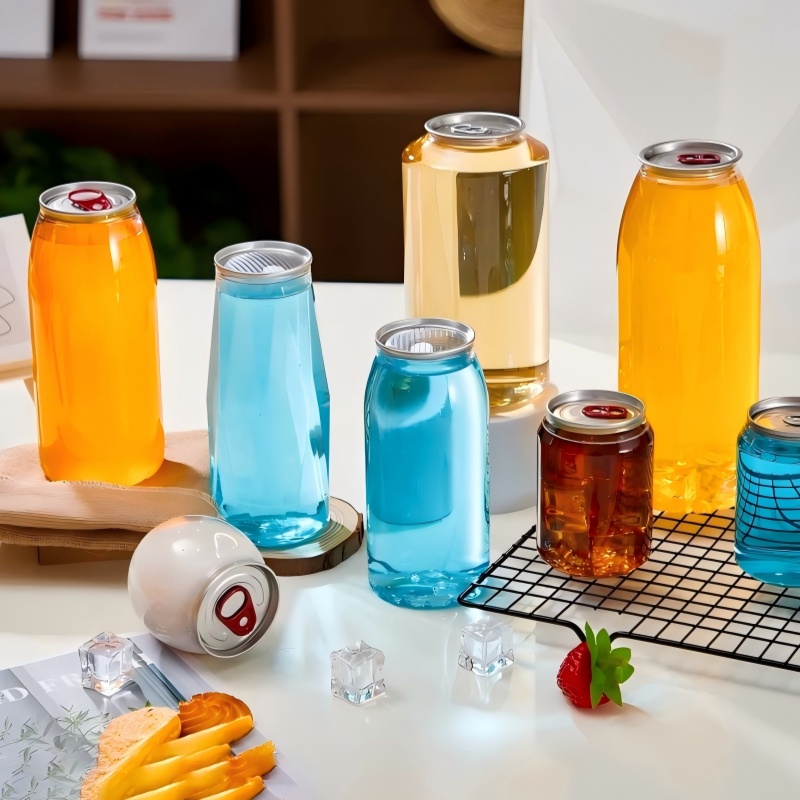
The organic beverage industry is witnessing an unprecedented transformation. Organic kombucha, traditionally packaged in heavy, fragile amber glass bottles, is rapidly transitioning to modern, lightweight alternatives. Among these, the 500ml PET Beverage Can has emerged as the premier standard for forward-thinking brands globally.
This shift is driven by modern consumer lifestyles. Today’s wellness-conscious consumers demand convenience, portability, and safety. Unlike glass, which is prohibited at beaches, pools, music festivals, and fitness centers, PET cans allow kombucha brands to access previously restricted outdoor distribution channels. The 500ml capacity represents the "sweet spot" for functional beverage consumption—providing a generous, satisfying single-serving portion that aligns with retail pricing strategies and consumer value perceptions.
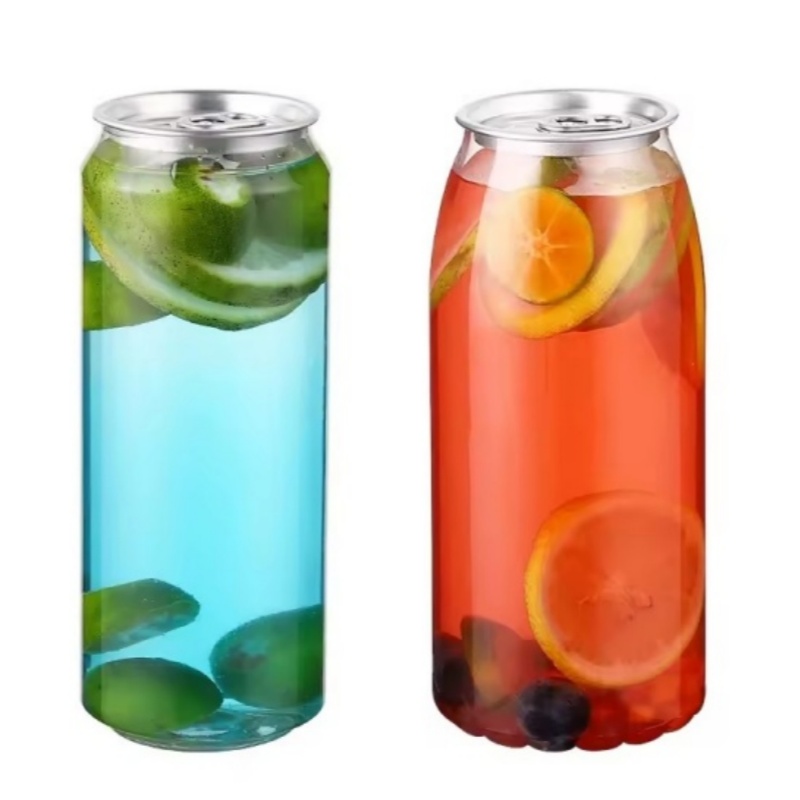
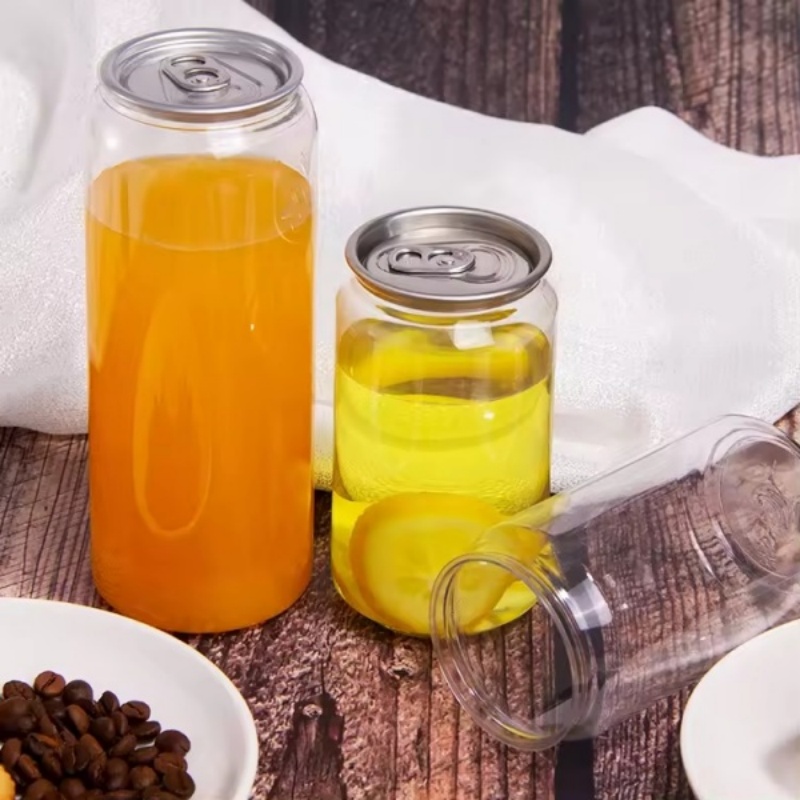
While aluminum cans offer portability, they lack visual transparency. Organic kombucha is a visually vibrant beverage, boasting beautiful natural hues derived from green tea, black tea, hibiscus, ginger, and raw fruit juices. A transparent 500ml PET can showcases these rich, organic colors directly to the consumer. This transparency acts as a powerful marketing tool on retail shelves, signaling freshness, purity, and premium quality. Consumers can physically verify the sediment and active cultures that define authentic, raw kombucha, building immediate brand trust.
How our 500ml PET beverage cans solve real-world industrial, logistical, and retail challenges for organic beverage producers.
Organic kombucha is a living product containing active yeast and bacteria. Even under cold-chain storage, slow secondary fermentation can occur, releasing carbon dioxide. Traditional rigid packaging can risk bursting under excessive pressure, while low-grade plastics can warp or bloat.
COPAK's 500ml PET beverage cans are specifically engineered with optimized wall thickness and a structured base profile. This design safely accommodates moderate internal pressure variations without compromising the structural integrity or aesthetic profile of the can. Combined with standard aluminum easy-open ends (EOE), our cans maintain an airtight seal that locks in carbonation while preventing oxygen ingress, thereby extending the shelf life of raw, unpasteurized kombucha.
The rise of direct-to-consumer (D2C) subscription models has forced kombucha brands to reconsider their shipping efficiencies. Shipping glass bottles requires extensive protective bubble wrap, increases package volume, and adds significant weight, leading to higher shipping costs and carbon emissions.
Our 500ml PET cans are shatterproof and exceptionally lightweight. By eliminating the risk of breakage during transit, brands can optimize their logistics, reduce packaging waste, and lower shipping costs by up to 35%. Furthermore, the uniform cylindrical shape of our 500ml cans allows for dense, efficient packing in shipping boxes and retail cold displays, maximizing shelf space utilization.
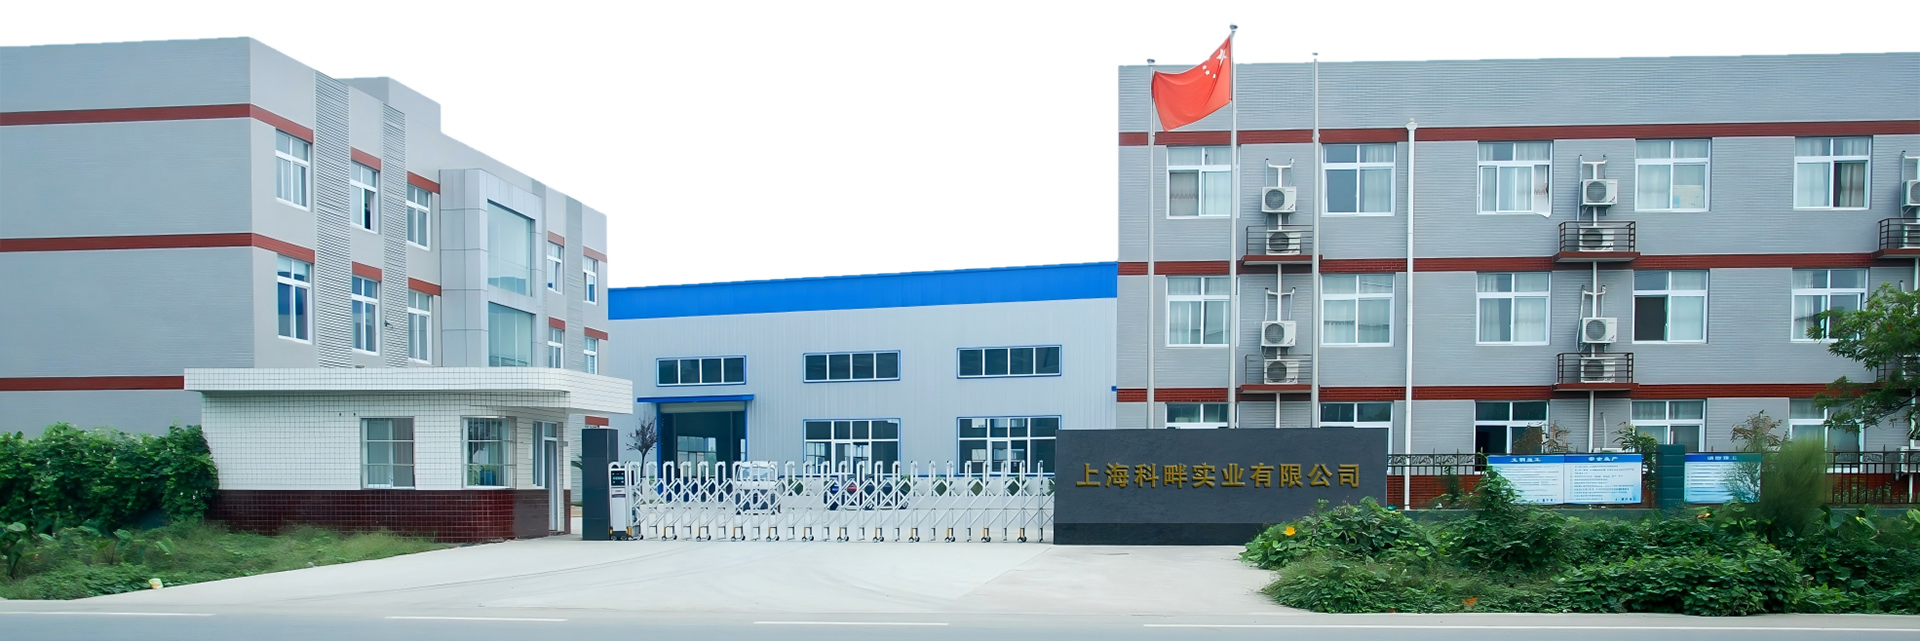
Established in 2021, Shanghai COPAK Industry Co., Ltd. maintains a sales office in Shanghai and an associated factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio includes PET cups, PET cans, and sealing machines, among other related items.
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs. As a long-term strategic partner and trusted supplier, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET cups and cans for our clients.
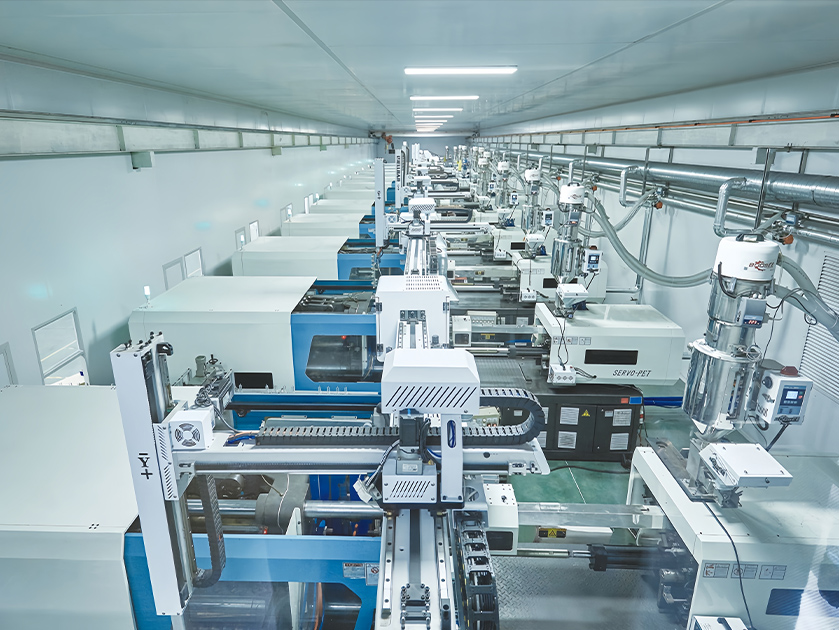
Our optimized facility and advanced equipment are governed by stringent quality control, ensuring efficient, high-standard production.
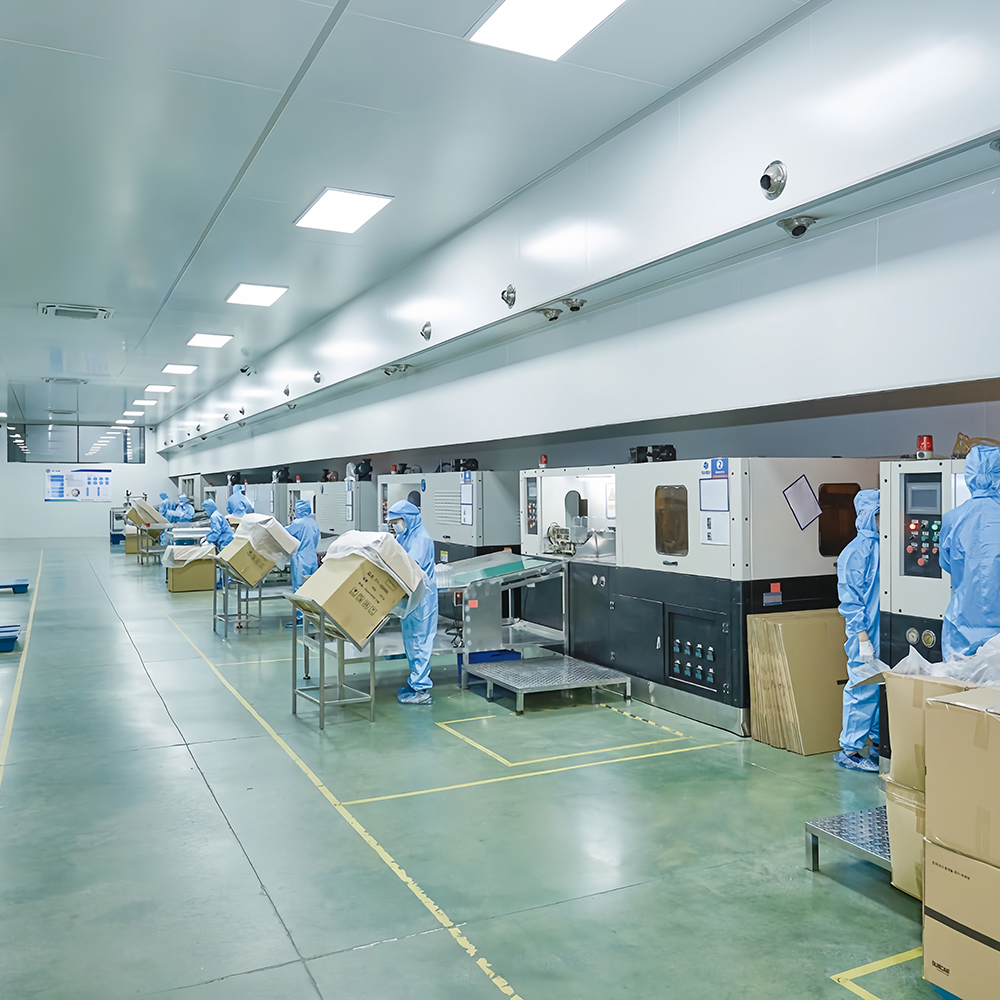
Our factory is situated in a well-connected industrial zone, enabling efficient distribution via convenient transportation networks. The spacious and well-organized facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
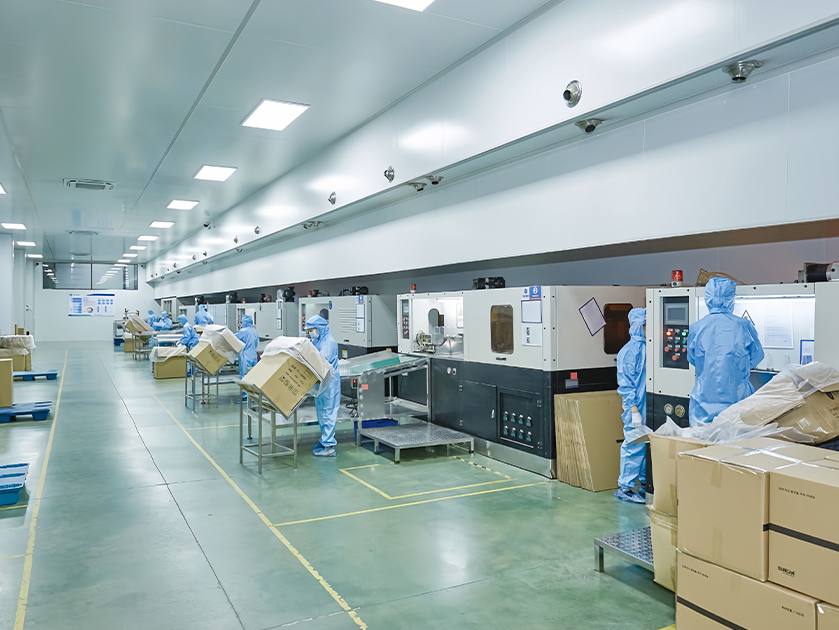
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision or quality. Additionally, our factory houses injection molding machines for preform production, as well as advanced printing equipment to support custom branding needs.
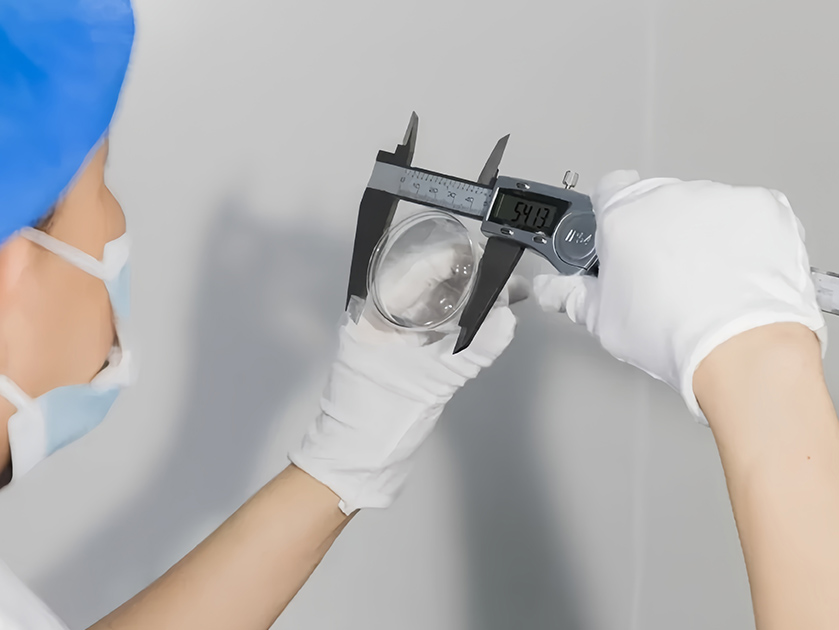
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cups and PET cans adhere to stringent quality standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
We offer extensive customization options to meet the unique requirements of beverage brands and clients, including tailored shapes, sizes, and capacities for PET cups and cans. Additionally, we provide full support for custom mold development and personalized printing solutions.
Adhering to global food-grade packaging regulations and standards, our factory holds various authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These certifications underscore our unwavering commitment to producing safe, high-quality beverage packaging products.
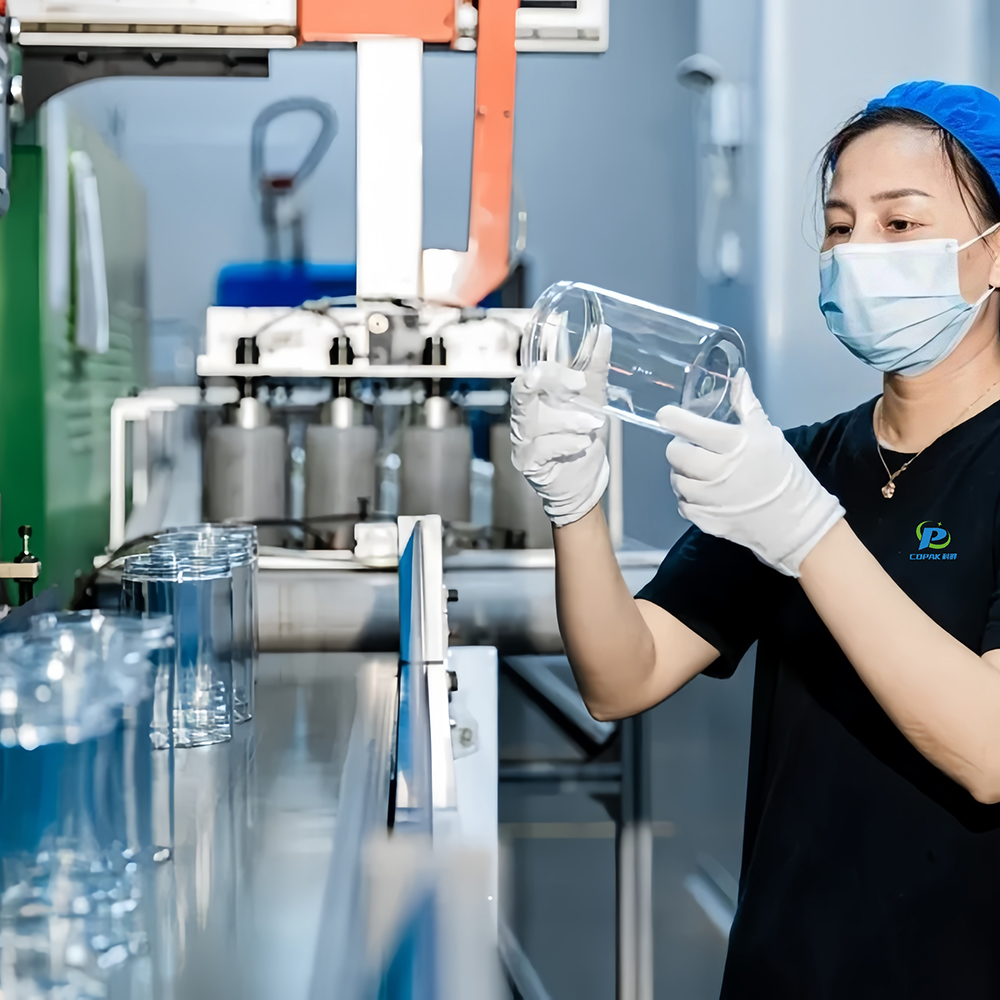
Our dedicated R&D team focuses continuously on product innovation and technological advancement. With professional expertise, the team specializes in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials and technologies to drive industry progress.
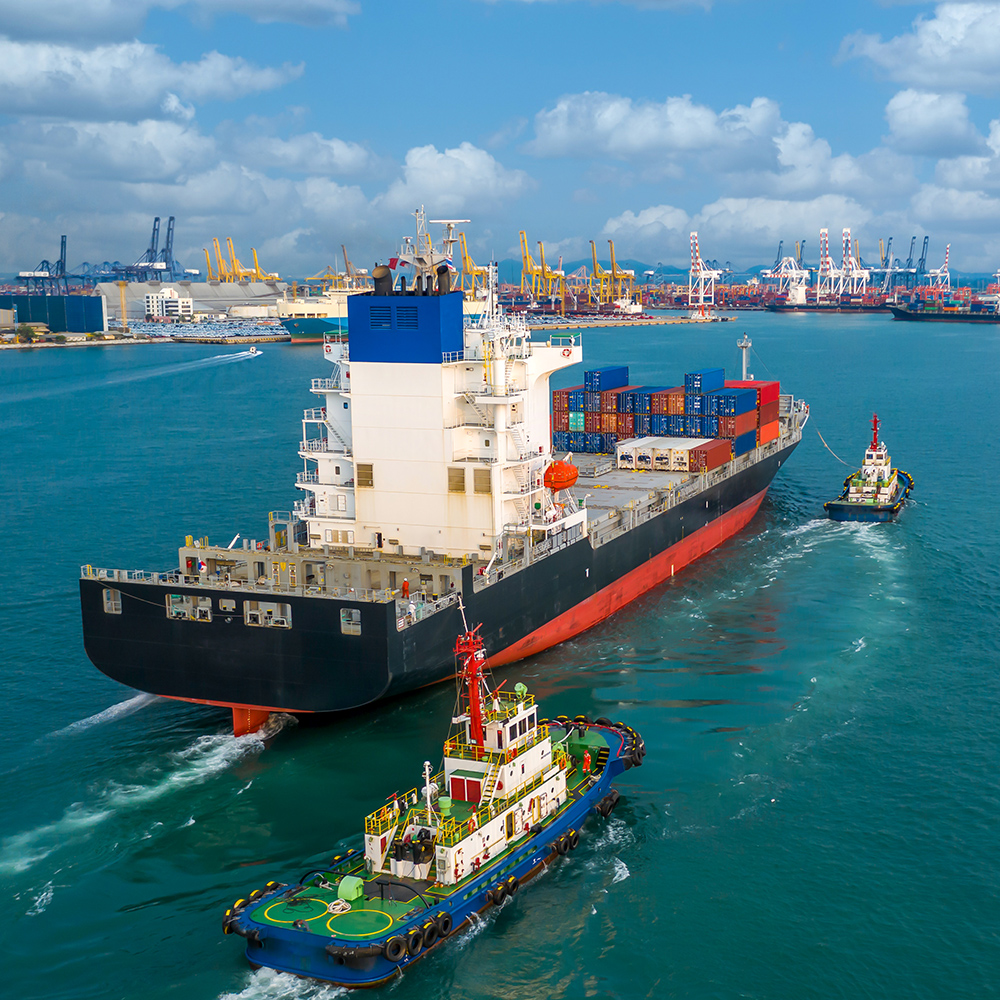
We have established a streamlined logistics system to ensure efficient product distribution. This encompasses well-managed warehousing, precise inventory control, and close coordination with trusted transportation partners, guaranteeing timely and reliable delivery to clients worldwide.
Partnering with us guarantees access to high-efficiency manufacturing, premium food-grade materials, and unmatched client support.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop

Free samples available upon request

Free replacements for products with critical defects
One of the primary concerns for raw, organic kombucha brewers is preserving the delicate balance of live bacteria and yeast (SCOBY). Exposure to high temperatures, oxygen, and ultraviolet light can degrade the quality of the beverage, alter its taste profile, and lead to over-carbonation.
Through extensive R&D, COPAK has developed an optimized polymer matrix for our 500ml PET beverage cans. Our cans feature advanced gas-barrier properties that limit carbon dioxide loss and restrict oxygen transmission rates (OTR). This ensures that the kombucha remains naturally carbonated and free from premature oxidation, maintaining its signature tangy flavor profile from the factory floor to the consumer's hands.
Additionally, for brands utilizing UV-sensitive ingredients, we offer customizable UV-blocking agents integrated directly into the PET material, preventing light-induced oxidation while maintaining the glass-like clarity of the package.
Having supplied PET cup and PET cans to numerous renowned brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation.
INQUIRY NOWFrom micro-breweries to industrial-scale beverage plants, we provide the perfect food-grade PET cans, cups, and custom packaging solutions.