Leave Your Message
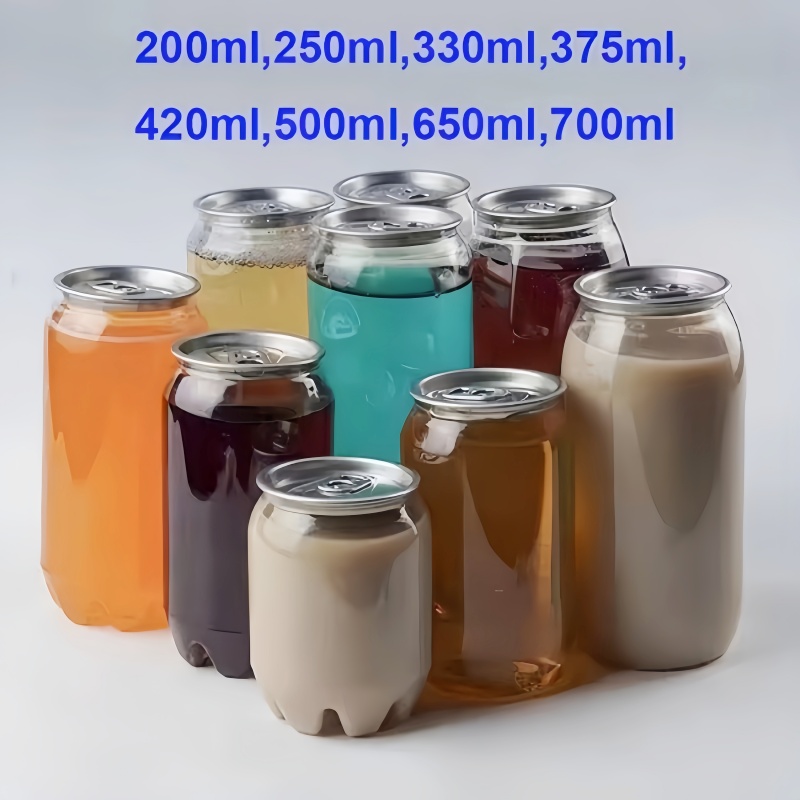
The global artisanal cold brew coffee market is experiencing an unprecedented surge, transforming from a niche cafe offering into a mainstream retail powerhouse. As coffee connoisseurs increasingly demand premium, ready-to-drink (RTD) experiences, the packaging protecting these delicate brews has never been more critical. Enter the 500ml PET Beverage Can—a revolutionary packaging format that seamlessly bridges the gap between aesthetic luxury, functional durability, and economic viability. This comprehensive analysis explores why the 500ml PET can is becoming the gold standard for artisanal cold brew coffee brands worldwide.
From an industrial perspective, the 500ml capacity hits the ultimate "sweet spot." It is large enough to serve as a multi-serve concentrate for home dilution, yet perfectly sized for a premium, single-serve "grande" experience for high-caffeine consumers. Logistically, PET cans are significantly lighter than glass. This drastic reduction in shipping weight translates to lower carbon emissions and drastically reduced freight costs. Furthermore, in the booming e-commerce sector for direct-to-consumer (DTC) coffee subscriptions, the shatterproof nature of PET virtually eliminates the costly issue of breakages during transit, ensuring a flawless unboxing experience for the end consumer.
The manufacturing of PET cans for artisanal beverages is no longer a traditional, mechanical process; it has entered the era of smart manufacturing. The integration of Artificial Intelligence (AI) and advanced robotics into the production line ensures that every 500ml PET beverage can meets the exacting standards required for specialty coffee.
Modern production facilities utilize AI-powered machine vision systems to inspect every single PET can in real-time. These advanced algorithms detect microscopic imperfections in wall thickness, structural integrity, and clarity that human eyes might miss. This ensures that when the can is pressurized—especially critical for Nitro Cold Brew applications—it performs flawlessly, preventing leaks and maintaining the perfect seal.
Artisanal cold brew is highly sensitive to oxygen and UV light, which can degrade its complex flavor notes. The latest trend in 500ml PET cans involves multi-layering technology and advanced oxygen scavengers integrated directly into the polymer matrix. Some premium variants also feature transparent UV-blocking coatings, extending the shelf life of the cold brew while maintaining the highly desired clear aesthetic.
As consumer environmental awareness peaks, the transition towards 100% recycled PET (rPET) is a defining industry trend. Advanced sorting and purification technologies now allow rPET to achieve the same optical clarity and structural strength as virgin PET. This creates a closed-loop lifecycle, drastically reducing the carbon footprint of cold brew packaging and aligning with the eco-conscious values of specialty coffee drinkers.
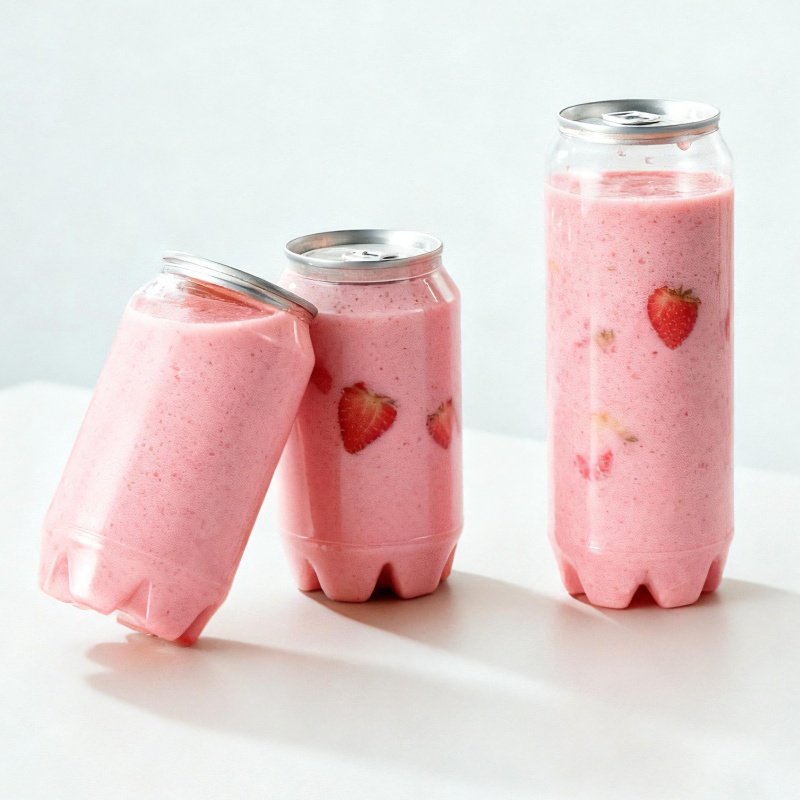
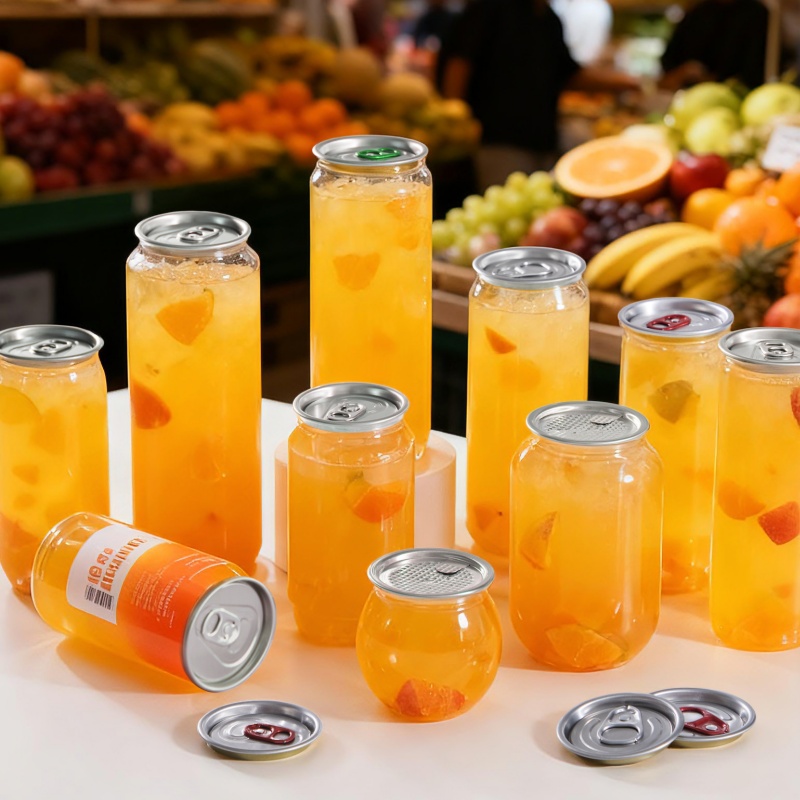
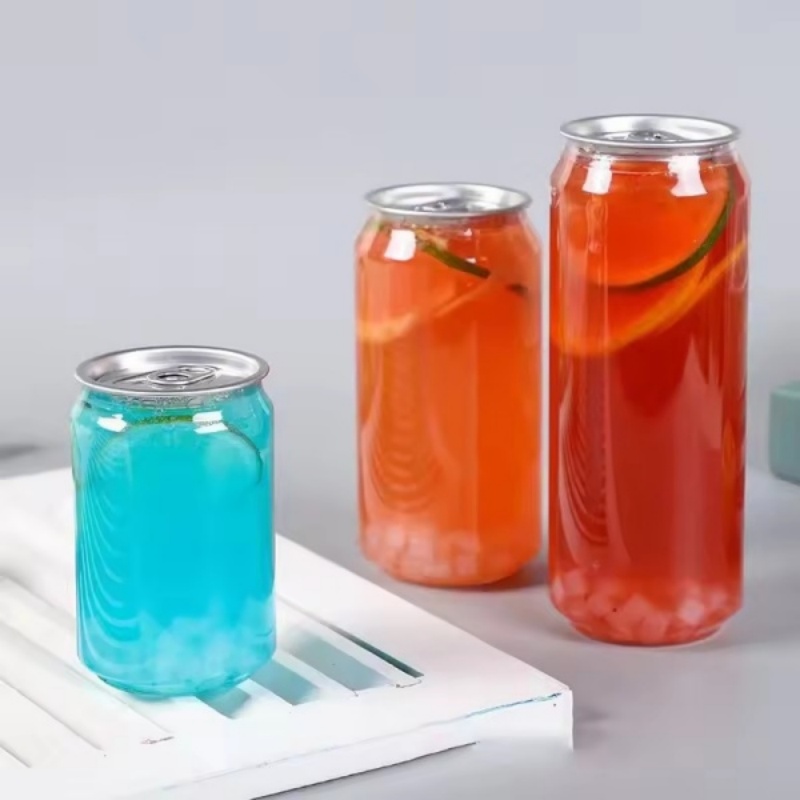
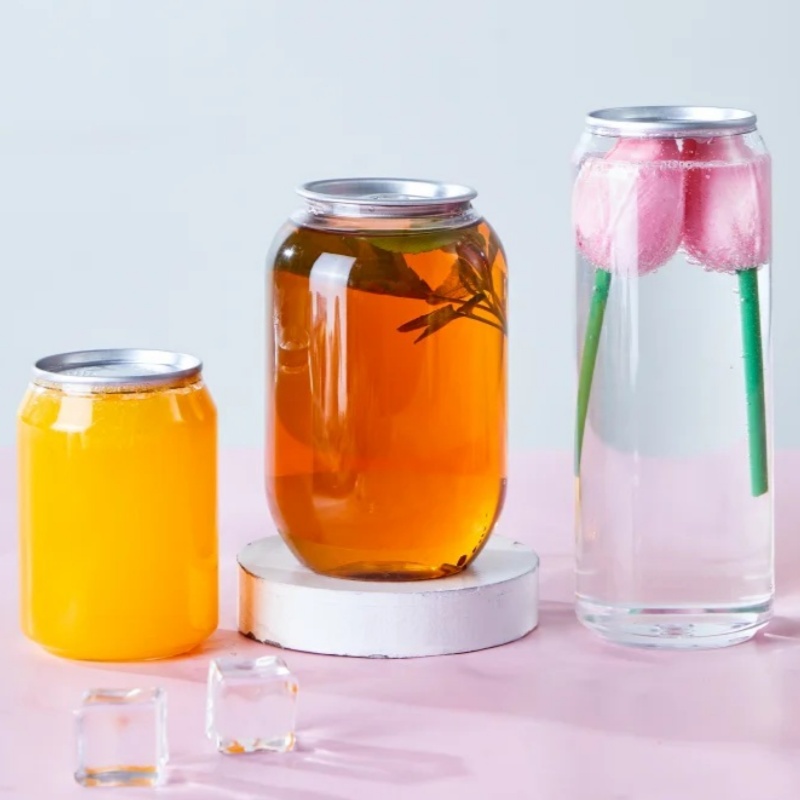
The versatility of the 500ml PET can opens up diverse revenue streams and application scenarios for coffee roasters and beverage entrepreneurs. Its unique combination of an aluminum pop-top lid and a clear plastic body creates a premium tactile and visual experience that adapts to various market demands.
Established in 2021, SHANGHAI COPAK INDUSTRY CO., LTD. maintains a sales office in Shanghai and an associated high-tech factory in Guangdong Province. As a professional supplier of eco-friendly food and beverage packaging solutions, our product portfolio is heavily tailored towards the booming coffee industry, including specialized PET cups, 500ml PET cans for artisanal cold brew, and advanced sealing machines.
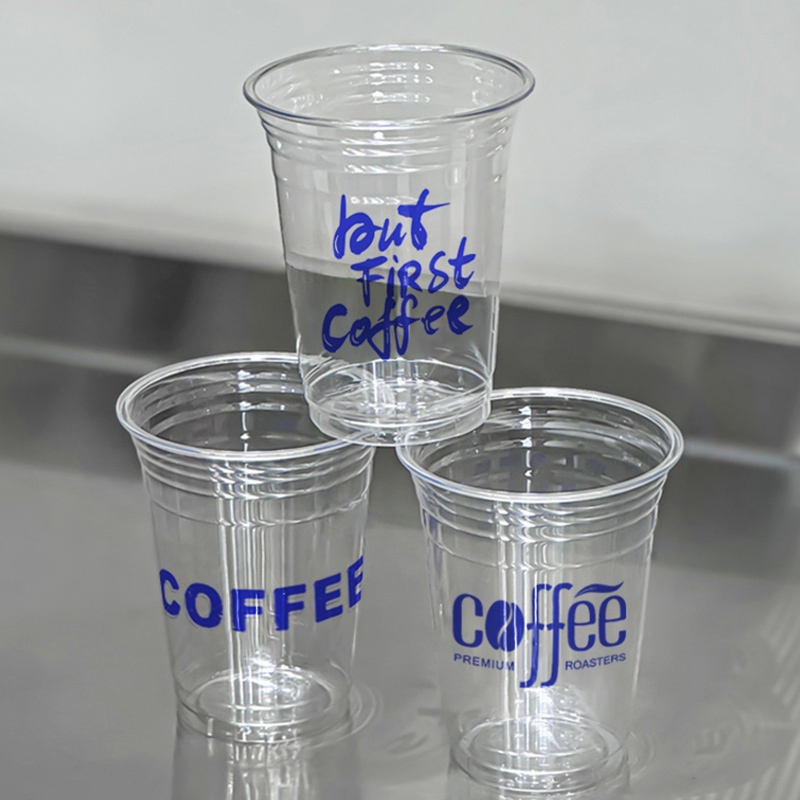
Committed to staying ahead of market trends through continuous innovation, COPAK delivers high-quality yet cost-effective packaging solutions. Our product range covers PET cups and cans in diverse shapes and capacities—from 1oz to 32oz—available in both plain finishes and custom printed designs tailored for artisanal coffee brands. As a long-term strategic partner, we dedicate ourselves to designing and manufacturing reliable, premium-quality, and stylish PET packaging for our global clients.
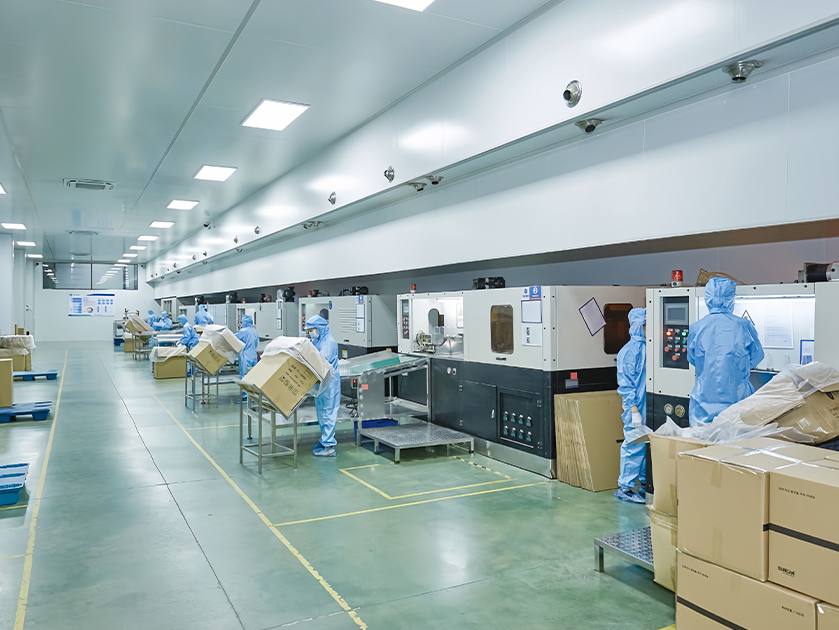
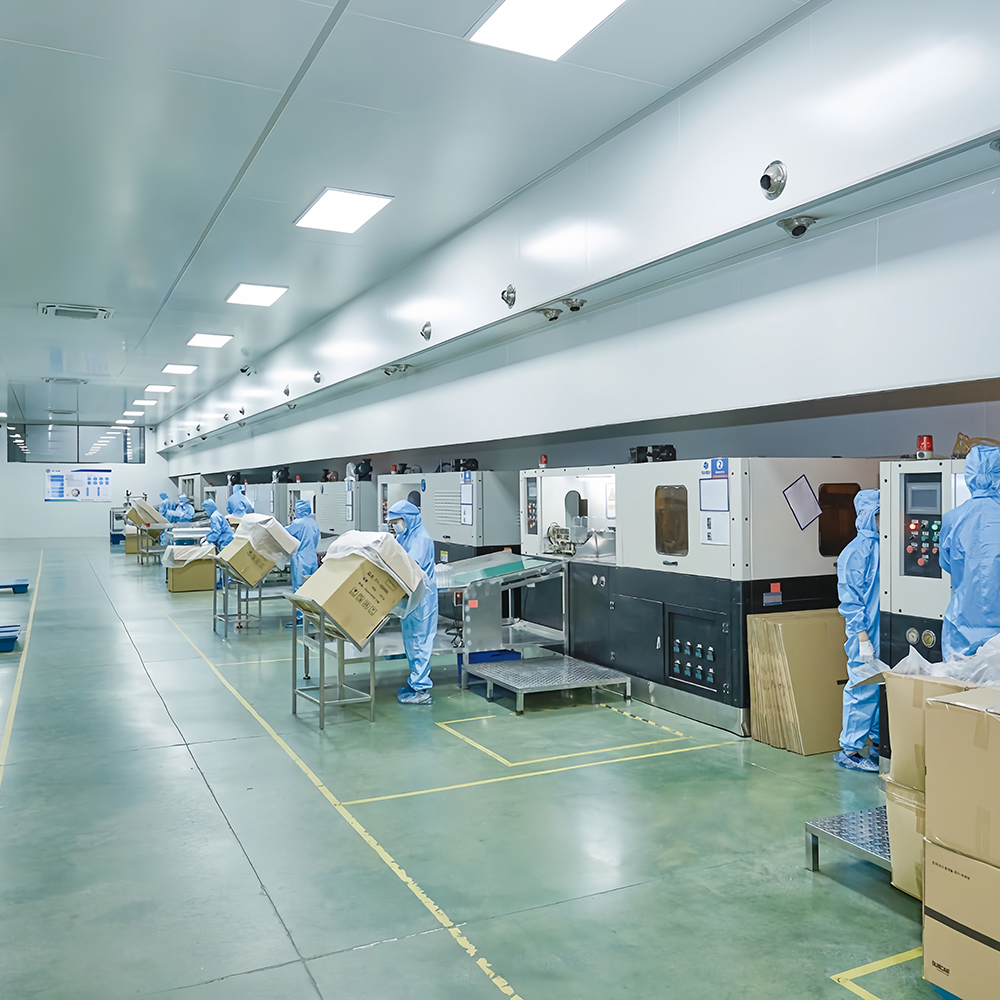
Our optimized facility and advanced equipment are governed by stringent AI-assisted quality control, ensuring efficient, high-standard production for sensitive beverages like cold brew coffee.
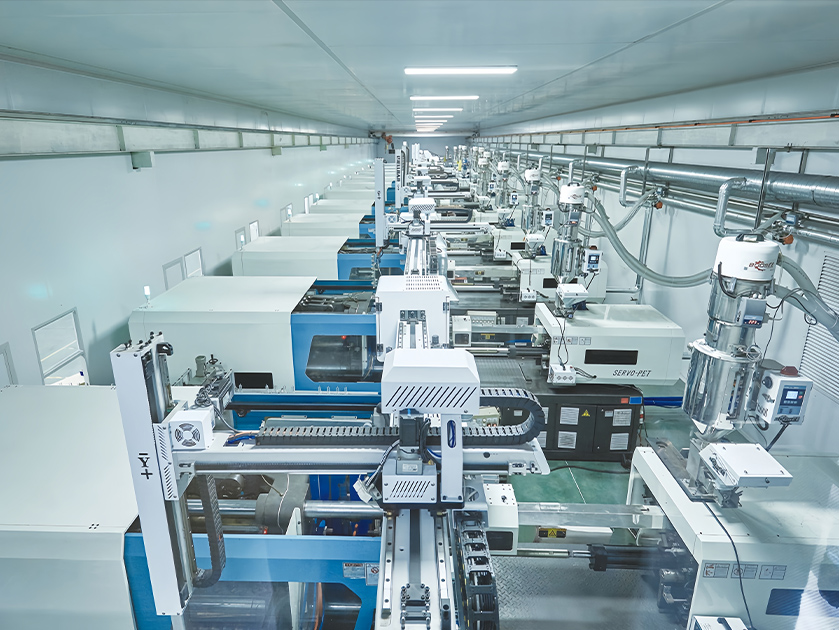
Our factory is situated in a well-connected industrial zone, enabling efficient distribution. The spacious facility features dedicated areas for raw material storage, production lines, quality control, packaging, and logistics operations.
We are equipped with state-of-the-art blow molding machines specifically engineered for PET cup and PET can production, enabling high-speed manufacturing without compromising precision. We also house advanced printing equipment to support custom branding needs.
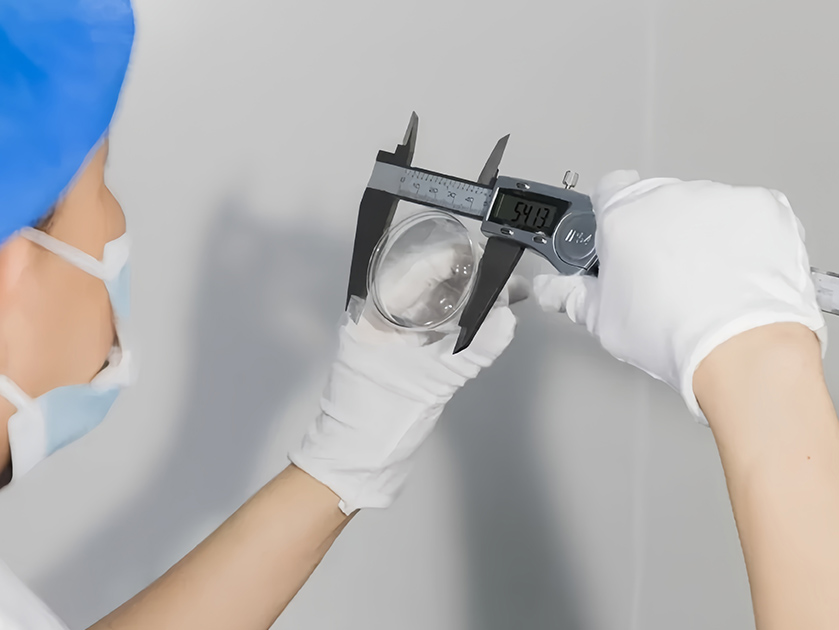
Our dedicated quality control department is equipped with specialized testing equipment to ensure all PET cans adhere to stringent standards. Key inspection items include wall thickness uniformity, dimensional accuracy, visual defect screening, and material integrity verification.
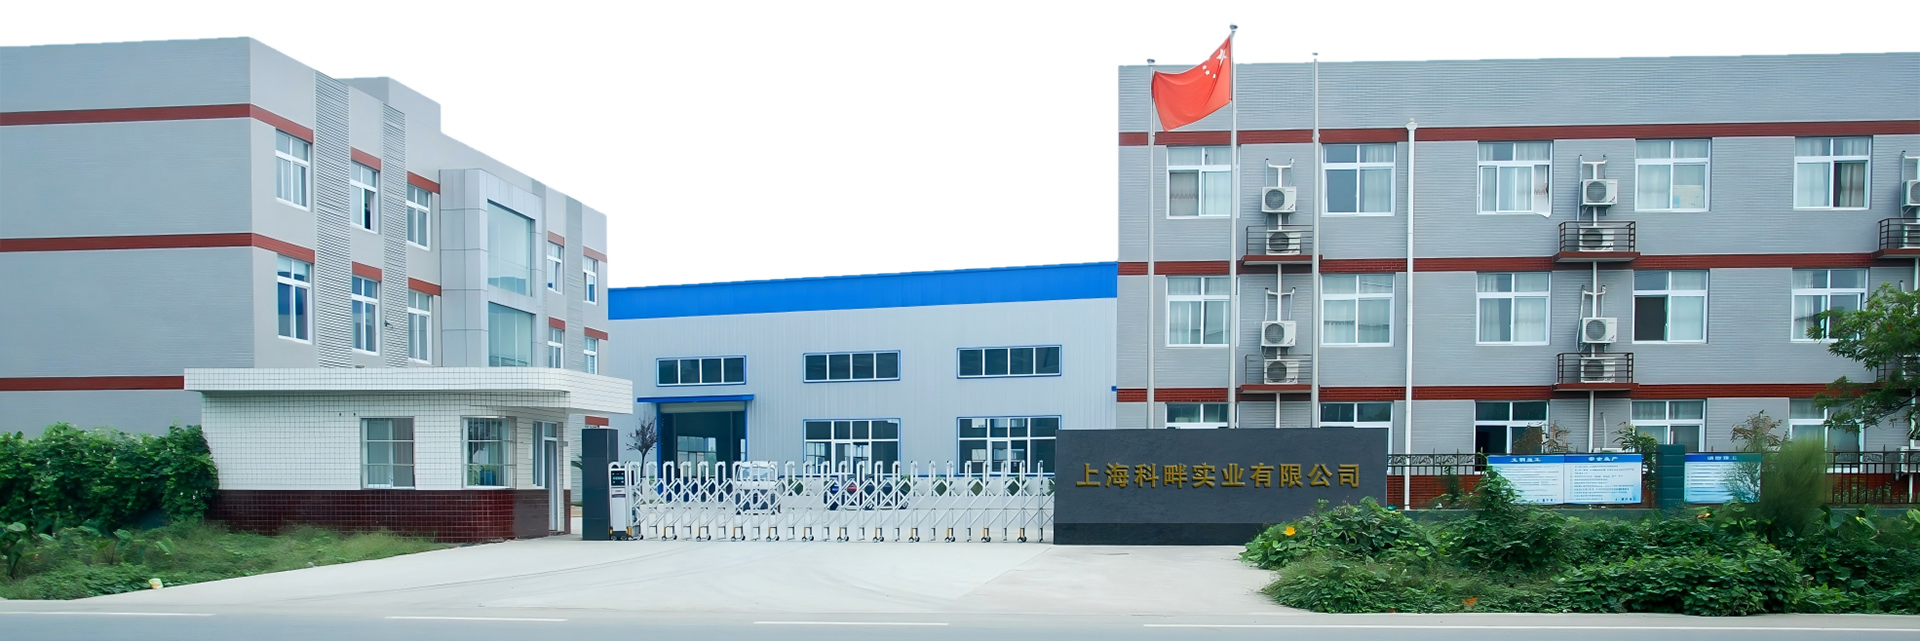
COPAK is deeply committed to sustainable development and has implemented targeted initiatives to minimize energy consumption, reduce waste generation, and promote material recycling. These include the adoption of energy-efficient production processes, robust waste management systems, and the integration of recycled PET (rPET) materials into our cold brew can manufacturing, ensuring your artisanal coffee aligns with eco-friendly consumer values.
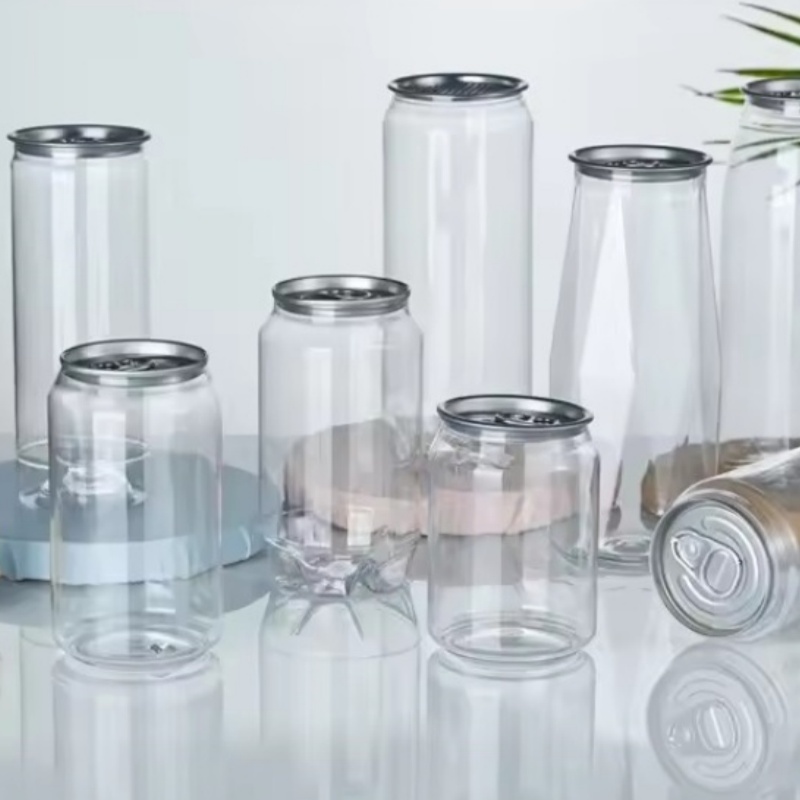
We offer extensive customization options to meet the unique requirements of artisanal cold brew brands, including tailored shapes, sizes, and capacities for PET cans. Additionally, we provide full support for custom mold development and personalized printing solutions to make your product stand out.
Adhering to global food-grade packaging regulations, our factory holds authoritative certifications, including ISO 9001, FDA, CE, ROHS, and EU No. 10/2011. These underscore our commitment to producing safe, high-quality beverage packaging.
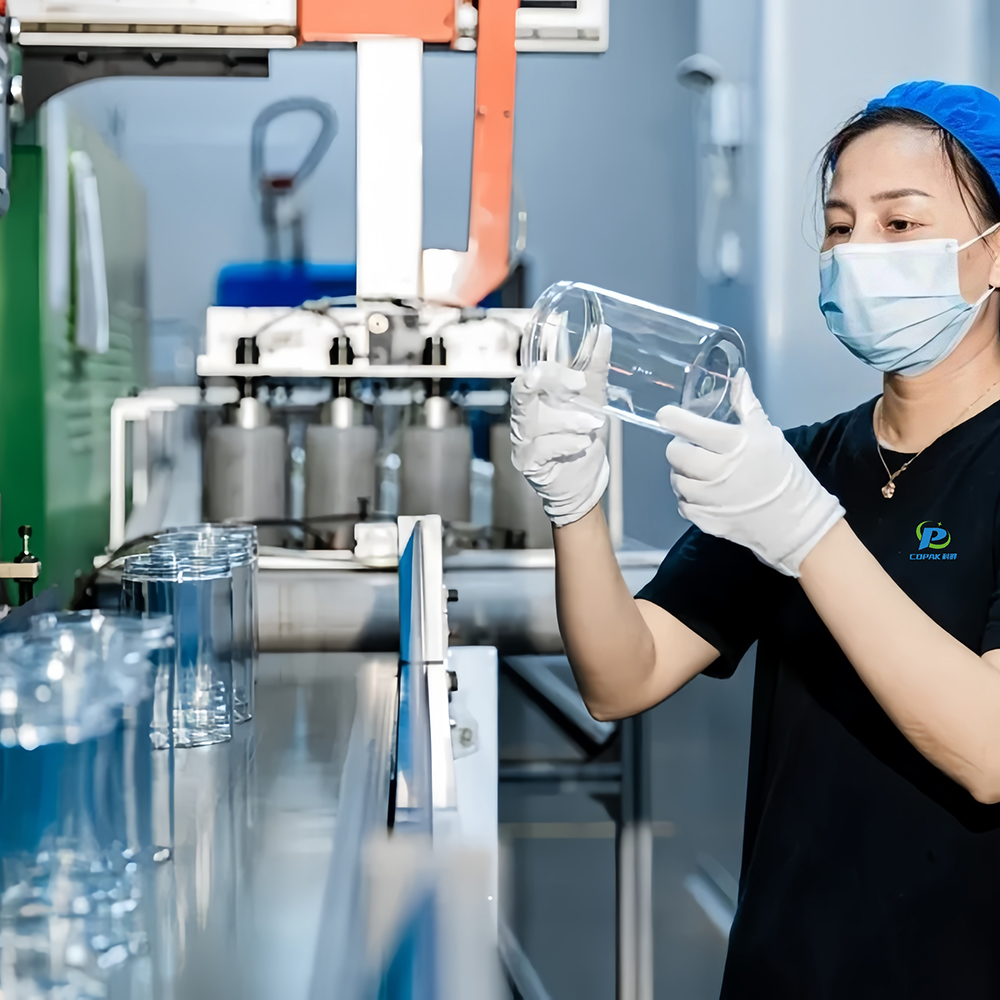
Our dedicated R&D team focuses continuously on product innovation. We specialize in developing innovative packaging solutions, optimizing production processes, and exploring sustainable materials to drive the RTD coffee industry forward.
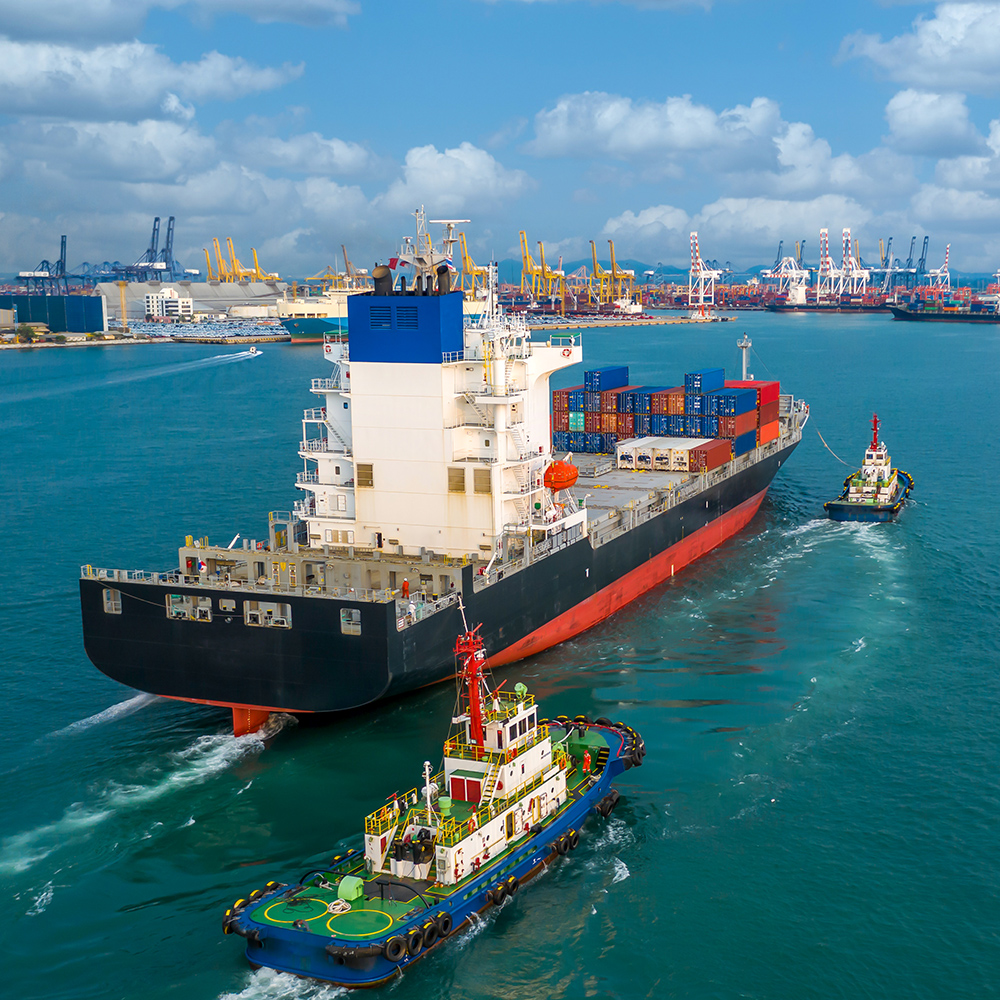
We have established a streamlined logistics system to ensure efficient product distribution globally. This encompasses precise inventory control and close coordination with trusted transportation partners for timely delivery.

Over 20 production lines for rapid order fulfillment

Fully automated, hands-free production equipment

100,000-class cleanroom workshop for food safety

Free samples available upon request

Free replacements for products with critical defects
Having supplied premium PET cans to numerous renowned artisanal coffee brands, our products are now distributed globally. Partner with COPAK for a dependable, trustworthy collaboration and achieve mutual success through win-win cooperation in the booming RTD beverage market.
INQUIRY NOW